
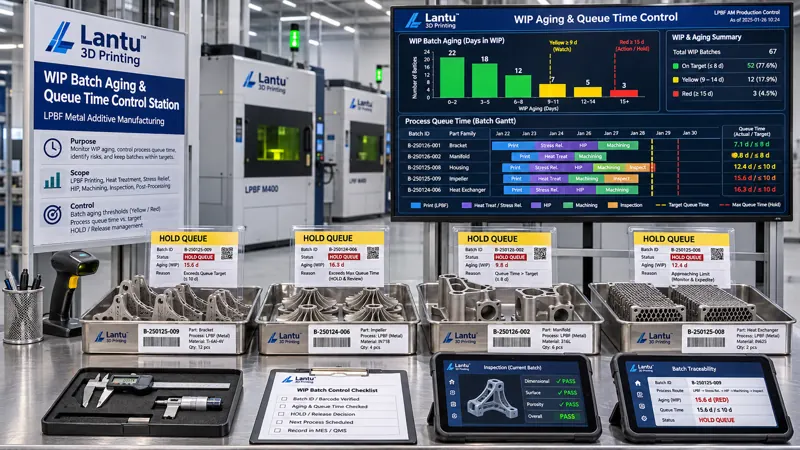
Introduction: The Schedule Is Not Wrong, Yet WIP Keeps Accumulating
Many 3D printing shops reach the same conclusion during post-project reviews: equipment did not stop, work orders were not omitted from scheduling, and powder was available, yet an order still required five to nine additional days from build removal to final delivery. The scheduling Gantt chart shows every operation assigned to a time window; on the shop floor, however, parts remain at depowdering stations, in front of heat-treatment furnaces, or in CMM inspection queues. The issue is not whether work was scheduled, but how long a WIP batch actually waited after being scheduled and who determined whether it could continue to flow. lantu3D classifies this issue as part of lifecycle management from blueprint design to physical delivery: the planning layer defines the production sequence, while the execution layer must provide status metrics for WIP batches; otherwise, delivery commitments cannot be independently verified.
1. Why WIP Aging Must Be Defined Separately
WIP age is not the number of days since an order entered production, nor is it equivalent to machine occupancy time. For metal LPBF parts, a build can be separated into multiple part numbers after removal from the machine, with each then proceeding through depowdering, support removal, heat treatment, wire EDM, blasting, inspection, and packaging. Different parts within the same batch may be held at different operations. It is recommended to use “part number + batch number + operation number” as the minimum status unit and record four timestamps: T_release (work-order release), T_start (actual operation start), T_finish (operation completion), and T_accept (downstream acceptance). Operation age is A_op = current time − T_finish; batch age is A_batch = current time − T_release; and queue time is Q = T_start − T_finish (upstream operation). Only by tracking these three metrics separately can a shop avoid mistaking “the machine printed for 18 hours” for “the part spent only a short time waiting.”
2. Establishing an Auditable Workstation Status Dictionary
The status dictionary should include at least: batch primary key, part number or tray number, current workstation, previous-operation completion code, next operation, kit-completeness status code, quality status code, aging interval, responsible person, and exception record number. Only four statuses should be permitted: RUN (in process), QUEUE (qualified and waiting), HOLD (controlled suspension), and BLOCK (blocked pending disposition). QUEUE and HOLD must be strictly distinguished: the former may automatically enter a downstream reservation slot, while the latter must include a reason code, approver, estimated release time, and reinspection requirement. Common reason codes include pending powder requalification, unavailable witness-coupon results, customer ECN impact analysis, inspection-resource failure, and borrowed tooling not returned. When status codes are entered at production-reporting terminals, the operator and terminal ID must be retained. Free-text entries such as “temporary hold” or “awaiting notice” must not be used as substitutes.
3. Aging Thresholds and Overdue Escalation Rules
Thresholds should be frozen by process family rather than applying a plant-wide 48-hour standard. They can be established using the measured P50 and P90 queue times of conforming batches from the previous three months: the QUEUE warning limit W = P90 × 1.2, and the HOLD limit H = 24 hours. Holds requiring third-party testing or customer approval may be extended to 72 hours, but the external reference number must be recorded. For example, if P90 for support removal is 9 hours, W is approximately 11 hours; if P90 for pre-heat-treatment queuing is 16 hours, W is approximately 19 hours; and if P90 for CMM inspection queuing is 22 hours, W is approximately 26 hours. When aging exceeds W, the batch enters the yellow list and the production team must confirm its disposition during the same shift. When it exceeds 1.5W, or when HOLD exceeds H, it enters the red list; planning, quality, and process engineering must jointly approve one of four outcomes: continue processing, outsource, isolate for reinspection, or scrap. Threshold versions should be reviewed quarterly as equipment capacity, product families, and inspection resources change. Old versions must not be overwritten; their effective dates and applicable order scope must be retained.
4. Process Dwell Attribution Cannot Be Reduced to “Bottlenecks”
Shop-floor accumulation is often broadly attributed to insufficient capacity, leading directly to further equipment purchases. A more auditable approach is to divide each Q interval into six categories: upstream/downstream takt mismatch, batch preparation and changeover, unavailable material or tooling, unsigned quality evidence, waiting for customer changes, and resource failure. Each occupancy category should be linked to an event code and supporting evidence: material shortages to kit-completeness checklists, unsigned evidence to inspection-lot or report numbers, customer changes to ECN numbers, and failures to equipment alarm codes. During monthly reviews, calculate the share of total queue time represented by each category, and separately track pure administrative waiting in cases where conforming evidence exists but the batch has not moved forward. If pure administrative waiting exceeds 20%, improve the status dictionary and handoff acknowledgments before adding machines.
5. Closed-Loop WIP Inventory and Hold Release
A physical-to-system reconciliation should be performed once per day at shift handover, but every physical item does not need to be moved to an inventory area. Use tray-number or DPM scanning to verify five items against the WIP list: workstation, status, aging interval, and exception record number, with sample checks of physical identification and quantity per tray. Discrepancies are classified into four types: location error, status error, quantity error, and missing identification. Any discrepancy requires a deviation record during the same shift; statuses must not be edited directly. A HOLD may be released only by the originally authorized role, which must enter the reinspection result, release time, first operation after release, and downstream recipient. If the process parameter package was revised, the powder lot changed, or a customer ECN became effective during the HOLD period, the impact analysis must be rerun before release; the pre-hold release decision may not be reused. Release records and original hold records must be retained as paired records, forming a time chain that can be audited by customers.
6. Release Gates and Delivery Evidence
Set five D1 through D5 release gates before a WIP batch enters packaging and shipment. D1 verifies that all part numbers have left RUN/QUEUE and that no exception records remain open. D2 verifies that A_batch does not exceed the total aging limit frozen for the applicable product family; any exceedance requires a three-party approval conclusion. D3 verifies one-to-one correspondence in the quality evidence chain among powder lot, build number, heat-treatment furnace run, witness coupon, and final inspection report. D4 verifies that HOLD release records are complete and that the ECN impact-analysis version is current. D5 requires the delivery owner to sign the shipment-status checklist, which includes the batch primary key, total queue time, total hold duration, overdue-disposition conclusion, and threshold version number. The checklist should accompany the shipment or be retained as stipulated by contract, allowing the question “Why did this batch wait three additional days?” to be answered by records rather than recollection.
7. Implementation Sequence and Common Misconceptions
A four-week implementation is recommended. In week one, establish only the status dictionary and four timestamps, without performance assessment. In week two, replay two weeks of historical production-reporting data to calibrate P90 and the W and H thresholds for each operation. In week three, launch yellow and red lists and shift-handover scan verification, migrating free-text exceptions into reason codes. In week four, make D1–D5 mandatory pre-shipment blocks and conduct a drill tracing the time chain backward from a serial number. Three misconceptions should be avoided. First, do not derive a single WIP limit from order due dates while ignoring process-family differences. Second, do not treat HOLD as an ordinary extension of QUEUE, allowing risks such as pending customer approval or incomplete inspection to be absorbed automatically by scheduling. Third, do not record only “where it is now” without recording “when the previous operation finished” and “when downstream accepted it”; otherwise, Q and A_op can never be calculated. Recommended metrics are: percentage of QUEUE items exceeding W, percentage of HOLD items exceeding H, share of pure administrative waiting, and first-pass rate for D gates before shipment. Targets should be ≤5%, ≤2%, ≤20%, and ≥95%, respectively.
Conclusion
Delivery stability in low-volume 3D printing depends not only on whether schedules can fully load equipment, but also on whether the interval from operation completion to downstream acceptance is measured, classified, and closed for each WIP batch. By using part number + batch number + operation number as the status unit, calculating batch age, operation age, and queue time with four timestamps, distinguishing waiting from controlled suspension through a four-state dictionary, and closing the evidence chain through threshold escalation, reason-code attribution, hold release, and D1–D5 gates, a shop can transform “WIP keeps piling up” into engineering status metrics that are determinable, reviewable, and available for customer verification. This is an indispensable management interface between the planning layer and the execution layer when moving from design blueprints to physical delivery.
Submit a model, drawing, image or written notes. Engineers will review material, process, finishing and delivery based on actual use.