
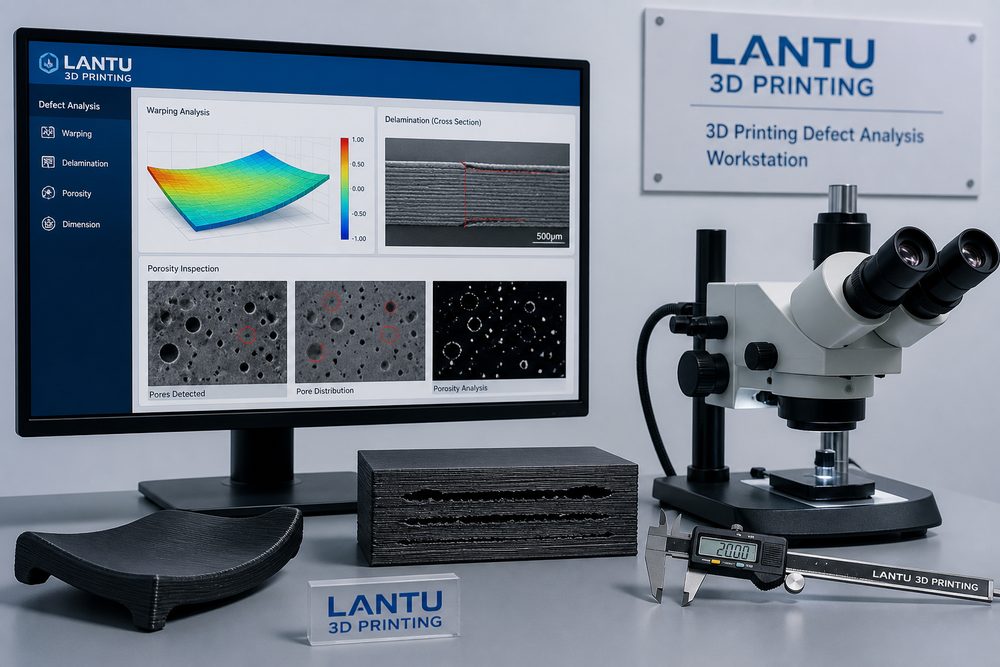
Introduction: Defects Are Not Random, They Are System Signals
When a 3D printing project experiences warping, delamination, porosity, surface stringing, or dimensional drift, the most common mistake is to simply print again and hope the problem goes away. In real engineering practice, defects are often the combined result of model structure, material condition, machine maintenance, process window, environmental control, and post-processing. Without a standardized troubleshooting workflow, the second print may fail as well, and the problem may even be incorrectly attributed to the material or the machine itself. In project retrospectives, lantu3D usually treats defects as system signals, using data logging and layered verification to identify the root cause.
1. First Confirm Which Stage the Defect Occurred In
The first troubleshooting step is to determine at which stage the defect appeared. In the slicing preview stage, you can detect thin walls, overhangs, isolated islands, insufficient supports, and infill anomalies. Warping that appears early in the print is usually related to bed adhesion, first-layer temperature, powder bed preheating, or resin exposure. Delamination in the middle stage is often associated with thermal stress, material moisture content, laser energy density, or unstable extrusion. If cracking, discoloration, or dimensional changes only appear after post-processing, the cause may be curing, heat treatment, cleaning solvents, or drying after coating. Recording the time point can reduce the troubleshooting scope by more than half.
2. The Root-Cause Chain for Warping
Warping is essentially caused by shrinkage stress exceeding the local restraint capability. In FDM, materials such as ABS and PC shrink significantly as they cool. If the chamber temperature is too low, the first layer is too loose, or the part has a large flat area on the build plate, the corners are likely to lift. In SLS, if the powder bed temperature is below the material’s crystallization window or cooling is too rapid, the edges of thin flat parts can curl upward. SLA parts may deform due to uneven wall thickness, curing shrinkage, and an unreasonable support layout. Engineering recommendations include splitting large flat surfaces or adding ribs, increasing first-layer adhesion area by 10% to 20%, keeping thin-wall thickness uniform, avoiding large-area unilateral supports on resin parts, and using slow cooling with optimized part orientation for SLS builds.
3. Diagnosing Delamination and Insufficient Strength
Delamination usually occurs along directions where interlayer bonding is weak. For FDM, check nozzle temperature, cooling fan speed, material moisture content, and layer height. If PLA is printed at a 0.2 mm layer height with too low a temperature, interlayer diffusion will be insufficient. Nylon that has absorbed moisture can create bubbles and microvoids, reducing strength. For SLA, check exposure energy, resin settling, and peel forces. For SLS, interlayer strength depends on powder refresh rate, laser power, and scan speed. During diagnosis, it is recommended to test samples from the same batch using three-point bending or tensile tests, and to archive photos of the fracture surfaces. If the fracture surface appears powdery or the layer lines are obvious, the interlayer bond is insufficient. If the fracture passes through the solid material, the material itself or the structural design may be the primary cause.
4. Porosity, Under-Sintering, and Surface Defects
Porosity in metal SLM is often related to powder particle size distribution, oxygen content, powder spreading quality, laser power, and scanning strategy. Too low an energy density can create lack-of-fusion pores, while too high an energy density may produce keyhole porosity. Pinholes on resin parts may come from bubbles, incomplete cleaning, or volatile release during curing. Rough SLS nylon surfaces are usually related to powder particle characteristics, temperature distribution, and sandblasting intensity. For porosity-related defects, visual inspection is far from enough; critical parts should be evaluated by CT scanning, metallography, or density testing. For appearance parts, it is recommended to apply primer surfacing and localized filler before painting, so that printing defects are not amplified in the final surface.
5. Build a Reusable Defect Troubleshooting Sheet
Each defect review should record at least six categories of data: model version, slicing parameters, material batch, equipment status, ambient temperature and humidity, and post-processing parameters. Model records should include wall thickness, overhang angle, minimum hole diameter, and support contact positions. Material records should include opening time, drying conditions, and batch number. Equipment records should include nozzle, scraper, laser window, or resin vat condition. Environmental records should include temperature, humidity, and ventilation. With tabulated records, the team can identify repeated patterns, such as a certain thin-plate part warping more severely in the same orientation, or a specific material batch showing increased delamination when humidity exceeds 60%.
Conclusion
The value of 3D printing defect analysis is not just to solve one failure, but to turn failure into process knowledge. By combining stage identification, root-cause chains, inspection methods, and a recording system, companies can reduce repeated trial and error and improve delivery stability. lantu3D recommends integrating defect analysis into the project lifecycle so that every abnormal event becomes evidence for the next successful delivery.
Submit a model, drawing, image or written notes. Engineers will review material, process, finishing and delivery based on actual use.