
Introduction: Why Directly Printing a Traditional Design Often Costs More and Carries Higher Risk
Many 3D printing failures are not caused by insufficient machine capability, but by design logic that still follows traditional machining or injection molding thinking. Machining favors regular shapes, tool access, and material removal efficiency; injection molding focuses on draft angles, gates, shrinkage, and mold life; additive manufacturing, by contrast, focuses on layer-by-layer stacking, support generation, thermal deformation, powder removal, interlayer strength, and post-processing accessibility. Sending a drawing that has not undergone DFAM review directly to print often leads to excessive supports, thin-wall deformation, undersized holes, trapped powder in internal cavities, budget overruns, or assembly failure.
The goal of design optimization is not to create flashy geometries, but to achieve a verifiable balance among performance, cost, lead time, and quality. In projects, lantu3D typically places design review at the front end of manufacturing, linking blueprint data, use scenarios, material processes, and delivery standards to avoid situations where customers discover only after printing that the structure is not suitable for real-world use.
1. Wall Thickness and Feature Size: Printable Is the Minimum, Usable Is the Goal
Wall thickness is one of the most basic and yet most overlooked parameters in 3D printing design. Different processes have very different minimum wall-thickness requirements: for SLA resin display parts, local wall thickness can be as low as 0.6-0.8 mm, but if the part must bear assembly or transportation loads, it is better to increase it to 1.2-2.0 mm; for SLS PA12 nylon functional parts, wall thickness is commonly recommended at 1.5-2.5 mm or more; for metal SLM parts, thin-wall structures are affected by thermal stress and post-processing, so direction, supports, and heat treatment must be evaluated together. Isolated posts, slender needles, cantilever beams, and similar features should not be judged only by the minimum buildable size, but also by their resistance to damage during cleaning, sandblasting, packaging, and use.
Designers should distinguish between "minimum printable wall thickness" and "engineering-safe wall thickness." For example, a 0.8 mm thin wall in an appearance sample may print successfully, but it can easily crack during express shipping; a 2 mm wall in a fixture may seem sufficient, but if the load is concentrated at one point, it may still crack when screws are tightened. A more robust approach is to add fillets, ribs, or local thickening in thin-wall areas, and then verify with finite element analysis or empirical load testing.
2. Supports and Orientation: Build Direction Determines Surface Quality, Strength, and Cost
Print orientation affects support volume, layer-line direction, dimensional accuracy, and mechanical performance at the same time. For SLA parts, placing cosmetic faces upward or sideways can reduce support marks, but may increase the visibility of layer lines. For metal SLM parts, large horizontal overhangs increase support requirements and thermal deformation risk, so tilting the part by 20°-45° is usually necessary to spread thermal stress. SLS does not require traditional supports, but orientation still affects interlayer strength and warping risk.
The principle of support optimization is to place supports on non-critical surfaces, reduce deep-channel supports that are difficult to remove, avoid support contact on weak edges, and leave enough room for post-processing tools. If a part has strict appearance requirements, the A-side should be marked in the design file and the orientation confirmed with the manufacturing team. For production parts, the labor time for support removal should also be evaluated, because the risk reduction gained from fewer supports may be offset by increased post-processing cost.
3. Holes, Slots, and Assembly Clearance: Using Compensation to Handle Real Manufacturing Deviations
Undersized holes are common in 3D printing. Causes include overcuring in photopolymerization, powder sintering spread, thermal shrinkage in metal parts, and the stair-step effect of layer building. When designing screw holes, shaft holes, and snap-fit features, compensation should be reserved according to the process. For SLA, small holes may need 0.1-0.2 mm allowance; for SLS, assembly clearance is often 0.2-0.4 mm; for metal parts, critical holes are usually recommended to be printed undersized and finish-machined to final dimensions. For sliding fits, rotational fits, and snap fits, a single clearance value is not reliable, so spline tests should be used to confirm performance.
Deep slots and internal cavities must also be designed with powder removal, cleaning, and coating accessibility in mind. A complex flow channel may be printable, but if there is no powder escape hole or inspection path, delivery can still carry residual-risk issues. During design optimization, auxiliary holes, split structures, or transparent validation samples can be introduced. For multi-part assemblies, it is also wise to print a small tolerance coupon first to verify insertion force, clearance, and dimensional changes after surface finishing before moving to full-scale production.
4. Topology Optimization and Lightweighting: Complex Geometry Must Serve Engineering Goals
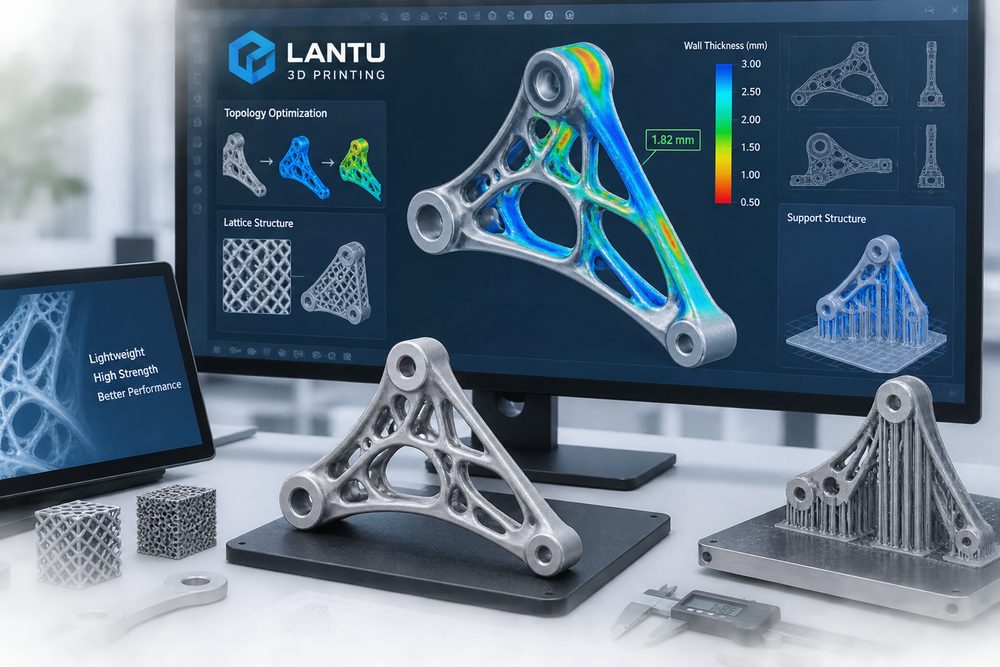
One advantage of additive manufacturing is the ability to realize topology optimization, lattice structures, and internal weight reduction. But lightweighting is not simply hollowing a part out. Topology optimization requires clear inputs for load, constraints, material, manufacturing direction, and safety factor; otherwise, the resulting organic structure may be difficult to depowder, difficult to inspect, or prone to localized stress concentrations. Common engineering goals include reducing weight by 20%-50%, maintaining critical stiffness, lowering material usage, or improving heat exchange efficiency.
Lattice design must account for strut diameter, node geometry, porosity, and powder-removal channels. In SLS nylon lattices, struts should not be too thin; metal lattices must also consider residual unmelted powder and fatigue performance. Load-bearing parts must be validated through simulation, sample compression tests, or fatigue tests rather than relying solely on software-generated results. In such projects, lantu3D reviews topology results together with process feasibility to avoid "beautiful models that are hard to deliver."
5. Building a DFAM Review Checklist: Making Design Optimization Repeatable
Enterprise teams can create a concise DFAM checklist: does the minimum wall thickness meet the intended use, are critical faces marked, has the print orientation been evaluated, can the supports be removed, have holes been compensated, has assembly clearance been verified, are powder or fluid drainage holes sufficient, is post-processing accessible, are critical dimensions measurable, and does the material match the temperature, strength, and chemical-resistance requirements? Each item should be confirmed before manufacturing, not reworked after a failure.
At the same time, design optimization should be linked to transparent cost control. Reducing supports, lowering part height, consolidating parts, arranging them intelligently, and avoiding unnecessary precision can all reduce printing and post-processing costs. On the other hand, blindly pursuing one-piece integration may increase risk. Truly mature additive-manufacturing design places function, manufacturability, inspection, cost, and delivery within the same decision framework.
Conclusion: DFAM Moves 3D Printing from Trial-and-Error to Engineering Delivery
Design optimization for additive manufacturing is a prerequisite for enterprises to achieve stable 3D printing results. Wall thickness, supports, orientation, assembly clearance, topology structure, and post-processing accessibility together determine whether a part can move smoothly from a digital model to a usable physical product. lantu3D is not positioned as a simple printing service provider, but as a partner that helps customers connect blueprinting, design, process, manufacturing, and delivery through a systematic method that reduces trial-and-error, improves quality, and shortens product validation cycles.
Submit a model, drawing, image or written notes. Engineers will review material, process, finishing and delivery based on actual use.