
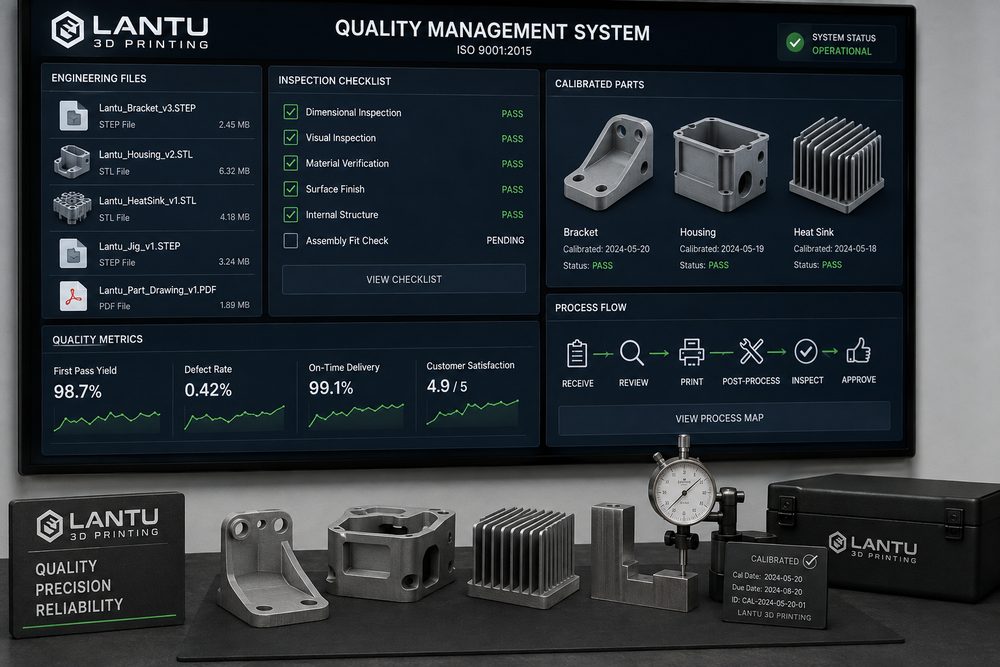
Introduction: At scale, the first thing tested is the standard, not the capability of a single machine
Many companies, when first adopting 3D printing, focus mainly on material cost, print accuracy, and lead time. But when a project grows from one prototype to 30 parts, 100 parts, or monthly replenishment orders, the factors that truly determine delivery stability quickly shift to the standardization system. If the same model file has unclear version control, old and new structures may get mixed up; if the same PA12 nylon material uses different powder refresh ratios, it can lead to differences in color, toughness, and dimensional shrinkage; if the same SLA resin part is post-cured for different lengths of time, surface hardness and assembly feel may vary. When lantu3D handles projects from design blueprints to physical delivery, standardization is treated as part of lifecycle management rather than paperwork at the end of production.
An effective 3D printing standardization system should cover at least five layers: input file standards, design review standards, material and process standards, in-process inspection standards, and delivery acceptance standards. The goal is not to force every project into the same workflow, but to build a reusable decision framework across different materials, batch sizes, and application scenarios so that engineers, procurement teams, customers, and production staff share a consistent understanding of what qualifies as acceptable delivery.
1. Input file standards: clarify version, units, and manufacturing intent first
Manufacturing risk in 3D printing often begins the moment a file enters the system. Common problems include broken STL meshes, confusion between millimeters and inches, multiple files with the same name but different versions, assemblies that lack datum relationships, and wall thickness information that exists only in verbal communication. The first step in standardization is to define file naming rules and required information fields. For example, a structure such as "project code-part number-version-material-date" is recommended, with version numbers incrementing from V01 onward. The frozen version must be confirmed by the customer or project owner. For functional parts that will be reordered over the long term, source files, STL/STEP manufacturing files, quotation screenshots, process review records, and final delivery photos should also be retained.
During file checking, minimum wall thickness, minimum hole diameter, minimum clearance, maximum envelope size, and critical surface markers should be specified. Using SLS PA12 as an example, a general load-bearing shell is usually recommended to have a wall thickness of no less than 1.5-2.0 mm, while slender clips should add fillets and ribs according to the direction of force. For SLA appearance parts that require sanding and painting, the model dimensions should reserve 0.1-0.3 mm of post-processing allowance. Writing these rules into an order acceptance checklist can significantly reduce rework caused by discovering after printing that the part cannot be assembled.
2. Design review standards: move risk forward with DFAM
Design review for additive manufacturing should not merely determine whether the model can be sliced; it should determine whether it can be manufactured reliably with the target process. DFAM review can be divided into four categories: printability, assemblability, surface requirements, and cost sensitivity. Printability focuses on overhang angles, enclosed cavities, thin walls, slender posts, sharp corners, and warping risk on large flat surfaces. Assemblability focuses on hole-to-shaft fits, threaded inserts, clip fatigue, and locating datums. Surface requirements focus on visible surfaces, support contact areas, and finishing grade. Cost sensitivity focuses on build orientation, support volume, powder utilization, and machine time per part.
For example, in a drone enclosure project, if the customer only provides the exterior surface and does not define the strength of the screw bosses, a direct print may crack during assembly. A standardized review would require adding an R0.8-R1.5 fillet at the base of the screw boss, increasing the boss wall thickness from 1.0 mm to over 1.8 mm, and considering heat-set brass inserts or metal inserts in scenarios involving repeated screw removal. Such changes may appear to increase early-stage communication time, but they can reduce the probability of late-stage rework to a controllable level.
3. Material and process windows: make parameter selection traceable
The standardization priorities differ by 3D printing process. SLA photopolymerization should focus on resin batch, layer thickness, support contact points, cleaning time, secondary curing time, and post-processing environment. SLS nylon should focus on powder refresh ratio, preheating temperature, cooling curve, packing density, and depowdering method. SLM metal printing requires records of powder batch, laser power, scan speed, layer thickness, oxygen content in the protective atmosphere, heat treatment regime, and nondestructive testing requirements. Standardization does not mean locking parameters permanently; it means establishing an "acceptable process window."
Using SLS PA12 as an example, common layer thickness can be controlled at 0.1-0.12 mm, and sufficient cooling after forming is needed to reduce warping and internal stress. If the part is for visual display, surface uniformity and color consistency should be prioritized. If it is a functional bracket, the relationship between build orientation and load direction should be recorded first. For the same long-term project, it is recommended to record material lot number, machine ID, build orientation screenshots, first-article dimensions, sampling ratio, and exception handling method for each batch to create a traceable data chain.
4. In-process inspection standards: from first-article approval to sampling ratio
The core value of a standardization system is turning "looks about right" into measurable quality indicators. For appearance parts, inspection items can include visible layer lines, support marks, color deviation, damage, deformation, contamination, and assembly feel. For functional parts, critical dimensions, hole positions, flatness, threaded insert pull-out strength, temperature resistance, or simple load tests should also be added. First-article inspection is recommended to cover all critical dimensions, while subsequent batches can use risk-based sampling ratios, such as 10%-20% for low-risk appearance parts and 30%-100% for high-risk assembly parts.
Inspection tools should also be standardized. Calipers, pin gauges, thread gauges, feeler gauges, electronic scales, and photo stations should be periodically calibrated or status-checked. For parts with tolerance requirements tighter than ±0.1 mm, process capability should be assessed in advance. If necessary, CNC finishing or post-drilling should be combined rather than judging the part as nonconforming only after printing with traditional machining tolerances applied.
5. Delivery acceptance standards: turn customer confirmation into reusable assets
Standardization at the delivery stage includes packaging, labeling, acceptance documents, and after-sales feedback. Each batch should at least be linked to the order number, part number, version number, quantity, material, process, surface finishing method, and inspection conclusion. For parts prone to deformation, partitioned packaging or custom foam inserts should be used. For painted, dyed, or polished parts, friction and contamination should be avoided during packaging. Customer feedback during acceptance should be written back into the project archive; issues such as overly tight assembly, color deviation, or visible local support marks can all become inputs for the next process or design review.
lantu3D emphasizes closed-loop management from requirements, design, and manufacturing to delivery. Standardization is not about slowing down the workflow; it is about reducing unnecessary repeated confirmations. When a customer places a second order, the platform can quickly retrieve historical versions, process windows, and inspection records, reducing the time spent on re-quoting and re-trial-and-error.
Conclusion: Standardization moves 3D printing from "can be made" to "reliably delivered"
The value of a 3D printing standardization system lies not in piling up forms, but in turning experience into an executable, traceable, and reviewable way of working. For enterprise customers, it reduces communication costs, rework costs, and quality disputes. For manufacturing service providers, it improves scheduling efficiency and cross-project reusability. In the future, as more small-batch manufacturing projects enter digital management, those who can link files, processes, inspection, and delivery data into a closed loop will be better positioned to upgrade 3D printing from a rapid prototyping tool into a stable manufacturing node.
Submit a model, drawing, image or written notes. Engineers will review material, process, finishing and delivery based on actual use.