
Introduction: Moving from isolated prints to an end-to-end deliverable engineering loop
SLM, FDM, and SLS process optimization: Key methods from parameter windows to batch stability is not simply about a machine or a material. It is about the full chain of “design—process—manufacturing—inspection—delivery.” For industry practitioners, the challenge in 3D printing is often not whether a part can be built, but whether it can be delivered with stable cost, traceable quality, and a repeatable workflow. lantu3D has long emphasized lifecycle management from concept to physical part: once a model or drawing is received, material, geometry, batch size, post-processing, inspection, and lead time should all be evaluated together, rather than making decisions based only on single-part pricing or one-off print experience.
In 3D printing process optimization, companies need to turn experiential settings into executable standards. For example, the preliminary review should confirm wall thickness, hole size, assembly clearances, support zones, and critical dimensions; during production, record layer thickness, power, scan speed, powder refresh rate, or nozzle temperature; and at delivery, build a basis for the next project through dimensional reports, appearance standards, and post-project reviews. This systematic capability determines whether 3D printing can move from “rapid prototyping” to “manageable on-demand manufacturing.”
1. Core issue: process optimization must go beyond tuning and create reusable build, post-processing, and inspection windows
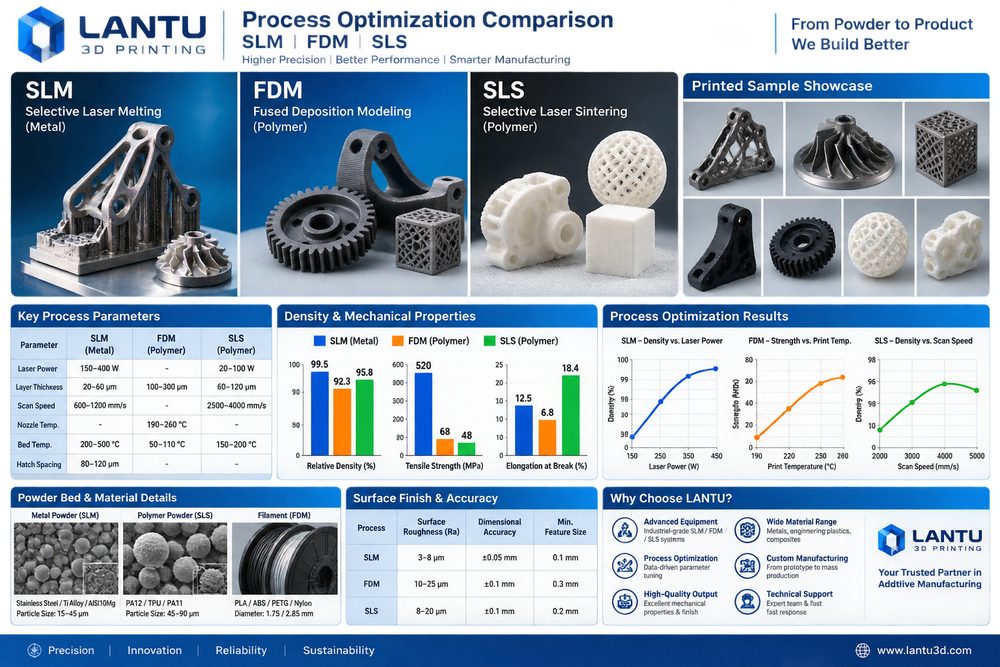
The essence of moving beyond parameter tuning is to expose and quantify uncertainty early, and to create reusable windows for build, post-processing, and inspection. Many projects focus only on material unit cost and machine hours at the quotation stage, while overlooking hidden costs such as design revisions, support removal, heat treatment, sanding or bead blasting, threaded inserts, dimensional rechecks, and packaging and shipping. For metal SLM parts, common control items include 20–60 μm layer thickness, oxygen monitoring, baseplate preheating, scan strategy, and stress-relief heat treatment. For SLS nylon parts, powder refresh ratio, bed temperature, cooling curve, and post-dyeing process directly affect warpage, toughness, and color consistency. For FDM fixtures and tooling, nozzle diameter, infill percentage, number of perimeter lines, and print orientation determine strength anisotropy.
From a management perspective, the key is not to chase the absolute limit of a single parameter, but to establish a process window. For example, engineering samples may allow shorter cycle times and less surface finishing, but assembly verification parts must include hole positions, snap fits, and mating clearances in inspection. Display parts, by contrast, need attention to surface texture, paint adhesion, and color consistency. By defining “application—risk—acceptance criteria” at project kickoff, teams can reduce rework and help customers better understand price differences.
2. Engineering decisions: how materials, processes, and post-processing should work together
Material selection should serve the use case, not just the name on the datasheet. SLM requires attention to laser power, hatch spacing, and shielding atmosphere; FDM requires nozzle temperature, bed temperature, perimeter count, and infill; SLS requires powder-bed temperature, cooling time, and powder refresh ratio. When a part needs impact resistance and lightweight performance, PA12, PA11, or glass-fiber-reinforced nylon are often the first candidates for review. When a high-fidelity surface and transparent effect are required, SLA or DLP resins are more suitable. When a project demands high-temperature strength, fatigue performance, or complex internal channels, aluminum alloys, titanium alloys, or stainless-steel metal printing can deliver real engineering value. Each choice also determines downstream processing: nylon parts may need bead blasting, dyeing, and impregnation; resin parts may need secondary curing, sanding, and coating; and metal parts may require support removal, heat treatment, machining, and nondestructive testing.
In project reviews, lantu3D typically places DFAM design, process route, and inspection method on the same table. For example, a thin-wall housing may be printable from a build perspective, but if it will later be painted and must withstand assembly screw torque, local ribs, fillets, and space for threaded inserts should be added. For a metal flow channel part, if trapped internal powder is difficult to remove, the design stage must add depowdering holes, inspection holes, or a different build orientation. The earlier an engineering decision is made, the lower the downstream cost.
3. Implementation path: using data to achieve stable delivery
In one structural sample printed by FDM, fracture occurred along the interlayer direction. The team rotated the build orientation by 90 degrees, increased infill from 25% to 45%, and moved critical hole features to post-machining. The functional test pass rate improved from 60% to 95%. The common lesson from this kind of project is to validate parameters in small batches first, then scale to stable production; confirm critical dimensions and functional surfaces first, then optimize cosmetic surfaces; define inspection samples and sampling ratios first, then discuss lead time. For R&D samples under 10 pieces, critical dimensions can be fully inspected one by one. For small-batch orders of 50–200 pieces, first-article approval, in-process sampling, final-piece verification, and exception isolation mechanisms are needed. This preserves the flexibility of 3D printing while giving customers quality certainty close to traditional manufacturing.
Digital traceability is equally important. Each batch should retain the model version, quotation version, material lot, machine ID, process parameters, post-processing method, and inspection results. When a customer places a repeat order or revises a design, the platform can quickly determine which parameters can be inherited and which risks must be reassessed. For supply-chain collaboration projects, CNC finishing, surface treatment, and assembly packaging can also be integrated into a single order view to reduce information loss across vendors.
4. Implementation checklist: turning experience into repeatable standards
A process optimization checklist should cover build orientation, support strategy, critical dimensions, surface requirements, parameter recording, first-article confirmation, and exception review. Companies are advised to embed the checklist into quoting and production workflows: first, confirm the application, load, temperature, appearance grade, and assembly relationship; second, check minimum wall thickness, hole diameter, overhang angle, powder evacuation paths, and support accessibility; third, select the material and process and specify the key parameter window; fourth, define post-processing, inspection, packaging, and delivery methods; fifth, after delivery, record customer feedback and review conclusions. The checklist does not need to be complicated, but it must be executed on every project.
For service providers, standardization does not mean sacrificing flexibility. On the contrary, only by standardizing routine risks can teams focus their energy on truly complex engineering issues. For buyers, a transparent workflow helps determine whether pricing is reasonable, whether lead times are credible, and whether quality responsibility is clearly defined. Competition in the 3D printing industry is shifting from “can it be printed?” to “can it be delivered stably, optimized continuously, and supported over the long term?”
Conclusion: improve the commercial value of 3D printing with a lifecycle perspective
The core conclusion of SLM, FDM, and SLS process optimization: Key methods from parameter windows to batch stability is that 3D printing must be managed within a complete manufacturing chain to unlock its real value. Materials, processes, equipment, quality, cost, and service are not isolated modules; they are an interdependent system. Through lifecycle management from blueprint/design to physical delivery, lantu3D connects early-stage review, process execution, post-processing inspection, and customer feedback, helping companies achieve more controllable results in R&D validation, small-batch manufacturing, and complex part delivery.
Submit a model, drawing, image or written notes. Engineers will review material, process, finishing and delivery based on actual use.