
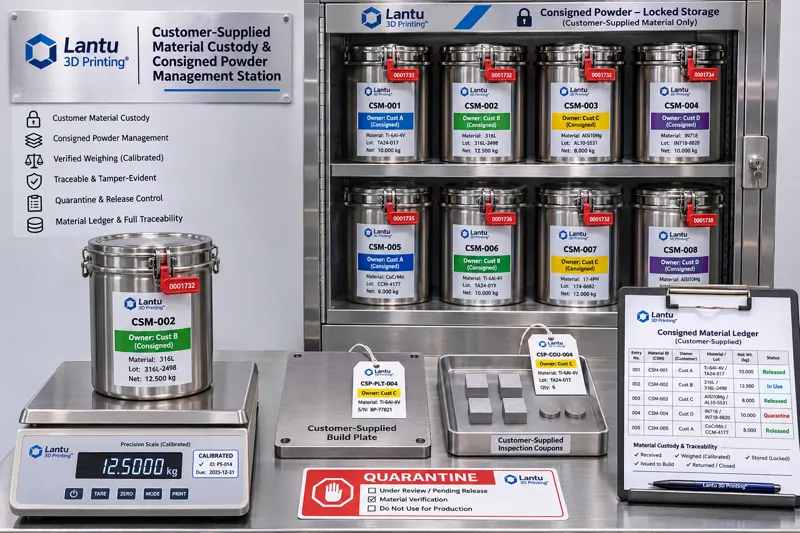
Introduction: After a Customer Delivers a Drum of Powder to the Shop Floor
In on-demand manufacturing, it is common for customers to provide powder, build plates, model files, or dedicated tooling: an aerospace customer may specify a particular batch of Ti6Al4V powder and require unused material to be returned; a medical customer may supply a validated resin batch to preserve the biocompatibility evidence chain; a tooling customer may ship build plates for conformal-cooling inserts with the order. At this point, the most frequently overlooked issues are not print parameters, but who owns the material, whether it can be mixed with in-house material, how unused material is returned, and what basis is used to settle losses. ISO 9001:2015 Clause 8.5.3 defines such items as “property belonging to customers or external providers” and requires their identification, verification, protection, and safeguarding. Where property is lost, damaged, or found unsuitable for use, the customer must be notified and documented information retained. AS9100D and IATF 16949 impose even stricter reporting timelines. In practice, most disputes do not arise from build failures, but from a receiving form that cannot clearly establish net weight: customer powder is combined with in-house recovered powder, 1.3 kg less surplus is returned, or scrapped parts are treated as ordinary waste without authorization. As a lifecycle management platform supporting delivery from drawing to physical part, lantu3D manages customer-supplied assets as an independent, auditable data chain running in parallel with the build—not merely as warehouse items with labels.
1. Define “Customer-Supplied” First: Four Asset Categories and Ownership Boundaries
Customer-supplied property is not a single type of material. It comprises four categories of assets with the same ownership principle but different control methods. Each must be specified during quotation and technical-agreement stages to avoid unclaimed property at delivery. 1. Customer-supplied powders and wire: metal powders, nylon PA12 powder, photopolymer resins, and filaments, uniquely identified by grade + lot number + container seal number. Ownership remains with the customer throughout, while the manufacturer has only entrusted processing and use rights. 2. Customer-supplied build plates and furnace-coupon carriers: LPBF build plates may be required by customers to be delivered with the part or returned. Their material, thickness, original flatness, and whether repeat blasting is permitted must be recorded. 3. Customer-supplied models and parameter files: STL/3MF files, native CAD files, customer-frozen process parameter packages, and PMI/MBD annotations remain customer property. Only controlled copies and hash values are retained. 4. Customer-supplied tooling, gauges, and comparison samples: locating fixtures, CMM gauges, approved samples, and sealed reference samples are returnable physical assets that require separate identification numbers and condition photographs.
Four boundary clauses should be fixed in the agreement: customer-supplied materials must not be diverted to other orders; they must not be blended with in-house materials or materials from other customers unless the customer provides written authorization specifying the blend ratio and lot numbers; whether scrapped parts and non-recoverable powder must be returned requires written instruction; and model copies must be deleted or archived as agreed at project completion, with deletion records issued. ISO/ASTM 52901 requirements for additive manufacturing procurement information can serve as a reference framework for the technical agreement, turning “material owner,” “blendability,” and “surplus disposition” into verifiable fields rather than vague statements such as “properly safeguarded.”
2. Incoming Receipt: Convert Verbal Handover into an Auditable Custody Ledger
The incoming-receipt process has one objective: ensure every subsequent weighing operation can be traced back to a numbered original record. Use a customer-supplied material number in the format CSM-YYYYMMDD-### as the primary key. The ledger should include at minimum: material-owner code, order number, material category, grade, lot number, container quantity and seal number, gross/tare/net weight (electronic scale accuracy no worse than ±1 g, with calibration certificate in date), COA/COC number, receipt date, storage-location code, status label (pending reinspection/released/quarantined/pending return), reinspection report number, and dual signatures from the handler and reviewer.
Reinspection is not intended to repeat customer testing; it confirms that the condition has not changed during transport and before or after opening. For metal powder, it is recommended to measure Hall flow rate in accordance with GB/T 1482 (15–53 μm powder for LPBF typically requires ≤25 s/50 g), and verify D50 using GB/T 1480 or laser diffraction. For Ti6Al4V, oxygen content should be verified against the customer certificate, with incoming limits of ≤1000 ppm oxygen and ≤300 ppm nitrogen. Moisture can be cross-verified by Karl Fischer titration or chamber dew point ≤−40 °C. For photopolymer resins, record viscosity at 25 °C and batch expiry date. For model files, calculate the SHA-256 hash and record units, coordinate system, geometry repair actions, and volume change before and after repair. If any item exceeds the technical-agreement threshold, immediately apply a “quarantined” label and notify the customer in writing within 24 hours. Do not put the material into production first and complete the paperwork later—this is one of the most common failures against Clause 8.5.3.
3. Dedicated Material Use: Three Hard Rules for Physical Segregation, Sealing, and No-Blending
Segregation depends on physical constraints, not slogans. Rule 1: one customer, one location; one lot, one container. Customer powder containers must be stored in locked dedicated cabinets or on dedicated pallets. Color coding and seal numbers must be linked to the customer-supplied material number. Shared sieving machines and powder containers with in-house recovered powder are prohibited; shared equipment must undergo material-changeover cleaning. Rule 2: recovered powder does not return to customer-supplied material by default. Even when recovered powder from LPBF has the same grade and lot number, thermal cycling can increase oxygen and nitrogen levels and shift particle-size distribution. If the customer authorizes reuse in writing, the authorization must restrict the powder to the same lot number, specify sieve mesh size and blend ratio (typically ≤30% in engineering practice), limit oxygen increase to ≤100 ppm, and document the blend as a version-controlled formula sheet linked back to the build parameter package. Rule 3: retain evidence for four changeover-cleaning steps—empty the powder chamber, vacuum under negative pressure, wipe with anhydrous ethanol, and conduct first-piece confirmation. After cleaning, weigh residual material (recommended: ≤0.5 g/m² or no visible residue by visual inspection), complete the cleaning record, and obtain second-person verification before changing to the next customer-supplied lot.
A typical failure scenario is a night shift combining Customer A’s remaining powder with Customer B’s container of the same grade “to fill the chamber.” The two powder lots have different oxygen contents and particle-size distributions, causing variation in final part density and fatigue performance. Yet the inspection report states only “Ti6Al4V,” making it impossible to prove which container was used. Physical segregation, seals, and documented changeover cleaning essentially protect the attribution of inspection conclusions.
4. Consumption Settlement: Issued Material, Recovery, and Surplus Must Reconcile
Nearly all settlement disputes arise from inconsistent definitions. “Net consumption” and “non-recoverable loss” must be separately defined and frozen in the data dictionary:
W_net = W_issued − W_recovered_usable − W_returned; W_loss = W_net − W_part − W_coupon − W_support. Here, W_issued is the net issued weight; W_recovered_usable is recovered powder deemed reusable after sieving (still customer property, merely returned to custody status); W_returned is the actual returned surplus; and W_part/W_coupon/W_support are the built weights of conforming parts, witness coupons, and supports + build plates, respectively. The reconciliation deviation |W_loss − measured loss| should be ≤1.5%. If exceeded, suspend return sign-off and issue a nonconformance report. The non-recoverable loss rate W_loss/W_issued should have a warning threshold of ≤2.0% (typically 0.8%–1.5% for metal LPBF; residual resin and cleaning losses are somewhat higher for photopolymer processes). If the threshold is exceeded, the cause must be traced to sieving, depowdering, or transfer operations.
Example: A customer-supplied Ti6Al4V order includes three builds. Issued material is 18.500 kg; usable recovered powder after sieving is 12.850 kg; returned surplus is 1.320 kg; and built parts + supports + witness coupons total 4.150 kg, while depowdering residue and below-sieve non-recoverable powder total 0.180 kg. Net consumption = 18.500 − 12.850 − 1.320 = 4.330 kg, and 4.330 = 4.150 + 0.180, giving complete reconciliation. The non-recoverable loss rate is 0.180/18.500 ≈ 0.97%, within the warning threshold. Note that the 12.850 kg of recovered powder must not be counted as cost consumption; it represents a change in the status of customer property. Reporting 4.330/18.500 as a 23.4% loss would directly trigger a commercial dispute. In shared-build scenarios, net consumption should be allocated to individual parts using weighting factors such as “scan time × number of layers × support volume.” The allocation rule and version number must be frozen before calculation, and the denominator should use the number of conforming delivered parts so that scrap and rework are reflected through yield.
5. Machine Release and Lot Binding: Customer-Supplied Material Cannot Exist Only in the Ledger
Even a complete ledger is insufficient if the build job lists only a material grade; the traceability chain remains broken. Machine-release controls should mandate six bindings: record the customer-supplied material number and seal number in the work order; record the parameter-package version and hash; record machine number and chamber dew point; place witness coupons in the same lot and orientation; require the “material owner” field in inspection records; and include a customer-supplied material declaration page in the delivery report. CMM dimensional reports, tensile/density reports, and powder reinspection reports should all be indexed by the same customer-supplied material number, forming a traceable evidence package. Acceptance rules should address uncertainty bands in accordance with ISO 14253-1, and laboratory capability should be confirmed in accordance with ISO/IEC 17025. If the parameter package changes during production, reassess the suitability of customer-supplied material through the ECN process. Verbal authorization to “continue using the previous parameter version” is prohibited.
6. Surplus Return and Scrap Disposition: Someone Must Sign at the End
Three actions are required at project closeout. First, reweighing and sealing: reweigh surplus material, recovered powder, and build plates separately, apply new seals, and attach a return list containing the customer-supplied material number, net weight, status, container quantity, and photographs. Together with the customer receipt, this completes the closed loop. Second, written disposition instruction: select one of four options—return surplus, transfer to the next batch, retain for 30 days, or authorize destruction—and obtain signature from the customer’s designated contact. Send a reminder seven days before the retention period expires; if no response is received, follow the default clause of the technical agreement and retain evidence. Third, scrapped parts and unusable powder: safety-critical or confidential parts must be destructively marked, such as by drilling holes or cutting corners, before disposition under customer authorization. They must not enter ordinary scrap streams. If non-recoverable powder contains active metals, transfer it in accordance with the MSDS and hazardous-waste manifest requirements, and enter the manifest number back into the ledger.
7. 30-Day Implementation Plan and Checklist
Week 1: revise the technical-agreement template and add a “customer-supplied asset list” appendix, defining material owner, blendability, surplus disposition, and reporting timeline as fields. Week 2: establish customer-supplied material numbering rules and a custody ledger; provide dedicated locked cabinets, color coding, seals, and calibrated electronic scales. Week 3: modify work-order and inspection templates to make “material owner/customer-supplied material number/parameter-package hash” mandatory fields. Week 4: run one actual order end to end and conduct one simulated return-signature process. After implementation, perform eight self-checks: 1) Are ownership details listed separately for all four asset categories? 2) Are calibration certificates for every scale current? 3) Are incoming reinspection thresholds written into the agreement? 4) Is each customer assigned a dedicated location with intact seals? 5) Are material-changeover cleaning records verified by two people? 6) Is blending supported by written authorization and a formula version number? 7) Do consumption reconciliation deviation and loss rate have warning thresholds? 8) Are return receipts and hazardous-waste manifests entered back into the ledger?
Conclusion
Customer-supplied material governance is not a warehouse detail. It translates the legal and standards-based obligation of “customer property” into measurable figures: one customer-supplied material number, one ledger including tare weight, one material balance reconciling within 1.5%, and one signed return list. When issued material, recovery, surplus, and built parts all reconcile, and the parameter package and inspection records can be traced back to the same lot, delivery includes more than conforming parts—it includes an auditable account of customer assets. For platforms focused on delivery from drawing to physical part, this account is as important as the dimensional inspection report.
Submit a model, drawing, image or written notes. Engineers will review material, process, finishing and delivery based on actual use.