
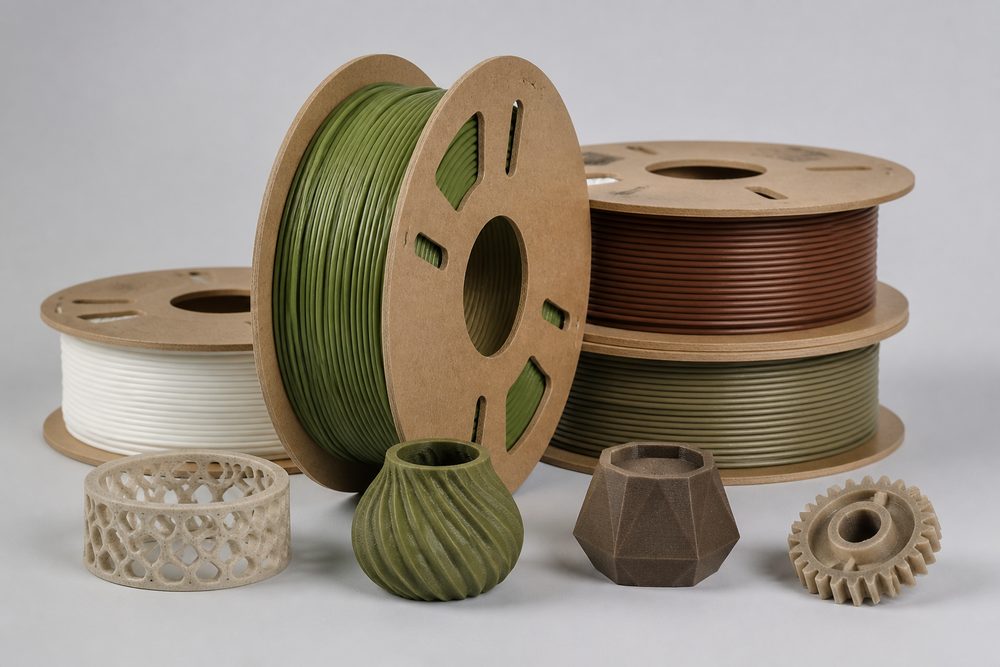
Introduction: The 3D Printing Industry Faces an Inevitable Choice of Environmental Transformation
According to data from the Wohlers Report 2024, the global additive manufacturing industry has an annual growth rate of 18.3%, but traditional petroleum-based materials still account for more than 75%, and carbon emissions are becoming increasingly prominent. The EU Carbon Border Adjustment Mechanism (CBAM) has already brought plastic products under regulatory control, and China’s “dual carbon” goals require the manufacturing sector’s carbon emission intensity to fall by more than 18% before 2030. If 3D printing companies do not actively transform, they will face three major risks: environmental compliance costs rising by 15-25%, restricted access to international orders, and downgraded brand ESG ratings.
Taking a 3D printing service provider in East China as an example, its annual output of 120 tons of PA12 nylon parts resulted in a carbon emission intensity of 8.2 tons CO₂/ton of material, far exceeding the industry benchmark of 6.5 tons CO₂/ton. When a customer requested carbon footprint documentation, the company lost a European order worth 3.8 million yuan due to the lack of an environmentally friendly material application plan. This case highlights the urgency and commercial value of environmental transformation.
1. Technological Breakthroughs and Industrial Applications of Bio-Based Materials
Bio-based materials refer to polymer materials made from renewable biomass resources such as corn, sugarcane, and castor oil. Their carbon footprint is 40-80% lower than that of petroleum-based materials. At present, the mainstream bio-based materials in the 3D printing field mainly include three categories: PLA, PHA, and PA11, each with specific technical parameters and application scenarios.
PLA (Polylactic Acid): Technical Optimization of an Entry-Level Eco-Friendly Material
Material properties: PLA is made by fermenting corn starch, has a biobased carbon content of 100%, and is the most mature environmentally friendly material for 3D printing. It has a relatively low melting point (150-160°C) and a glass transition temperature of 55-65°C, making it suitable for FDM processes.
Key process parameters:
- Extrusion temperature: 190-220°C (40-50°C lower than PA12)
- Heated bed temperature: 50-60°C (to prevent warping)
- Print speed: 40-80 mm/s (too fast will reduce interlayer bonding strength)
- Layer height: 0.1-0.3 mm (0.2 mm is recommended to balance efficiency and quality)
Performance limitations and improvements: Pure PLA has a tensile strength of 50-60 MPa, but an impact strength of only 2.5-4.0 kJ/m², with poor heat resistance (HDT about 55°C). By adding natural fillers such as bamboo fiber (20-30%) and wood flour (10-15%), the impact strength can be increased to 6-8 kJ/m² and the HDT to 75-85°C, while maintaining bio-based characteristics.
Application case: An educational equipment manufacturer used PLA + 20% bamboo fiber composite material to print teaching models. The products passed the EU EN71-3 toy safety standard, the unit cost was reduced by 35% compared with imported PLA, annual production capacity reached 80,000 units, and the products have entered educational markets in 15 countries.
PHA (Polyhydroxyalkanoates): A Breakthrough in High-Performance Bio-Based Materials
Technical advantages: PHA is synthesized through microbial fermentation, has complete biodegradability (with a degradation rate of over 90% in seawater within 180 days), and offers a wide range of tunable properties. The tensile strength of PHB (polyhydroxybutyrate) reaches 40-50 MPa, and the elongation at break of PHBV (hydroxybutyrate-hydroxyvalerate copolymer) can exceed 300%, far superior to PLA’s 5-10%.
Process key points: Controlling PHA crystallinity is crucial to print quality. A stepwise cooling strategy is recommended:
- Extrusion temperature: 175-185°C (to avoid thermal degradation)
- Printing environment temperature: 25-30°C (to control crystallization speed)
- Post-processing: annealing at 80-100°C × 2 hours increases crystallinity from 45% to 65% and improves dimensional stability by 40%
Cost challenge: At present, PHA raw material costs 250,000-350,000 yuan/ton, which is 3-4 times that of PLA. However, by adopting mixed microbial fermentation processes (such as the engineered Ralstonia eutropha strain developed by MIT’s team), raw material costs can be reduced to 150,000-200,000 yuan/ton, with commercial mass production expected by 2025.
PA11 (Polyamide 11): A Benchmark for Industrial-Grade Bio-Based Materials
Material source: PA11 is synthesized from castor oil and has a bio-based carbon content of about 40%. It is a direct replacement for petroleum-based PA12. Its water absorption rate is 1.9% (PA12 is 1.5%), but it offers better toughness, with a low-temperature impact strength of 40 kJ/m² (PA12 is 30 kJ/m²).
SLS process parameter comparison:
| Parameter | PA11 | PA12 | Difference Explanation |
|---|---|---|---|
| Laser power |