
Introduction: Shift Handover Is the Most Overlooked Capacity Breakpoint in 3D Printing Workshops
In a 3D printing workshop, equipment may run continuously for more than ten hours, and a single build job often spans two or even three shifts. The day shift spreads powder, initiates the process, and starts the build; the night shift monitors the melt pool and oxygen level; the following morning shift depowders, cuts parts from the build plate, and sends them for inspection. The job itself is continuous, but personnel rotate. What truly determines whether a batch can be completed on schedule is often not the machine parameters, but the quality of the brief handover between the three shifts.
Many on-site issues point to the same root cause: information known by the previous shift is unknown to the next. A protective lens may be close to its alarm threshold without being recorded; the seventh part on a build plate may have shown balling, but this was mentioned only verbally; the recovered-powder sieve may not yet have been cleaned; or two customer-added parts may not have been scheduled. Once such information exists only in an operator's memory, it effectively does not exist. By the time the next shift discovers it, an entire build may already have been scrapped or delivery delayed.
1. What Must Actually Be Handed Over: Dividing Implicit Information into Four Status Categories
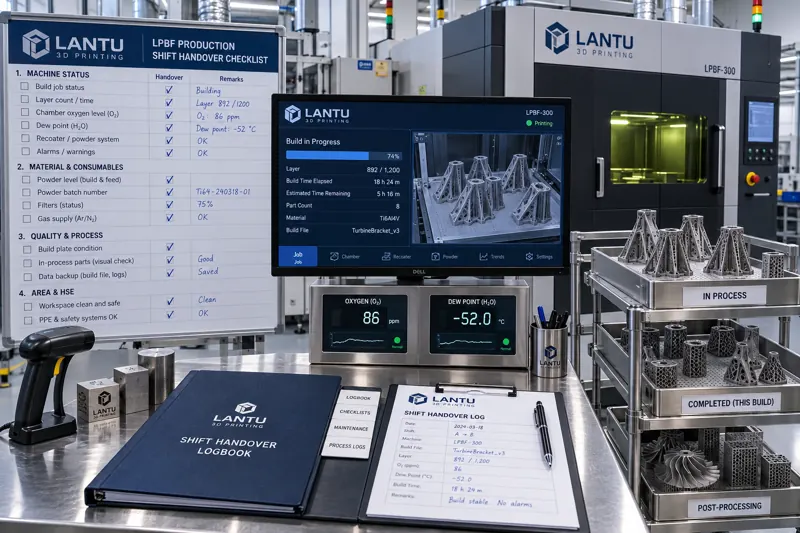
An effective shift handover is not simply saying a few words. It means structuring the status of ongoing operations. For a 3D printing workshop, the information to be transferred can be grouped into four categories.
The first category is equipment status. This includes the machine's current operating mode (printing, standby, depowdering, maintenance), cumulative laser operating hours and power calibration date, protective-lens transmittance or replacement date, current oxygen and dew-point readings, circulating-water temperature and filter differential pressure, and recoater blade service time. These are not binary judgments of whether something is normal; they are numerical trends. Saying only that the machine is normal removes the basis on which the next shift can make decisions.
The second category is job-in-process status. Each active build job should include the job number, machine location, layers completed and remaining, estimated completion time, whether printing was resumed after an interruption, powder batch number and reuse count, and downstream post-processing route, such as stress-relief annealing, wire EDM, or hot isostatic pressing. 3D printing jobs have long cycle times, and cross-shift continuation is routine, so progress information must be measurable.
The third category is exceptions and deviations. Every exception during the shift—including alarm codes, downtime duration, corrective actions, whether work in process was affected, and whether quality intervention is required—should be documented individually. This is especially important for issues that appear manageable, such as slight interlayer warping, localized uneven powder layers, or oxygen levels that briefly exceed the limit before returning to normal. Such deviations may not stop the machine immediately, but can directly affect the final part's metallurgical quality.
The fourth category is pending actions and commitments. This includes the process stage of parts scheduled to ship the next day, the effective time of customer-requested technical changes, materials that must be replenished, and batches awaiting quality release. Together, these four categories form a complete shift-handover package.
2. Why Verbal Handover Will Inevitably Fail
Many workshops rely on briefly discussing matters during the pre-shift meeting. The problem with verbal handover is not attitude, but structure. First, under pressure, people selectively retain information, and exception details are the first to be lost. Second, spoken handovers often lack numerical data, preventing the incoming engineer from assessing trends. Third, verbal information cannot be traced, making it impossible during a later review to confirm whether something was actually communicated.
A subtler risk is unclear accountability. When two shifts interpret the same statement differently—for example, “keep using that batch of powder for now”—disputes arise during quality traceability: Was the powder approved for use, or was it awaiting sieving? Written handover records convert conditions such as “approved for use until what threshold” into verifiable requirements, naturally eliminating disputes. For parts subject to customer audits or traceability requirements, handover records are themselves part of the process evidence.
3. Standard Work for Shift Handover: Time, Location, and Sequence
To make shift handover a standard operation, three elements must be defined.
Time window: A 15- to 20-minute overlap period is recommended, with both outgoing and incoming personnel present. A shorter period does not allow sufficient time for a complete on-site inspection; a longer one increases labor cost. The overlap is necessary because many conditions must be confirmed against the actual equipment, not merely against paperwork.
Location and route: Handover should follow a fixed route: first review the job queue and alarm history on the main control screen; then inspect each machine to confirm operating status and consumable levels; finally, check the physical items and labels in the work-in-process holding area. The value of a fixed route is that it does not depend on individual habits. Every shift checks in the same order, greatly reducing the chance of omissions.
Sequence and sign-off: Hand over exceptions first, then jobs, and finally pending actions. Exceptions have the highest priority; if time is limited, routine pending items—not exceptions—should be compressed. Once the handover is complete, both parties sign off. The incoming shift must confirm that the information has been received and understood before the outgoing shift leaves. Sign-off is not a formality; it fixes the point at which responsibility transfers.
4. Cross-Shift Consistency: Parameters, Acceptance Criteria, and Operating Practices
Shift handover addresses not only continuity of information, but also consistency. If the day and night shifts use different levels of force for support removal, different grinding sequences, or different surface acceptance criteria for the same part, final delivery consistency will fluctuate. Customers do not see which shift made a part; they see whether the batch is consistent.
The solution is to quantify acceptance criteria and formalize them in work instructions: allowable support-remnant height, abrasive grit sequence, surface-roughness comparison coupon number, and permitted scope of manual rework. During handover, the key is to confirm whether the previous shift followed the same criteria and whether any parameters were adjusted based on experience. Any deviation from standard parameters must record its reason and result; otherwise, the next shift cannot determine whether it was an effective optimization or the beginning of a deviation.
5. Quantitative Management of Shift Handover: From Records to Metrics
Shift-handover records have value only when they are used. Three metrics can be extracted from the records for trend tracking.
Handover completion rate: Audit the percentage of required fields completed in handover records, including equipment readings, job-in-process progress, exception entries, and pending actions. The target should be no lower than 98%. The item most frequently omitted should become the next training priority.
Handover-related exception ratio: Measure the proportion of shift exceptions that already existed during the previous shift but were not recorded. A declining figure indicates improving handover quality; if it does not decline over time, records and actual execution are likely disconnected.
Cross-shift first-piece pass-rate variance: Compare first-piece inspection results after the same job is continued by different shifts. A large variance usually indicates inconsistent parameters or operating criteria rather than an equipment issue.
These three metrics require no additional investment. They only require structured handover records and monthly consolidation. Their value lies in converting the question of whether shift handover is being performed well from a subjective impression into measurable data.
6. Common Misconceptions and Responses
The first misconception is turning shift handover into a form-filling competition, where records become increasingly long but no one reads them. The response is to limit the number of required fields, typically to no more than 15, with all other information treated as supplementary notes.
The second misconception is valuing handover only when a problem occurs. Workshops with good handover practices rarely experience incidents caused by handover, which can make the investment seem unnecessary. In reality, it is a typical preventive investment whose benefits are reflected in incidents that never occur.
The third misconception is omitting handover during single-person night shifts. Single-person shifts depend even more heavily on written records because no one is available for face-to-face questions. In such cases, the level of recording detail should be increased, especially for exception entries.
Conclusion
Continuity in a 3D printing workshop depends on the lossless transfer of four categories of status between shifts: equipment, jobs, exceptions, and pending actions. By replacing verbal instructions with structured checklists, replacing “normal” with specific readings, and replacing experience-based judgment with quantitative criteria, shift handover becomes a genuine capacity-protection process rather than a formality. For workshops handling low-volume, high-mix, long-cycle jobs, the marginal return from these three measures is often greater than that of adding another machine.
Submit a model, drawing, image or written notes. Engineers will review material, process, finishing and delivery based on actual use.