
Introduction: An Engineering Variable Too Often Dismissed as “Antistatic Clothing”
In the work instructions of most 3D printing workshops, static electricity appears only twice: “wear antistatic clothing” in occupational health training and “dry sweeping is prohibited” in powder-cleaning procedures. Yet the problems that are genuinely difficult to resolve on the shop floor are caused neither by people nor by brooms. The same batch of Ti6Al4V powder may show weighing drift of 0.3% to 0.8% after sieving; reclaimed powder may form rings on the inner wall of transfer containers; intermittent thin powder bands may appear ahead of the recoater during spreading; and resin parts may attract another layer of fine dust after cleaning. The common upstream cause is charge accumulated by powder during sieving, pneumatic conveying, pouring, and wiping. However, workshops often lack any measurable value, defined acceptance threshold, or record traceable to a build ID. lantu3D manages delivery from drawings to physical parts as a lifecycle chain. Electrostatic condition is a process variable that has long been missing from that chain: it is neither an item on a personal protective equipment list nor an appendix to temperature-humidity records, but a process condition that must be defined, measured, and released independently.
I. First Define the Boundaries: Protecting People, Protecting Parts, and What This Layer Controls
The most common mistake is to place static electricity directly under EHS dust-explosion control. The three areas are adjacent, but their subjects are fundamentally different. The EHS layer addresses questions such as: “Will operators inhale metal powder? Will they be injured by laser exposure? What happens if a dust cloud encounters an ignition source?” Its outputs are PPE lists, interlocks, and emergency response cards. The workshop environmental-control layer addresses: “At 45%±5% relative humidity, will powder absorb moisture and then vaporize in the melt pool to form porosity?” Its outputs are continuous temperature-humidity records and moisture-content gates. This layer addresses a different question: “Has charge accumulated between powder and containers, screens, piping, and work surfaces been discharged, and on what basis may this container of powder be loaded into the machine?” A simple rule for classifying the layer is this: if it can be expressed as a measured grounding resistance, a surface-resistance classification table, a charge-decay curve, or a per-shift inspection log, it belongs to the electrostatic engineering layer. Its humidity purpose also differs from that of 8582: the upper humidity limit there prevents moisture absorption, while the lower humidity limit here provides a discharge path for charge. The two operating windows must overlap rather than replace one another.
II. Four Types of Measurement Points and Determinable Thresholds
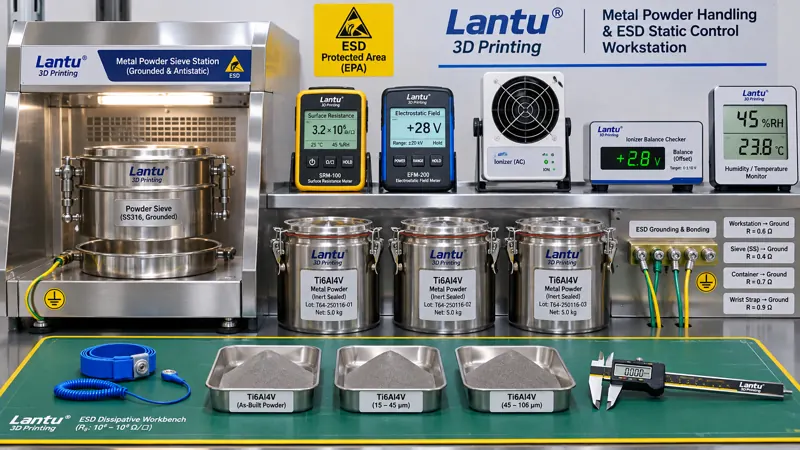
The first category is the discharge path. Equipment protective earth, sieving stations, transfer carts, powder containers, and bench mats must be equipotentially bonded. The connection resistance from the common grounding point to each endpoint should be ≤1 Ω. The resistance-to-ground of antistatic work surfaces should be maintained within the dissipative range of 10⁵–10⁹ Ω; below 10⁵ Ω, personnel electric-shock and current-limiting risks must be assessed, while above 10⁹ Ω, discharge is too slow and the surface effectively behaves as an insulator. The classification principles in IEC 61340-5-1 and ANSI/ESD S20.20 may be used as references. It is not necessary to copy an entire system, but the workshop must define in its own work cards which points are measured, which instrument is used, how often measurements are taken, and what happens when limits are exceeded. The second category is workstation electrostatic potential. Use a non-contact electrostatic field meter at four locations: the pouring port, above the screen, the weighing bench, and inside the powder-bed chamber door. A limit of ≤±100 V is recommended around sensitive electronic balances and sensors, and ≤±500 V for general workstations. Readings must be taken while equipment is operating; a zero reading when equipment is stopped is meaningless. The third category is charge decay. For samples of bench mats, containers, and filter media, the recommended decay time from ±1000 V to ±100 V is ≤2 s, or the half-life should be recorded and a baseline frozen. Newly replaced plastic liners, new batches of filter bags, and newly cleaned containers must all be retested. The fourth category is environmental neutralization. Relative humidity should remain above 40% RH and overlap with the 45%±5% range required for build stability; the combined operating window should therefore be 45%–50%. Ionizing air blowers should be used only where insulating components are unavoidable, with balance voltage ≤±35 V and decay time ≤2 s. They must be included in inspections rather than forgotten after installation.
III. Four Paths by Which Static Electricity Affects Build Quality
Path one: sieving and screen clogging. Charged fine powder adheres to screen wires, reducing effective open area. Oversize material is then incorrectly classified as “agglomerated powder,” and the available quantity of reclaimed powder is underestimated. Path two: weighing and blending. Powder charge varies with ambient humidity and conveying speed, causing irregular electronic-balance drift of 0.3%–0.8%. Blend ratios and net material consumption per part are distorted, contaminating activity data used in cost sheets and carbon accounting. Path three: powder spreading and powder layers. Charged powder adheres to the recoater leading edge and forms thin powder bands near substrate edges, causing local powder-layer thickness variation. Subsequent balling and lack-of-fusion defects may then be incorrectly attributed to laser parameters. Path four: surfaces and cleanliness. Resin parts and cleaned metal parts experience greater dust attraction, cleanliness retesting of internal flow channels fails, and adhesion before blasting or coating becomes unstable. The common feature of all four paths is that the symptoms appear to belong to four separate stages—sieving, metering, building, and post-processing—while the root cause lies in the same place. Without electrostatic records spanning process stages, personnel can only adjust parameters one stage at a time.
IV. Engineering Controls: Discharge First, Neutralization as Backup
The control sequence must not be reversed. First, establish conductive paths: bond metal containers, sieving machines, transfer carts, and piping flanges, then connect them to a single grounding point. Do not use “application of antistatic agent” as a substitute for bonding conductors. Select dissipative materials for benches and floors and include them in the classification table. Insulating plastic trays may be used only for short-term transfer and must be paired with ionization. Next, classify container and tooling materials. Based on surface resistance, classify containers, liners, scoops, and screen frames as conductive, dissipative, or insulating. Insulating items must not directly contact powder intended for machine loading. For every newly purchased item batch, perform spot checks of surface resistance upon receipt and retain samples. Third, link humidity to process control: suspend sieving and pouring when humidity falls below 40% RH. Work may resume only after humidity returns to the combined operating window and electrostatic potential has been rechecked. Event timestamps must be linked to the current work order and build ID. Only then should active neutralization equipment such as ionizing air blowers and static-elimination bars be used, and only at stations where material substitution is not feasible. It must be emphasized that blowing powder with compressed air is both a dust-explosion risk and a strong charge-generation process; it must never be used as a powder-cleaning method.
V. Per-Shift Inspection Logs and A/B/C Three-State Release
A six-field inspection card is recommended: measured shift humidity and data-logger ID; maximum electrostatic potential at the four workstations; sampled equipotential-bonding resistance points and values; ionizing blower balance voltage; powder lot numbers and build IDs involved in sieving, pouring, and weighing during the shift; and the inspector and verifier. Results are classified into three states. State A means all six items are within limits and machine loading is permitted. State B means one item is slightly out of tolerance—for example, potential between ±500 V and ±1000 V, or decay time of 2–4 s. Release is permitted only after doubled-frequency retesting and first-piece standard-sample confirmation, and the lot must be separately identified. State C means an open grounding circuit, humidity below 40% RH, potential exceeding ±1000 V, or decay time exceeding 4 s. Machine loading is immediately frozen, and all builds powder-spread since the last qualified point must be reviewed, including layer images, weighing records, and witness-specimen results. No concessionary release is allowed without acceptable evidence. Recovery requires remeasurement of grounding and potential, a new first-piece verification, and joint signoff by process engineering and quality; simply adding a record afterward is not sufficient to restart the machine. Logs should be retained under dual indexes of powder lot number and equipment ID, enabling any delivered part to be traced back to the electrostatic condition of its production shift. Together with inspection lots, heat-certification chains, and measurement traceability, this forms the delivery evidence package rather than a separate system.
VI. Thirty-Day Implementation and Common Misconceptions
Week one: establish a baseline. Measure the four categories of points throughout the workshop, map high-charge stations, and prioritize pouring ports and sieving stations. Week two: standardize the hardware. Add bonding conductors, replace bench mats and containers with dissipative alternatives, equip insulating stations with ionizing blowers, and verify balance voltage. Week three: issue work cards and provide training. Post inspection cards, classification tables, A/B/C criteria, and recovery procedures. Have operations and quality each practice retesting and dual signoff. Week four: conduct a traceability drill. Randomly select a delivered part and require the team to retrieve the shift electrostatic inspection, powder lot number, build layer number, and first-piece verification record within 30 minutes. The target first-pass retrieval rate is ≥95%. Four common misconceptions are: treating the issuance of antistatic clothing as completion of electrostatic control; setting only an upper humidity limit to prevent moisture absorption while omitting a lower limit to prevent charge accumulation; measuring only equipment protective earth while ignoring powder-contacting endpoints such as containers and bench mats; and failing to retest surface resistance and decay time after replacing screens, liners, or cleaning agents. All of these can be prevented through mandatory fields on the inspection card.
Conclusion
Static electricity has long been a variable in 3D printing workshops that “everyone mentions, but no one assigns a value.” Separating it from PPE lists and temperature-humidity records, defining five measurable groups—discharge paths, surface resistance, electrostatic potential, charge decay, and a humidity floor—and linking results to release criteria for work orders, powder lots, and build IDs completes the chain from design to physical delivery. For lantu3D, the value is not merely a few additional record sheets. It is the ability, when screen clogging, weighing drift, intermittent powder layers, or surface dust attraction reappears, to first eliminate a verifiable common root cause rather than repeatedly adjusting parameters across four process stages.
Submit a model, drawing, image or written notes. Engineers will review material, process, finishing and delivery based on actual use.