
Introduction: Why 3D Printing Especially Needs Knowledge Management
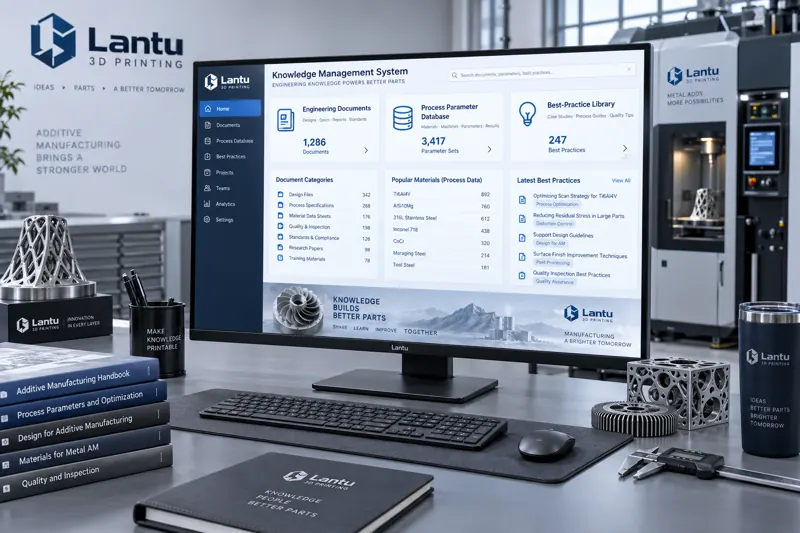
3D printing is a manufacturing method highly dependent on experience. On the same SLM machine, changing a batch of powder, adjusting laser power, or modifying a scanning strategy can lead to vastly different forming quality. In reality, a large amount of process know-how is locked in the minds of a few senior engineers and scattered across WeChat groups, emails, and personal notes. Once employees leave, that experience is lost with them. Even more troublesome is that many hard-earned lessons are never recorded, causing similar defects to occur repeatedly and teams to fight the same fires again and again. When a company moves from single-piece prototyping to small-batch production with multiple materials and parallel processes, without a knowledge management system, delivery stability and scalability will be constrained by experience bottlenecks.
1. The Core Asset of Knowledge Management: The Process Parameter Library
The most fundamental and also most easily overlooked asset is a structured process parameter library. It should not merely be screenshots of default machine parameters, but should cover the full chain of material—equipment—process window—result. For example, PA12 nylon under the SLS process may have a recommended printing temperature of 185–195°C, a layer thickness of 0.1–0.15 mm, and a preheating temperature about 3–5°C below the melting point; 18Ni300 maraging steel under SLM may use laser power of 200–370 W, scanning speed of 800–1200 mm/s, and layer thickness of 0.03–0.05 mm. Each parameter entry should include corresponding part features, forming quality metrics such as density, dimensional accuracy, and surface roughness, as well as traceable batch numbers. In this way, similar parts in the future can directly reuse existing data instead of starting from scratch. The value of a parameter library lies in its ability to be searched, reused, and verified.
2. Turning DFM Guidelines into Executable Review Checklists
Design for manufacturability (DFM) is knowledge that 3D printing companies should formalize most urgently. Instead of relying on verbal reminders based on experience before every quotation, it is better to turn general rules into a structured review checklist: minimum wall thickness, such as about 0.5–1 mm for resin SLA, about 1–1.5 mm for nylon SLS, and about 0.3–0.5 mm for metal SLM; overhang angle, where self-supporting structures generally require ≥45°; minimum feature size; assembly clearance, where functional fits are recommended at 0.1–0.3 mm; support accessibility and removal cost, and so on. The checklist should be continuously iterated based on real cases—whenever rework occurs because a rule was missing, that rule should be added to the guidelines. When DFM guidelines become checkable review items, even newcomers can block most foreseeable risks during the quotation stage.
3. Failure Case Library: Turning Pitfalls into Organizational Assets
Failure is the most expensive knowledge and also the easiest to discard. It is recommended to establish a failure case library using a unified template to record part geometry features, process route, failure symptoms such as cracking, warping, balling, lack of fusion between layers, and dimensional out-of-tolerance, root cause analysis, corrective actions, and verification results. For example, a thin-walled aluminum alloy part warped after being removed from the build plate; the root cause was accumulated thermal stress and a single direction of stress release, and the corrective measures were to add an annealing process and optimize scan partitioning. In another case, a deep-cavity structure was scrapped during post-processing because supports were inaccessible; the root cause was that support removability had not been evaluated during the DFM stage. A failure case library makes it possible to avoid making the same mistake a second time, and its value is often higher than that of successful cases.
4. Continuous Accumulation of Equipment and Material Data
Equipment status and material batches also need to be recorded. The same grade of powder can differ between batches in particle size distribution, oxygen content, and flowability, which directly affects printing stability. Establishing material batch files, including supplier, batch number, key physical and chemical indicators, and applicable process windows, as well as equipment operation logs, including key component life, maintenance records, and process drift curves, can help quickly determine whether quality fluctuations are caused by material, equipment, or process variables. When equipment maintenance plans, powder recycling rates, and environmental temperature and humidity are all incorporated into the same data chain, quality traceability gains a solid data foundation.
5. Classification, Retrieval, and Reuse Mechanisms: Making Knowledge Truly Usable
Accumulation is only the first step; the key is whether the knowledge can actually be used. Knowledge should be tagged across multiple dimensions, including part type, material, process, and problem, and should support scenario-based retrieval. For example, entering “thin-walled aluminum alloy SLM warping” should directly retrieve parameter recommendations, DFM taboos, and failure cases. Beyond retrieval, highly reusable knowledge should be brought forward into process cards and templates: quotation templates, DFM review forms, post-processing SOPs, and first-article inspection checklists. Only when engineers see the right knowledge at the right moment does knowledge management move from the archive room to the production line.
6. Implementation Path and Common Misconceptions
A practical implementation path should move from light to heavy: first pilot with a single process, such as SLS nylon, and use existing documents to consolidate a parameter library and DFM checklist; then establish a failure case review mechanism to turn weekly quality issues into organizational memory; finally, connect equipment and material data to form a traceable closed loop. Common misconceptions include equating knowledge management with buying a system, whereas tools are only carriers and content operation is the core; recording only successes and not failures; and allowing knowledge to become outdated quickly because no one maintains it after it is written. Sustainable knowledge management depends on embedding recording, review, and reuse into daily routines, rather than treating it as a one-off project.
Conclusion
The competitiveness of 3D printing companies increasingly depends not on the performance of a single machine, but on whether they can systematize scattered experience and make one-off successes repeatable. By building a knowledge management system centered on process parameter libraries, DFM guidelines, failure case libraries, and equipment and material data, companies can stabilize quality, shorten the learning curve, and transform individual experience into organizational assets as they expand from prototyping to small-batch delivery.
Submit a model, drawing, image or written notes. Engineers will review material, process, finishing and delivery based on actual use.