
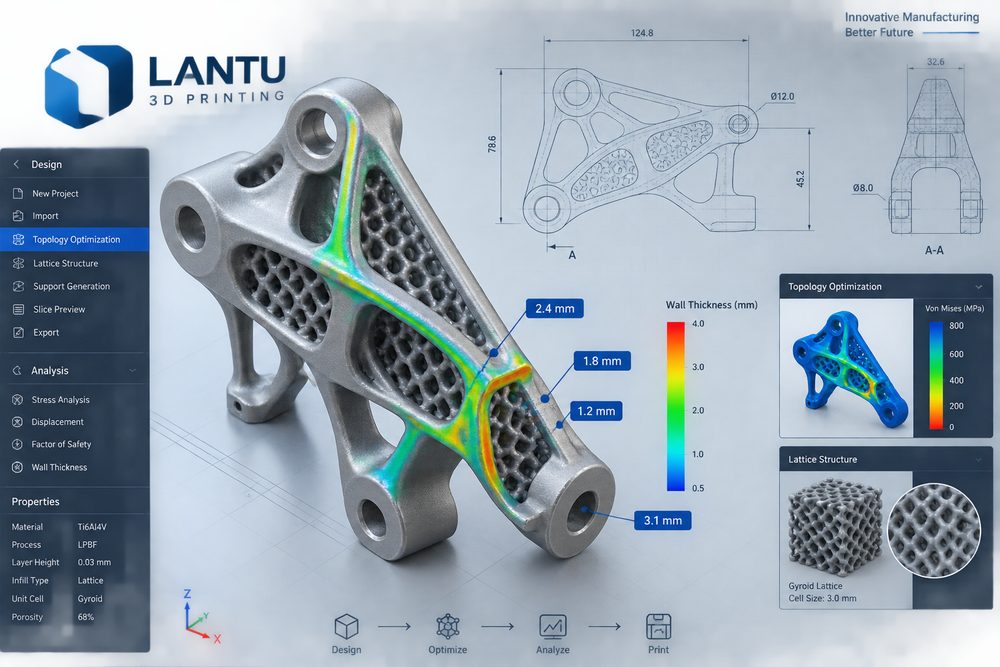
Introduction: A Key Step from Single-Part Prototyping to Deliverable Projects
3D printing design optimization is not something to think about only after a model has been sent to the machine; it is a systematic effort that runs through requirement clarification, structural design, process planning, quality verification, and delivery review. In project practice, lantu3D pays more attention to the full lifecycle closed loop from concept and design to physical delivery: first clarify the use case, loads, appearance, assembly, and budget; then quantify risks through materials and processes; and finally make the results traceable through inspection, post-processing, and file archiving. For enterprise customers, a good-looking sample does not mean the project is successful. Only when dimensions, surface quality, strength, lead time, and cost are all under control does 3D printing truly become a reliable manufacturing capability.
1. Core Issue: The Goal of Design Optimization Is Not to Make the Model More Complex, but to Make Manufacturing Results More Stable and Economical
In scenarios where SLA, SLS, MJF, SLM, and FDM processes coexist, the same 3D data can produce completely different results depending on material shrinkage, layer thickness, support strategy, and post-processing path. Taking common engineering parts as an example, SLA resin parts typically use a layer thickness of 0.05-0.1 mm to achieve a fine surface finish, but long-term load-bearing capacity and temperature resistance must be evaluated carefully; SLS PA12 parts are suitable for complex internal cavities and small-batch functional verification, and common dimensional tolerances should be reserved at about ±0.2 mm or ±0.3% depending on part size; metal SLM parts also need to consider thermal stress, support removal, heat treatment, and machining datums. Common experience includes the following: the minimum load-bearing wall thickness for SLS nylon functional parts is usually recommended to be no less than 1.2-1.5 mm; thin-wall areas of resin appearance parts should be checked for warping risk; assembly hole positions should reserve 0.1-0.3 mm clearance depending on material and post-processing; and sharp corners can be replaced with R0.5-R2 fillets to reduce stress concentration.
2. Engineering Analysis: Bring Uncertainty Forward to the Design Review Stage
Many failures do not come from insufficient equipment capability, but from requirements that were never expressed in engineering terms. For example, for appearance parts, it is not enough to say that the surface should be good; acceptable texture, paint color variation, sanding areas, and visible assembly surfaces should be specified. For functional parts, saying that the strength should be high is also not enough; the main load direction, peak load, operating temperature, fatigue frequency, and safety factor should be defined. lantu3D usually recommends building a project risk table before quoting, listing wall thickness, hole diameter, overhangs, slender rods, threads, inserts, post-processing, and inspection methods one by one. The benefit is that customers can make clear trade-offs among price, lead time, and performance instead of discovering after delivery that the model needs to be remade.
3. Solution: Layered Control for Parameters, Samples, and Batch Delivery
For a reliable 3D printing project, a three-layer validation method is recommended. The first layer is digital validation: check whether the STL/STEP files contain broken surfaces, non-manifold edges, overly thin walls, or undefined assembly clearances. The second layer is process validation: confirm the material grade, printing orientation, layer thickness, infill or scan strategy, support contact area, and estimated shrinkage compensation. The third layer is physical validation: verify the solution through first-article measurement, assembly trial fit, surface reference samples, and necessary mechanical testing. If the project is planned to expand from 1 sample to 20-200 pieces in small batches, it is even more important to fix the version number, process sheet, inspection form, and packaging requirements in advance to avoid unexplained differences between batches.
4. Implementation Checklist: Actionable Steps from Communication to Acceptance
It is recommended to follow five steps: first identify the load path and appearance surfaces; second check the minimum wall thickness, hole diameter, and overhang angle; third determine the printing orientation and support contact areas; fourth validate assembly clearance with samples; and fifth freeze the final parameters into the batch production version. At the same time, customers are advised to attach a 2D critical-dimension drawing or annotated screenshots when submitting the model, because a 3D model can express shape but may not express functional priority. For parts that require painting, electroplating, dyeing, polishing, or CNC finishing, allow a machining allowance of 0.05-0.3 mm during the design stage and clearly define which faces are assembly faces, appearance faces, and non-critical faces. For projects with batch delivery plans, first-article reports, material lots, machine numbers, and post-processing records should also be retained to form a traceable quality chain.
5. lantu3D's Role: Delivering Not Only Parts, but a Manageable Manufacturing Process
lantu3D's value lies not only in turning drawings into samples, but also in organizing scattered information across design, manufacturing, post-processing, inspection, and delivery into an executable workflow. For R&D teams, this means concept validation can be completed faster; for procurement and project managers, it means clearer quotation boundaries and more transparent change records; for end users, it means the delivered parts are closer to real application needs. Especially as product iteration accelerates, 3D printing should not be seen as a temporary workaround, but as a standardized module within the R&D and small-batch manufacturing system.
Conclusion
High-quality 3D printing insights and project experience ultimately point to the same principle: the earlier the goals, constraints, and risks are clarified, the more stable the manufacturing process will be. Whether the topic is post-processing, design optimization, defect analysis, or industry trends, truly practical methods depend on data, process, and validation. When choosing a 3D printing service, enterprises should pay attention to whether the provider can offer material recommendations, structural feedback, process records, post-processing plans, and acceptance criteria, rather than comparing only the unit price of a single part. Only then can every prototype become accumulated certainty for the next delivery.
Submit a model, drawing, image or written notes. Engineers will review material, process, finishing and delivery based on actual use.