
Introduction: Why This Issue Is Becoming Critical
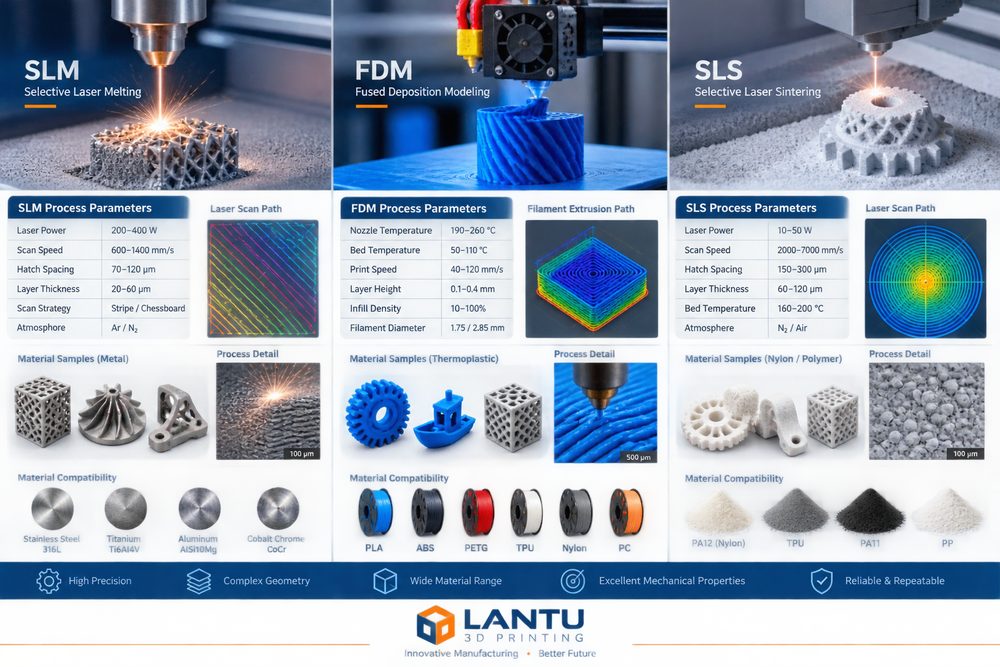
How to tune parameters for SLM, FDM, and SLS: turning 3D printing process optimization into a repeatable production capability is essentially about building the ability of 3D printing to move from "being able to make it" to "being stable, explainable, and deliverable." As customers shift from visual prototypes to functional parts, small-batch production, and rapid spare parts, relying solely on experience-based quoting and ad hoc machine tuning can no longer meet delivery, quality, and cost requirements. lantu3D Printing is positioned as a lifecycle management and implementation platform from blueprint/design to physical delivery, so every step needs to be managed in a structured way.
1. Parameter Windows Determine Batch Stability
For SLM, the focus should be on laser power, scan speed, powder layer thickness, and oxygen content in the protective gas; for FDM, the focus is on nozzle temperature, chamber temperature, layer height, and infill ratio; for SLS, the key variables are preheating temperature, refresh powder ratio, and cooling curve. In real projects, engineers should not look at a single metric in isolation, but should evaluate the part's intended use, load direction, assembly relationship, surface requirements, temperature resistance, and budget on the same decision matrix. For example, precision appearance parts are usually better suited to SLA or high-precision resin, wear-resistant structural parts may use SLS nylon, and parts with high load-bearing and temperature-resistance requirements need evaluation of SLM aluminum alloys, titanium alloys, or stainless steel.
Key parameters should be recorded in a verifiable format: common layer thickness ranges are 0.05-0.2mm, functional part wall thickness is generally not recommended to be below 1.2-2.0mm, and holes, threads, and snap-fit positions need process compensation allowances. Only by feeding these constraints back to the design side in advance can manufacturing avoid repeated rework later.
2. From Problem Analysis to Engineering Decisions
Consolidate first-part parameters, defect photos, dimensional deviations, and reinspection results into a process package to avoid re-testing and rework for every order. Common failures do not necessarily come from the equipment itself, but from misalignment among requirement input, model design, material selection, print orientation, post-processing, and inspection standards. For example, if a customer requests "high strength, good surface finish, low price, and delivery tomorrow," and no priorities are set, rework is likely to occur late in production.
It is recommended to complete three judgments at the project initiation stage: first, whether the part is a display sample, assembly sample, or functional part; second, whether the key indicator is dimension, strength, appearance, temperature resistance, or delivery time; third, who bears the cost of failure and whether first-piece approval is required. The earlier this judgment is completed, the easier it is for the project to proceed as planned.
3. Practical Implementation Methods
Implementation can use a combination of "standard parameter library + project review sheet + exception review." The standard parameter library records recommended settings for different materials, machines, and layer heights; the project review sheet is used to confirm model completeness, minimum wall thickness, support risks, post-processing methods, and inspection standards; the exception review turns issues such as warping, delamination, porosity, dimensional deviation, and surface defects into rules that can be avoided next time.
For small-batch orders, first-piece or small-sample validation should be done before batch production begins. Critical dimensions can be checked with calipers, CMM, or scan comparison; appearance parts should have clear standards for sanding, painting, coloring, or polishing; assembly parts must complete actual fit tests before delivery. This not only reduces customer risk, but also minimizes internal rework.
4. Management Metrics and Continuous Optimization
Companies should focus not on the peak speed of a single machine, but on the overall efficiency from order receipt to delivery. It is recommended to continuously track quotation response time, first-pass review rate, first-piece pass rate, material loss rate, equipment utilization, rework rate, on-time delivery rate, and customer repurchase rate. Each metric corresponds to an optimizable link in the process.
When data accumulates to a certain scale, the platform can further support automated quoting, intelligent scheduling, risk alerts, and knowledge base recommendations. In its services, lantu3D Printing should distill these experiences into reusable workflows so that customers receive not just a part, but a more certain manufacturing path.
Conclusion
Competition in the 3D printing industry is shifting from the number of machines to engineering capability, process capability, and delivery capability. Whether it is materials, processes, applications, equipment, services, quality, cost, customer experience, digitalization, or supply chain, the truly valuable approach is to identify, quantify, and manage uncertainty in advance. For industry practitioners, establishing standards, accumulating data, and continuously reviewing outcomes is the core path to turning 3D printing into stable productivity.
Submit a model, drawing, image or written notes. Engineers will review material, process, finishing and delivery based on actual use.