
Introduction: After a Customer Complaint, the Hardest Part Is Not Explaining It but Determining Accountability
Once a customized 3D-printed part exhibits dimensional deviation, assembly interference, premature surface corrosion, or batch-to-batch property variation at the customer site, the usual response sequence is familiar: sales reassures the customer, engineering reviews photos remotely, quality issues an 8D report, and the parties eventually negotiate a compromise between “reship one part” and “customer performs local grinding.” The problem is that this approach treats the complaint as a service event rather than a quality-loss event. For example, during installation of a batch of 20 PA12 nylon brackets, six parts were found to have hole-position deviations of 0.35–0.55 mm. The company replaced the six parts and covered collect-on-delivery SF Express freight, recording only approximately RMB 4,200 in reproduction costs. However, the customer’s four-hour line stoppage, reinspection of 12 parts, rescheduling, and subsequent order reduction were not included in any ledger. Three months later, the same fixture-location solution failed again. Management still saw only “low after-sales expenses,” so root-cause improvement never became a priority. lantu3D treats the path from blueprint and design to physical delivery as lifecycle management; a complaint closed loop must be captured in four auditable fields: return determination, loss allocation, recall trigger, and defect-escape review.
I. Define the Boundaries First: Returns, Replacements, Rework, Concessions, and Recalls Are Not the Same Thing
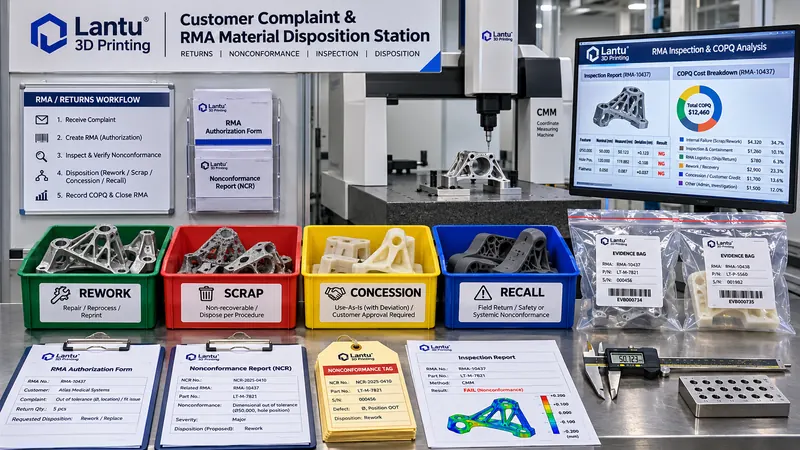
Many disputes arise from inconsistent terminology. Companies should formalize five disposition categories in their quality procedures: return means that both ownership and the physical goods are returned, and is appropriate for functional failure or systematic deviations within a batch; replacement means the original part is returned and a conforming part is reshipped, with the original retained as evidence; rework restores conformity through machining, grinding, or re-heat treatment at the customer site or after return to the factory, and must have re-verification records; concession acceptance means a deviation does not affect function and is accepted for use as-is with written customer authorization—for example, roughness on a non-mating surface may be relaxed from Ra 6.3 μm to 9.0 μm, while assembly-hole dimensions may not be changed; recall/retrieval applies when delivered batches share a common cause and may continue to fail, requiring proactive return or on-site screening by serial number. An RMA (Return Material Authorization) is not merely a shipping document; it is a controlled identifier assigned to each returned item. The customer, order number, batch number, print job number, material heat lot, post-processing batch, failure mode, preliminary classification, shipping method, recipient, and evidence list must all be linked one-to-one. Returned goods without an RMA number should not enter the nonconforming-material area; otherwise, later reviews cannot determine which powder lot or process window produced them.
II. Complaint Classification: Replace Subjective Impressions with Measurable Severity and Spread
Customer complaints should be divided into A, B, and C levels, with numerical criteria rather than descriptive language. Level A covers safety-critical parts, pressure-bearing parts, functional assembly failures, or cases where the same issue affects ≥2 parts in a batch or the batch defect rate is ≥5%. It requires response within two hours and containment of same-batch inventory and in-transit goods within 24 hours. Level B covers appearance defects, noncritical dimensions, or packaging damage that does not affect function, involving one part in a batch with acceptable reinspection results. It requires response within eight hours and a disposition within three working days. Level C covers inquiries, missing documents, and logistics tracking. It does not enter the nonconforming-product process but is included in service metrics. Severity (S), occurrence (O), and detection (D) can each be scored from 1 to 5 to generate a risk priority number, RPN=S×O×D. For example, a mislocated assembly hole in a metal bracket may have S=5, O=3, and D=2, yielding RPN=30 and automatically triggering a Level A classification. Classification must be linked to traceability: RMA to print job number, equipment ID, powder-spreading batch, shielding-gas oxygen record, heat-treatment curve, and CMM report. If 18 parts from the same batch have already been delivered, containment should not cover only the one complained-about part; it should cover all 18 parts under the same job number, plus work in process from adjacent jobs using the same fixture and compensation parameters.
III. The RMA Handling Chain: Seven Steps from Receipt Evidence to Re-Verification
The first step is authorization: the quality engineer issues the RMA, freezes the batch records, and prevents the original model and process parameters from being overwritten. The second step is documenting six-side photos of the received item and the condition of the packaging. Impact-indicator labels, crushed cushioning patterns, and seal integrity should all be retained as evidence to avoid misidentifying shipping damage as a printing defect. The third step is segregation: returned parts are labeled with red nonconformance tags and placed on separate pallets, without mixing them with items awaiting rework or retained samples. The fourth step is repeat inspection: measurements are performed according to the original drawing’s CTQ list. For metal parts, sampling direction must be recorded, as elongation of vertical and horizontal LPBF specimens may differ by 20–40%. Reinspection should preferably use the same calibrated CMM, probe, and fixturing orientation, and measurement uncertainty must be included in the report. The fifth step is root-cause stratification: one primary cause and contributing factors must be identified from seven categories—design-compensation error, model-version error, equipment-state drift, excessive powder moisture content, post-processing deformation, packaging/shipping damage, and customer assembly misuse. “Improper operation” alone is not acceptable. The sixth step is disposition determination: rework, scrap, concession, replacement, or recall must be jointly approved by quality, engineering, and production. Scrapped parts must be destructively marked and entered into the scrap ledger. The seventh step is re-verification and closure: reworked parts receive full-dimensional reinspection; replacement parts include FAI key characteristics and material certificates. Closure requires customer confirmation of use and evidence that CAPA effectiveness has prevented recurrence from the same cause during the following three batches or 90 days.
IV. Calculate Quality Loss Completely: COPQ Allocation and Defect-Escape Metrics
If complaint costs include only reproduction expenses, they will be systematically underestimated. A four-category COPQ (Cost of Poor Quality) structure is recommended: internal failure costs, including scrapped materials, equipment occupation, reprinting labor, rework, and reinspection; external failure costs, including replacement logistics, customer-site support, line-stoppage compensation, price reductions, and lost orders; appraisal costs, including additional CMM inspection, CT, metallography, and third-party reinspection; and prevention and corrective-action costs, including fixture revisions, process-window recalibration, SOP updates, and training. Using the initial batch of 20 brackets as an example: materials and machine time for six replacement parts cost approximately RMB 4,200; SF Express freight and declared-value coverage cost RMB 380; two person-days of engineering field support cost approximately RMB 1,600; CMM reinspection of 12 parts cost approximately RMB 900; the negotiated discount for customer line stoppage was RMB 3,000; and the fixture locating-pin revision and first-article validation cost approximately RMB 2,500. The total is approximately RMB 12,580—three times the original book entry. Define defect escape rate as the number of CTQ-nonconforming parts discovered after delivery divided by the number of parts delivered during the same period, expressed per million parts. If 2,400 parts are delivered in a quarter and six external defects are found, the rate is 25,000 ppm. The target is to reduce it to ≤5,000 ppm after improvements across three batches. Quality monthly reports must display complaint volume, RMA closure cycle time, external failure cost per part, same-cause recurrence rate, and on-time CAPA closure rate side by side; otherwise, even a well-written 8D cannot demonstrate that the system is improving.
V. Recall Triggers and Drills: Do Not Wait Until a Second Customer Calls
Recalls are not exclusive to the automotive and medical industries. Four hard triggers are recommended: two Level A complaints from the same cause associated with the same material heat lot or print job number; CT or metallography confirms batch-level porosity or lack of fusion beyond the acceptance grade; heat-treatment curves, oxygen-content records, or powder-reuse counts are proven to exceed the process window after affected parts have been shipped; or a safety risk occurs at the customer site. Within two hours of a trigger, establish a response team comprising quality, engineering, production, customer service, and legal personnel. Use serial-number lists to distinguish five statuses—installed, at customer inventory, in transit, work in process, and in stock—and issue corresponding on-site screening guidance, stop-use notices, interception instructions, and isolation instructions. Conduct a tabletop drill once per quarter: randomly select a delivered batch and require a contactable serial-number list within 60 minutes, containment of same-batch inventory and in-transit goods within 90 minutes, and an external technical-statement template within 24 hours. The drill output should not be meeting minutes, but executable contact lists, decision thresholds, and communication-script versions.
VI. Implementation Checklist: Upgrade the Complaint Ledger into an Engineering Closed Loop in 30 Days
Week 1: standardize RMA numbering rules and nonconforming-product labels; complete a four-level index linking order number, job number, batch number, and serial number; and incorporate return, replacement, rework, concession, and recall dispositions into procedure documents. Week 2: establish the A/B/C classification table and RPN thresholds; configure response deadlines, escalation paths, and containment-scope rules; and connect the dispatch system to freeze affected batches. Week 3: launch the four COPQ categories and defect-escape-rate reporting; include logistics, discounts, field support, and third-party testing in external failure costs; and require every RMA to include at least three evidence photos and one reinspection report. Week 4: conduct a recall tabletop drill, use customer-complaint data from the previous 12 months to identify the top three high-cost root causes, and assign a CAPA owner and effectiveness criterion to each. Key audit items include: whether returned parts exist without RMA numbers; whether Level A complaints achieve same-batch containment within 24 hours; whether scrapped parts receive destructive marking; whether concession acceptance has written customer authorization; whether CAPA closure includes evidence of no recurrence over the next three batches; and whether COPQ covers lost orders rather than only reproduction costs.
Conclusion: The Deliverables of a Complaint Closed Loop Are a Set of Auditable Numbers
lantu3D emphasizes lifecycle management from design blueprints to physical delivery, and the after-sales stage is equally part of the engineering chain. When customer complaints are upgraded into controlled RMA identifiers, classification criteria, a seven-step handling chain, full-scope COPQ allocation, and recall-trigger mechanisms, the company gains more than a carefully worded 8D report. It gains traceable answers to: which batch, which machine, which parameter, how much loss, and whether recurrence occurred. Review four metrics quarterly: 100% same-batch containment achievement for Level A complaints, average RMA closure time of ≤7 working days, same-cause recurrence rate of ≤5%, and a continuously declining defect-escape rate per million parts. Only when return and recall data can feed back into fixture design, process windows, and inspection plans do customer complaints truly shift from a cost center to an entry point for engineering improvement.
Submit a model, drawing, image or written notes. Engineers will review material, process, finishing and delivery based on actual use.