
Introduction: Electricity, Gas, and Carbon Are Accounted For—Why Is Water Still Hidden in the Main Meter?
Over the past two years, lantu3D has progressively refined its workshop energy accounting: peak/off-peak tariffs and demand are reconciled with electricity bills; oxygen content in inert gas and gas consumption per part are reported in m³/part; and carbon footprint is reported in kgCO₂e per qualified delivered part. Yet one utility has almost never been separately accounted for: cooling water. Lasers, galvanometers, build-chamber jackets, vacuum pumps, air compressors, dehumidifiers, and post-processing annealing furnaces in metal LPBF systems all rely on circulating water to remove heat. A single machine commonly has a cooling-loop flow rate of 8–15 L/min, a supply-return temperature difference of 3–6 °C, and a required supply-water temperature of 20 ± 2 °C. Most factories have only one building-level water meter, with make-up water mixed with fire-protection and domestic use; cooling-tower blowdown valves are opened based on experience; and heat-transfer efficiency gradually declines as heat-transfer surfaces scale up. Only when laser output fluctuates, chamber-temperature alarms occur, or vacuum-pump exhaust temperature rises do operators reactively shut down the machine.
These issues share a common cause: it is not that water is unavailable, but that water has not been converted into verifiable engineering data. This article does not offer water-saving slogans. It provides an accounting method that can be implemented through submeter readings, heat-balance equations, cycles-of-concentration criteria, per-part water-use metrics, and release records—bringing water into the same energy ledger as electricity, gas, and carbon.
1. Define the Boundary First: Four Heat Loads and Three Water Circuits
The first step in accounting is not installing meters, but clearly defining the system boundary. Workshop cooling water typically serves four categories of load: optical and laser loads (lasers, galvanometers, and protective-lens mounts, which are most sensitive to water temperature and quality); build-chamber loads (build-cylinder jackets, build-plate preheating circuits, and atmosphere-circulation heat exchange); auxiliary power loads (vacuum pumps, air-compressor aftercoolers, and chiller condensers); and post-processing loads (annealing furnaces and temperature-controlled cleaning tanks). Their thermal-load profiles do not overlap: laser loads vary with scanning duty cycle, build chambers plateau during preheating and recoating, auxiliary equipment runs almost continuously, and post-processing is intermittent by furnace cycle. If they are combined in a single main line, no ΔT reading can be attributed to a specific source.
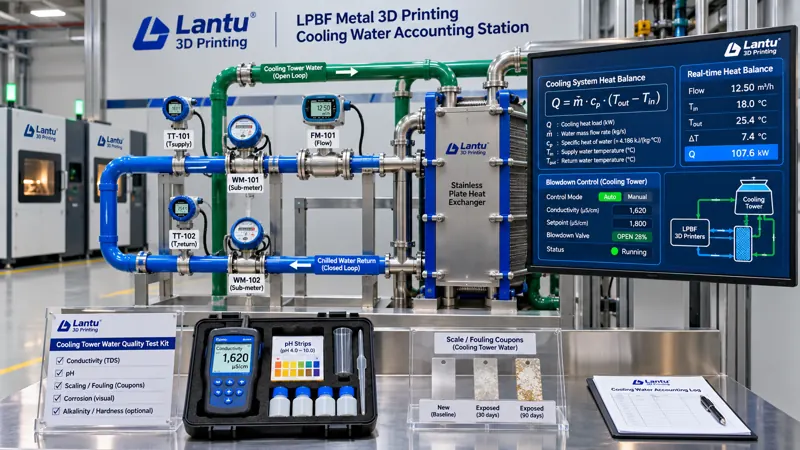
The water system should be separated into three independently metered circuits: the primary side (heat-rejection circuit for cooling towers or outdoor units), the secondary side (equipment-side closed loop, usually deionized water or glycol solution), and make-up water and blowdown (municipal-water make-up, concentration-control blowdown, and overflow losses). Water volume in the secondary closed loop is essentially constant; actual consumption occurs through primary-side evaporation and blowdown, plus make-up water. Therefore, the numerator for “per-part water use” can only be make-up water volume, not circulating-pump flow. Once the boundary is documented in a Water System and Metering Point Diagram and every measurement point is numbered (W-01 make-up meter, W-02 blowdown meter, T-01/T-02 secondary-side supply and return temperatures, F-01 secondary-side flow), all later disputes can be traced back to the same diagram.
2. Submetering and Heat Balance: From Readings to Reproducible Q
Heat removed on the secondary side is calculated as Q = c·m·ΔT, where the specific heat of water c is 4.18 kJ/(kg·°C) and mass flow m is converted from F-01. For example, for a 500 W-class LPBF machine with a secondary-side flow of 12 L/min (0.2 kg/s) and a supply-return temperature difference of 4.5 °C, Q ≈ 4.18 × 0.2 × 4.5 ≈ 3.76 kW. This should align with the combined heat load from laser electrical power and electro-optical conversion losses, galvanometers, and chamber heat dissipation. If deviation exceeds ±20%, suspect flowmeter drift or unpaired temperature-sensor calibration first. The critical discipline is paired temperature measurement: installing only an outlet thermometer and treating the setpoint as inlet temperature makes ΔT a fixed value and renders the heat balance meaningless.
On the primary side, use make-up water W_make-up, blowdown W_blowdown, and evaporation W_evap for water balance: W_make-up = W_evap + W_blowdown + W_drift (drift and leakage). Of these, only make-up and blowdown can be read directly from meters. Evaporation can be back-calculated from heat balance as W_evap ≈ Q_total / (r + c·Δt), where r is latent heat of vaporization at approximately 2400 kJ/kg and Δt is the cooling-tower temperature difference. This closes the balance even without an evaporation meter. A persistent closure error >8% signals leakage or meter inaccuracy—not simply that “hot weather required a little more make-up water.”
3. Cycles of Concentration and Blowdown: Recirculating Water Cannot Be Make-Up Only
An open cooling tower evaporates pure water while salts remain in the system. The cycles of concentration N = make-up-water ionic concentration / circulating-water ionic concentration, commonly approximated on site by the conductivity ratio. If N is too low, excessive blowdown wastes water and treatment chemicals; if N is too high, calcium carbonate precipitates, heat-transfer surfaces scale, and corrosion rates increase. An engineering control window of N = 3–5 is common, corresponding to blowdown of approximately 1/(N−1) of evaporation; at N=4, W_blowdown ≈ W_evap/3. Criteria must be written in assessable terms rather than as “good water quality”: circulating-water conductivity ≤1500 μS/cm, total hardness as CaCO₃ ≤200 mg/L, pH 7.5–9.0, and turbidity ≤10 NTU. Sample weekly and record chemical-treatment batch numbers and dosage. Conductivity above the limit on two consecutive measurements requires mandatory blowdown and retesting. Do not simply increase make-up water for dilution—that only conceals N and does not reduce total salt mass.
The secondary closed loop requires a separate set of criteria: deionized-water conductivity should be ≤50 μS/cm; glycol concentration should be calculated according to freeze-protection requirements and reviewed quarterly; and pH and corrosion-inhibitor concentration should follow the manufacturer’s water-quality specification. Optical-load loops should be fitted with 5–20 μm filters and differential-pressure gauges. Replace the filter element when differential pressure exceeds 1.5 times its initial value. Protective lenses and laser flow channels are highly particle-sensitive, and the cost of a failed filter element far exceeds the cost of the filter itself.
4. Scaling and Heat-Transfer Degradation: Converting Approach Temperature into a COP Criterion
The greatest danger of scaling is that it does not trigger an alarm. As thermal resistance on heat-transfer surfaces gradually increases, secondary-side ΔT decreases and equipment inlet-water temperature rises. The control system automatically increases cooling-tower fan or chiller-compressor load to maintain the setpoint, so water temperature may appear normal while electricity consumption quietly rises. Therefore, criteria cannot focus only on temperature; they must monitor approach temperature and energy efficiency: the approach between primary-side outlet water and secondary-side inlet water at a plate heat exchanger should be ≤2 °C. For chiller COP (cooling capacity/compressor input power), use the comparable operating-condition value from the first month of operation as the baseline. A decline >15% triggers chemical cleaning and retesting; a decline >25% requires shutdown inspection and assessment of heat-exchanger core replacement.
Water-system events must also be linked to build quality: every supply-water temperature excursion and every heat-transfer-efficiency anomaly must record the corresponding build layer number, chamber position, and scan-job ID at the time of occurrence. Review the oxygen content, melt-pool monitoring, and witness-coupon results for parts in that chamber. This follows the same logic as tying millisecond-scale voltage sags to build layer numbers in power-quality control—a utility disturbance can support a release decision only when it is tied to specific parts. A three-tier disposition is recommended: Grade A (water temperature, flow, and quality all within limits), normal release; Grade B (temporary excursion ≤5 min and passing witness coupon from the same chamber), release after review with deviation recorded; Grade C (excursion >5 min, COP decline >25%, or unaddressed conductivity exceedance), isolate parts from that chamber and handle them according to inspection-lot retest rules.
5. Per-Part Water Use: Qualified Delivered-Part Basis and Shared-Build Allocation
The accounting basis should align with gas consumption and carbon footprint: per-part water use = (make-up water during the accounting period − non-production water use) ÷ number of qualified delivered parts during the accounting period. Non-production water use—domestic use, fire protection, floor cleaning, and landscaping—must be separately metered and deducted from the numerator. Otherwise, monthly changes in headcount will contaminate the metric. The denominator is the number of parts that pass inspection, complete specified post-processing and packaging, and are delivered to the factory gate—not the number of printed parts. Water used for scrap and rework should be amplified through yield and assigned to qualified parts. This is precisely why the metric provides greater decision-making value than “total water bill/total part count.”
For shared builds, allocation should use a thermal-load proxy rather than simple equal allocation by part count. Use each part’s “scan time × number of layers × support-and-build-plate volume correction factor” to form an allocation weight w. Allocate the common pool—preheating, atmosphere purging, build-plate cooling, witness-coupon cooling, and standby baseline water use—by w. Directly attributable use, such as water used in a dedicated post-processing cleaning tank for one part, should be assigned directly to that part. The weighting formula must be frozen before the accounting period begins and recorded under a version number in the Water-Use Allocation Rules. Selecting weights after seeing results is prohibited—freeze the rules first, then discuss factors. This is a shared baseline principle for energy and carbon accounting. Report three figures simultaneously: average water use per part, P50/P95 by part family, and the shares of water use, electricity cost, and gas consumption in unit-part energy cost. This avoids local optimization such as “saving 3 m³ of water while consuming 400 additional kWh of electricity.”
6. Evidence Chain and Implementation: ALCOA+ and an Eight-Item Checklist
All readings must be reproducible by a third party, so records should be organized under ALCOA+: attributable (measurement-point ID, meter ID, and calibration validity), legible (original readings rather than manually transcribed summaries), contemporaneous (using the same time source as build timestamps, with no retrospective entries), original (retain raw meter-pulse records and temperature-curve files), and accurate (enter corrected values in a compensation table with two-person review), plus complete, consistent, enduring, and available. Each record must include at least: timestamp; cumulative W-01/W-02 readings; instantaneous T-01/T-02 values; F-01 flow; conductivity and pH; corresponding build ID and layer number; disposition grade; operator; and reviewer. Calibrate meters annually, calibrate temperature sensors as pairs, compare flowmeters with portable ultrasonic instruments, and enter calibration certificate numbers into the ledger.
A 30-day implementation can be completed in five steps: in Week 1, draw the metering-point diagram and install W-01/W-02 and paired temperature sensors; in Week 2, run water-balance closure analysis and establish the cycles-of-concentration window; in Week 3, establish the COP baseline and three-tier release criteria; in Week 4, freeze allocation rules and trial-calculate per-part water use for three part families; and in Week 5, add water use to the monthly energy ledger and review it alongside electricity cost, gas consumption, and carbon intensity. Finally, conduct a self-audit using the eight-item checklist: complete metering-point diagram and measurement IDs / separately metered make-up water and blowdown / paired temperature calibration / water-balance closure error ≤8% / conductivity and hardness thresholds with weekly records / approach-temperature and COP baselines with trigger actions / excursion events tied to build layer numbers with three-state disposition / version-controlled allocation rules with qualified delivered parts as the denominator.
Conclusion
Cooling water is not “just a pipe attached to the equipment”; it is a fourth accountable utility alongside electricity, gas, and carbon. Managing it does not begin with installing a larger chiller, but with four specific elements: a numbered water-system and metering-point diagram, a water-balance equation that closes, numerical criteria for water quality and heat-transfer degradation, and a per-part water-use metric based on qualified delivered parts and linked to builds. With these four elements in place, abnormal water temperature no longer has to be discovered only after a shutdown, and water conservation no longer depends on slogans. It becomes engineering data that can enter quotation and costing sheets and be reviewed by customers and third parties. For a platform such as lantu3D that manages the process from blueprint/design through physical delivery, the verifiability of utility data is itself part of delivery capability.
Submit a model, drawing, image or written notes. Engineers will review material, process, finishing and delivery based on actual use.