
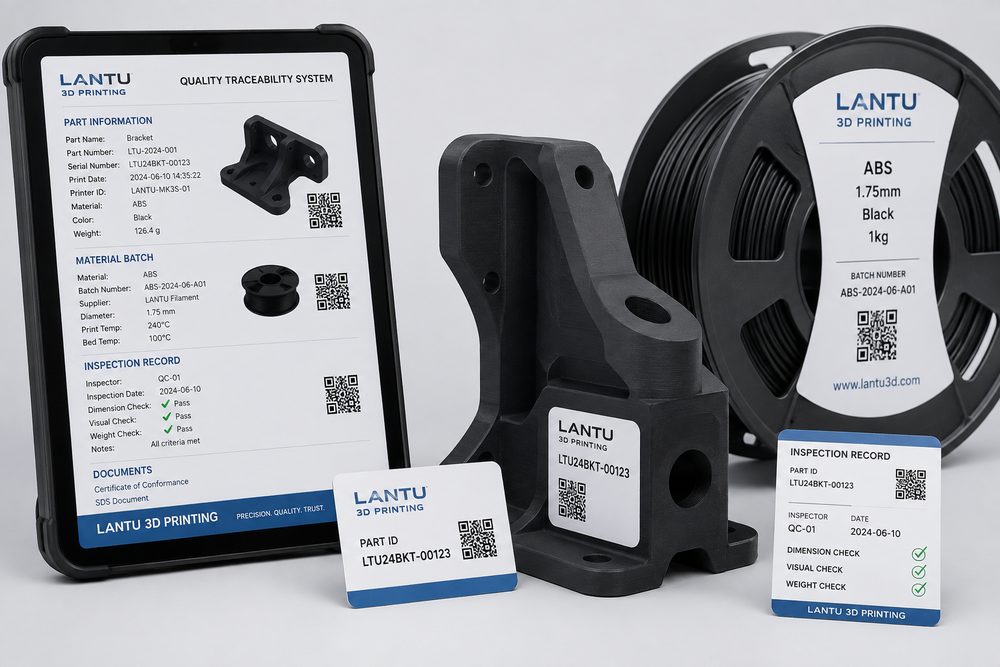
Introduction: Without traceability, quality issues are only guesses
3D printing service orders often involve multiple product types, small batches, and rapid iterations. A customer may update the model within a day, an engineer may adjust supports based on print orientation, and a post-processing operator may refine visible surfaces. If traceability records are missing, once there is poor assembly, color variation, or dimensional out-of-tolerance issues, it becomes very difficult to determine whether the problem came from the file version, material batch, machine status, or manual post-processing.
Quality traceability is not only necessary for large factories. For a 3D printing service platform, a lightweight but continuous traceability chain can significantly reduce communication costs, help customers understand the manufacturing process, and help internal teams accumulate reusable quality knowledge. lantu3D is positioned as a bridge between digital design and physical delivery, so traceability should cover the entire path from file receipt to shipment confirmation.
1. File version traceability: make sure the correct model is printed first
The file version is the starting point of the traceability chain. Each order should record the original file name, receipt time, customer-confirmed version, engineering modification history, and final print version. If an engineer performs repairs such as surface fixing, thickening, part splitting, adding powder-removal holes, or adjusting assembly clearances, a new version must be created and the changes documented. Do not use vague names such as “final,” “new,” or “rev2” as the only reference.
It is recommended to use an order number + part number + version number naming convention, for example B3D-260904-A03-V02. The version confirmed by the customer should be locked, and any later changes must be reconfirmed. For multiple similar parts, thumbnails, key dimension screenshots, and file hash values can also help avoid confusion. Only when the file version is clear can later quality judgments have a solid basis.
2. Process parameter traceability: record the key variables that affect the result
Different 3D printing processes require different parameters to be recorded. SLA should record the material model, layer thickness, build orientation, support strategy, exposure or machine settings, and cleaning and curing time; SLS should record material batch, powder refresh ratio, layer thickness, build chamber position, cooling time, and depowdering method; metal SLM should record powder batch, layer thickness, laser strategy, heat treatment, cutting method, and machining datum.
Not all parameters need to be entered manually in long form. Equipment job sheets, slicing screenshots, and material batch labels can be archived as attachments. The key is that when a problem occurs, it should be possible to look back and see whether the parts came from the same material batch, were located at the edge of the build chamber, underwent the same post-processing flow, or used the same inspection standard.
3. Process anomaly traceability: turn failure records into risk warnings
Many teams only record successful deliveries and overlook failure processes. In fact, print failures, support breakage, powder-removal difficulty, warpage, surface contamination, and rework次数 are all highly valuable traceability information. Recording anomalies is not for assigning blame, but for determining whether a risk is repetitive.
It is recommended to classify anomalies into design risk, process risk, equipment risk, material risk, and post-processing risk. Each anomaly record should at least include the discovery time, part number, phenomenon description, temporary handling, root cause judgment, and preventive measures. For example, if a nylon buckle part repeatedly turns locally white after depowdering, this may indicate insufficient wall thickness, fillet size, or assembly deformation clearance; if a resin part warps after secondary curing, the build orientation and curing fixture should be checked again.
4. Inspection record traceability: let acceptance judgments have evidence
Pre-shipment inspection should focus on the indicators the customer truly cares about, rather than formal stamping. Common inspection items include critical dimensions, assembly fit, appearance surfaces, quantity, color, post-processing grade, and packaging status. For functional parts, load, insertion/removal, sealing, or temperature resistance tests can be added; for display parts, color difference, paint adhesion, and surface defect checks can be added.
Inspection records should include the design value, measured value, acceptance criteria, and inspector. Dimensional records can be supported by caliper photos, CMM reports, or scan comparison images; appearance records can be archived with photos taken under standard lighting. If the customer later reports a problem, inspection records can help both sides quickly determine whether the issue already existed before shipment or was caused during transportation, assembly, or use.
5. Packaging and shipment traceability: quality delivery does not only happen in the workshop
The packaging method for 3D printed parts directly affects delivery quality. Long and thin parts, thin-wall parts, and painted parts are easily compressed, rubbed, or deformed during transport. Shipment traceability should record packaging materials, separation method, labels, quantity list, logistics tracking number, and shipping photos. For high-value or fragile parts, single-piece isolation, foam positioning, outer-box reinforcement, and orientation marks are recommended.
If the customer receives missing, mixed, or damaged parts, complete packaging records can quickly identify which link caused the problem. For orders delivered in batches, the list should also indicate the batch number, shipped quantity, remaining quantity, and corresponding file version to avoid version mixing during on-site assembly.
6. Data review: the traceability system must ultimately support improvement
The value of quality traceability is not only in post-event lookup, but also in continuous improvement. By analyzing anomaly types, rework rates, material issues, post-processing time, and customer complaint causes, the most critical areas for optimization can be identified. For example, if the rework rate of a certain thin-wall housing has long exceeded 8%, wall-thickness reminders should be added during the design review stage; if color-difference complaints for dyed parts are concentrated, batch dyeing and sample confirmation procedures should be adjusted.
Lightweight traceability can start with spreadsheets, QR code labels, and shared job sheets, then gradually transition to systematic management. The key is not how complex the tool is, but whether each step is willing to leave verifiable records.
Conclusion: Quality traceability is the trust foundation of service manufacturing
In 3D printing services, quality traceability connects files, materials, equipment, processes, inspection, packaging, and customer feedback. It makes issue localization faster, responsibility boundaries clearer, and the next delivery more reliable. For enterprise customers, only a service platform with traceability capabilities can truly support long-term cooperation from R&D prototypes to small-batch delivery.
Submit a model, drawing, image or written notes. Engineers will review material, process, finishing and delivery based on actual use.