
Introduction: One Build, Two Systems, Two Curves
During a delivery review for a metal LPBF part, the customer requested layer-by-layer curves for build-chamber oxygen concentration and laser power. The curve exported from the MES contained 4,217 points, while the machine’s local log contained 4,239 points, with power values differing by 6% at the same layer number. The engineering team spent two days confirming that the machine was not at fault: when the edge gateway backfilled data after an 11-minute overnight disconnection, it mixed the “device timestamp” and “database ingestion timestamp” into one field and lost the sequence numbers of 22 points. The part itself passed inspection, but the data link was not trustworthy, so the report could not be issued. lantu3D classifies such issues within lifecycle management from digital blueprint to physical delivery: the data link is not an ancillary machine function, but a controlled object on the same level as the model, parameter package, and powder lot number. This article provides an implementable controlled-acquisition specification: a point semantic dictionary, four timestamps, quality flags, an offline persistent queue, four backfill verification checks, and A/B/C link-release states.
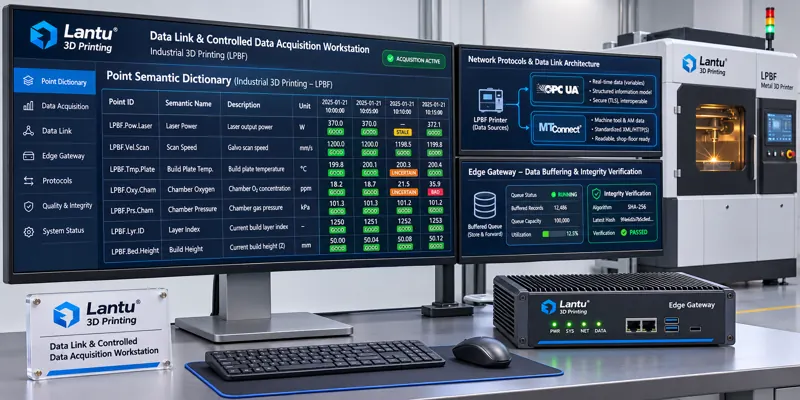
1. Point Semantic Dictionary: Define What a “Point” Means First
Most shop-floor acquisition tables contain only three columns: variable name, value, and time. This is insufficient for decision-making. An 11-field semantic dictionary should be established for every data point: ① unique equipment ID, including model and factory serial number; ② point code, such as LPBF-03.CHAMBER.O2_PPM; ③ physical quantity name and engineering unit, such as ppm, W, mm/s, and °C; ④ data-source type, such as PLC register, machine API, or external sensor; ⑤ sampling interval and trigger method, such as periodic 1 Hz / 10 Hz sampling or layer-event triggering; ⑥ range and resolution, such as 0–2,000 ppm and 0.1 ppm; ⑦ filtering and aggregation rules, such as retaining raw values unfiltered and storing a 1-minute average as a separate derived point; ⑧ accuracy or uncertainty source; ⑨ applicable process stage, such as preheating, building, cooling, or post-processing; ⑩ associated primary key, consisting of work order number + build number + layer number; and ⑪ version number and effective date.
The dictionary must be version-controlled: adding points, changing ranges, or changing sampling rates must go through a change order, while historical points must continue to be interpreted under their original definitions. Without a semantic dictionary, cross-machine comparison and allocation across a shared build are impossible—two machines may both have a point called “Power,” but one may represent the setpoint and the other the measured feedback value. Directly merging them will inevitably lead to incorrect conclusions.
2. Four Timestamps and Clock Reference: Make Every Point Locatable and Replayable
Each record should carry four timestamps: T_dev (time generated by the device), T_gw (time received by the gateway), T_store (time written to the database), and T_backfill (time backfill was completed; null during normal online operation). Each serves a distinct purpose: T_dev is used for process reconstruction and layer alignment; the difference between T_gw and T_dev reflects link latency; T_store supports database auditing; and T_backfill identifies records that have undergone outage recovery.
The clock reference must also be specified: equipment and gateways should use synchronized PTP/NTP, with a target deviation of ≤10 ms and drift recorded daily. For sampling above 10 Hz or simultaneous multi-layer events, timestamp resolution, in ms or μs, must be specified in the point dictionary. A common misjudgment is to use T_store rather than T_dev when plotting curves: points within a backfill window become compressed into the same time, creating false power steps. The engineering rule is to mark a point as STALE when |T_gw − T_dev| exceeds three times the sampling interval; if the delay exceeds 30 s for 10 consecutive points from the same machine, a link alarm is triggered.
3. Quality Flags: GOOD / STALE / UNCERTAIN / BAD
A numerical value does not inherently convey trustworthiness; it must carry a quality flag. GOOD means the point arrives within the cycle window, is within range, has a continuous sequence number, and meets clock-deviation requirements. STALE means it arrives late or carries forward the previous value; it may be displayed on dashboards but must not enter release calculations. UNCERTAIN means the value is near the measurement-range limit, sensor calibration has expired, the backfill digest has not been verified, or conflicting values occur at the same layer number. BAD means out of range, non-numeric, sequence discontinuity, or hash mismatch. Only GOOD points may be included in conformity denominators and statistical calculations for per-part energy consumption, gas consumption, and layer power; UNCERTAIN points must be manually reviewed and converted to GOOD or BAD. The system must not automatically downgrade release requirements.
The four states should be stored with the record rather than calculated afterward, because backfill, replay, and cross-system export can alter context. Quality flags must be stored together with the point-dictionary version number so that the original decision criteria can be reproduced during historical recalculation.
4. Offline Persistent Queue: Size Capacity for the Worst-Case Window, Not Average Bandwidth
Edge-gateway disconnections are normal operating conditions rather than exceptions. Gateways require a local persistent queue using a composite primary key (equipment ID + point code + T_dev + layer number), with every record carrying a sequence number and SHA-256 digest. Capacity should be calculated as “maximum tolerable outage × peak point frequency × record size.” For example, for 12 machines with 40 points each, sampled at an average of 1 Hz and approximately 200 B per record, eight hours requires about 69 MB. Considering 10 Hz points, retransmission copies, and indexing overhead, reserve ≥256 MB and no less than 24 hours of capacity, with an 80% utilization alarm and a pre-overflow degradation strategy: retain critical CTQ points first and suspend derived points.
The queue must use write-ahead logging (WAL) and power-loss protection. After recovery, it must not be cleared directly; records may be deleted by transaction only after all four backfill checks have passed. “Overwrite immediately upon reconnection” is prohibited—that was precisely the root cause of the 22 lost points described in the introduction.
5. Four Transactional Backfill Checks: Sequence Number, Count, Digest, and Primary-Key Conflict
Backfill should treat “equipment + outage interval” as one transaction and perform four checks in sequence: ① sequence continuity: no skipped or duplicate sequence numbers within the interval; ② count consistency: the difference between the gateway queue count and the machine-local export count must be ≤0.1%; if exceeded, the entire interval is converted to UNCERTAIN for manual comparison; ③ digest match: concatenate records in sequence, calculate SHA-256, and compare it with the interval digest from the equipment side; ④ primary-key conflict: before database ingestion, check the composite primary key. Conflicting records must not be silently overwritten; they must be written to an isolation table for disposition.
Only when all four checks pass may the transaction be committed, T_backfill written, and the quality flag changed from “pending backfill” to GOOD; if any check fails, the entire interval returns to the queue, and partial commit is prohibited. A 30-minute trace-back drill is recommended every month: randomly select one build and require the same curve to be reconstructed from the machine log, gateway queue, and database within 30 minutes. The link is considered controlled only if the consistency rate is ≥95%.
6. A/B/C Three-State Link Release: Can the Data Be Used for Certification?
Link status should be directly tied to engineering release. State A (issuable)—the CTQ point-dictionary version is valid, all four timestamps are complete, GOOD rate is ≥99.5%, there are no open backfill events, and clock drift is compliant; witness coupons and inspection reports may be linked to the build’s process curves. State B (conditionally usable)—non-CTQ points contain STALE values or completed backfill events, with a GOOD rate of 98%–99.5%; the data may be used for internal process analysis but not as customer delivery evidence or as the basis for concession release. State C (frozen)—critical CTQ points contain BAD values, a digest mismatch exists, an unclosed outage exceeds 24 h, or the dictionary version is inconsistent with that used during production; process data for that build must not be issued and must proceed through a deviation report and data review.
The three states require dashboards and assigned owners. Five indicators should be reviewed weekly: link health, measured by GOOD rate; backfill closure time; clock drift; point-dictionary version consistency; and trace-back drill pass rate. In this way, “data trustworthiness” is no longer a verbal assurance, but an engineering criterion that can be determined, traced, and reproduced.
7. Implementation Checklist and Common Misjudgments
Implementation follows six steps: inventory points and freeze Dictionary V1.0 → standardize clocks and timestamp fields → configure gateway queue capacity and utilization alarms → implement four backfill checks and an isolation table → store quality flags in the database → incorporate A/B/C release rules into inspection procedures. Three common misjudgments are: treating “data was collected” as “data can be issued,” despite missing quality flags and release status; treating “average values” as “raw evidence,” although derived points cannot replace raw points; and treating “backfill succeeded” as “data is complete,” without count and digest verification.
Boundary conditions must also be understood: point dictionaries and quality flags do not replace equipment metrology calibration, which belongs to geometric accuracy and measurement traceability; nor do they replace account permissions and audit logs, which belong to the access-control layer. Only the combination of all three forms a complete evidence chain from design blueprint and process parameters to physical delivery.
Conclusion
The value of an equipment data link lies not in how many points are connected, but in whether every point can be defined, located, assessed, and reproduced. An 11-field dictionary eliminates semantic ambiguity; four timestamps eliminate timing misalignment; four-state quality flags distinguish trustworthiness; persistent queues and four transactional backfill checks eliminate data loss during outages; and A/B/C states translate link status into an engineering conclusion on whether a report can be issued. For additive manufacturing, where small batches, high mix, and stringent traceability are standard, this method turns process data into a genuinely deliverable asset rather than a collection of logs that cannot substantiate themselves after the fact.
Invia un modello, un disegno, un'immagine o note scritte. Gli ingegneri valuteranno materiale, processo, finitura e consegna in base all'uso effettivo.