
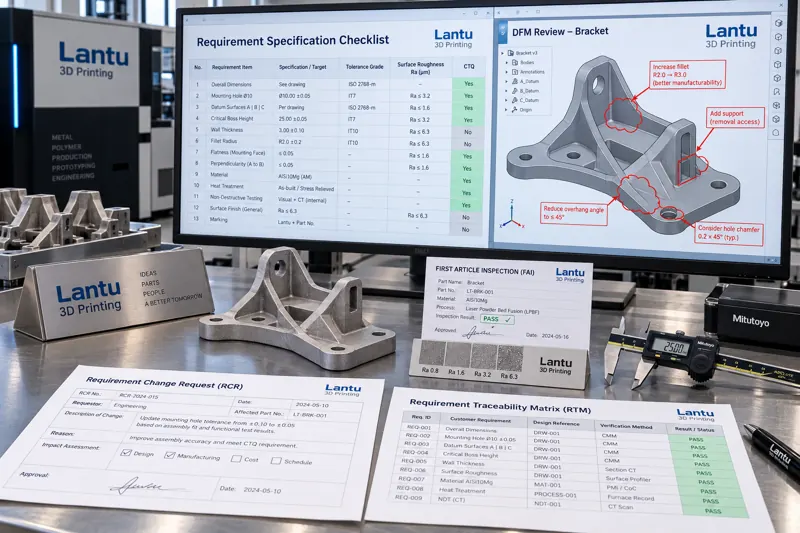
Why Requirements Must First Become Verifiable Specifications
In additive manufacturing projects, the most common rework does not occur during printing, but during requirements interpretation. Customer requests such as “slightly higher strength,” “a smoother surface,” or “better dimensional accuracy” are not directly executable engineering instructions. Without a material grade, heat-treatment condition, and specimen orientation, there can be no acceptance criteria. lantu3D defines requirements engineering as the first checkpoint in lifecycle management from drawing to physical part: translating vague descriptions into numbered requirements with thresholds and verification methods, so that quotation, production scheduling, and inspection share a common language.
A usable requirements specification typically includes four categories of information: geometry and tolerances (critical dimensions, GD&T, and datum systems); material and condition (grade, powder-batch requirements, heat treatment, and densification requirements); surface and performance (roughness grades and locations and orientations for mechanical-property specimens); and delivery and traceability (batch identification, required inspection reports, and packaging methods). If any category is missing, it will eventually need to be added through a change order.
CTQ Identification: Reducing Dozens of Dimensions to a Few Critical Items
A printed part may contain hundreds of specified dimensions, yet only 5 to 12 typically determine assembly and function. These are CTQs, or critical-to-quality characteristics. They should be identified by working backward from the functional chain: dimensions affecting assembly fits, surfaces affecting sealing or load bearing, and radii and surface conditions affecting fatigue life should all be classified as CTQs. Non-mating dimensions that serve only the overall form can be treated as general items.
Once items are graded, inspection resources can be allocated appropriately. CTQ items should be inspected 100% and supported by retained measured data; important items may be sampled by lot; and general items require only visual and shipping-damage inspection. For metal LPBF parts, specimen orientation must also be specified separately. The difference in elongation between vertical and horizontal orientations can reach 20% to 40%; a performance requirement that does not specify specimen orientation is inherently invalid.
Sample Approval and First Articles: Turning “Looks Right” into “Measures Right”
Sample approval before a production order is the most effective way to converge requirements. The sample stage should not merely confirm appearance; it should lock down three factors: whether the material-and-process parameter combination meets performance requirements, whether print deformation remains within the compensation range, and whether the post-processing route can consistently reproduce the required surface condition.
First article inspection (FAI) should cover all CTQ items and include material certificates, heat-treatment curves, and inspection reports. The first-article sample must be retained as a sealed reference for comparison with subsequent lots. A sealed sample signed off by the customer is the only physical evidence for determining whether a change has occurred later. Without a retained sealed sample, any dimensional dispute will revert to the parties’ respective recollections.
Requirements Changes: Ensuring Every Modification Has a Cost and a Trace
Because printing projects have short lead times, customers often request adjustments after sample evaluation. Changes themselves are not the problem; the problem is changes without identifiers, impact analysis, or version control. A standardized change process should include a change request recording the revised content and original identifier; an impact analysis covering effects on tooling, parameters, inspection items, and delivery time; revision control to ensure obsolete drawings are immediately withdrawn; and, when necessary, renewed first-article validation.
Two types of changes must be distinguished in particular: geometric changes generally require renewed simulation and first-article validation, whereas document-only clarifications, such as adding a surface-roughness notation, require only an update to the technical documentation. Confusing the two can lead either to excessive validation or missed validation.
Technical Agreements: Defining Acceptance Rules Before Delivery
A technical agreement is the final output of requirements engineering and the basis for judgment during delivery. At minimum, an executable technical agreement should define the referenced standard numbers and revisions; acceptance criteria and measurement methods for critical characteristics; sampling plans and acceptance numbers; disposition of nonconforming products, including rework, concession, or rejection; and retained-sample and retest procedures for dispute resolution.
A performance requirement without acceptance criteria is equivalent to no requirement at all. For example, “smooth surface” should be written as: “Ra ≤ 6.3 μm on specified surfaces, evaluated in accordance with GB/T requirements, with a sampling length of 0.8 mm and the average of three measurements.” Likewise, “acceptable strength” should be written as: “Room-temperature tensile strength of furnace companion specimens ≥ the specified value; specimen orientation shall be vertical; specimens shall undergo heat treatment with the production lot.”
Conclusion
Translating customer requirements into verifiable specifications is the highest-return step in the delivery chain from drawing to physical part. Identifying CTQs, establishing benchmarks through samples and first articles, controlling modifications through change orders and revision control, and defining acceptance rules through technical agreements can collectively prevent rework before quotation and provide an evidence-based foundation for resolving delivery disputes.
Invia un modello, un disegno, un'immagine o note scritte. Gli ingegneri valuteranno materiale, processo, finitura e consegna in base all'uso effettivo.