
Introduction: A Material Certificate Cannot Answer “What Is in the Delivered Part?”
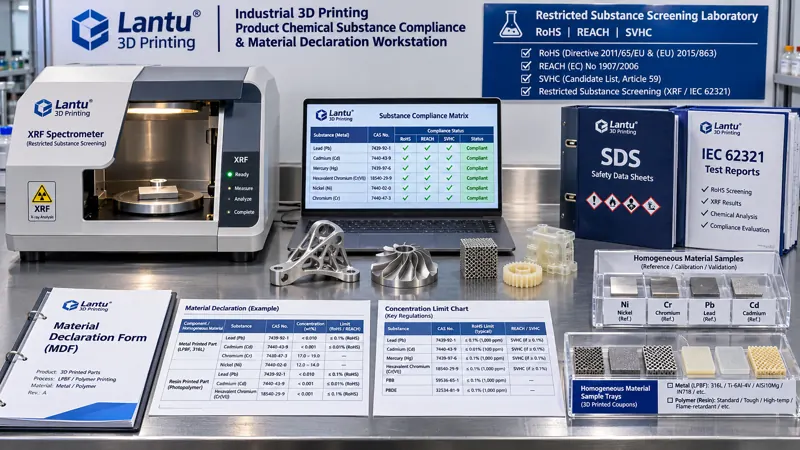
3D printing service providers frequently encounter customer questions such as: Can you provide a RoHS declaration of conformity for this shipment of nylon, metal, or resin parts? Do REACH Substances of Very High Concern (SVHCs) exceed 0.1%? For packaging and coatings exported to the EU, what are the concentrations of hexavalent chromium, cadmium, lead, and phthalates? Many teams simply forward the material supplier's certificate of analysis or SDS, only to have it deemed insufficient evidence. The issue is not necessarily that the material is non-compliant; rather, a certificate demonstrates the batch properties of a drum of powder or a spool of filament, but cannot demonstrate that, in a finished part that has undergone powder spreading, sintering, cleaning, blasting, electroplating, bonding, and packaging, the substance composition and concentration of every homogeneous material still comply with applicable limits. lantu3D regards the journey from design drawing to physical delivery as a lifecycle chain. Substance compliance is not merely an attachment held by procurement, but engineering data that must be transferred along the chain, verifiable, and version-controlled.
1. Break Down “Homogeneous Materials” into Assessable Boundaries
The assessment unit under RoHS and REACH is neither the complete assembly nor an individual part, but a homogeneous material: a material unit that cannot be further mechanically disassembled and has uniform composition throughout. For example, a metal bracket produced by LPBF and surface-treated should at minimum be broken down into: the base metal (such as as-printed 316L or Ti6Al4V), surface plating or conversion coating, insert-nut alloy, adhesive at bonding interfaces, marking ink, cushioning packaging foam, and barrier bags. Resin parts must also be divided into the photopolymer resin itself, cleaning residues, color coatings, and post-curing layers. The principle is to create a mapping table from the material BOM to the homogeneous-material list. Each row should state the material name, supplier, grade, lot number, mass proportion, location, whether it can be mechanically separated, and referenced declaration number. If a plating layer is only a few micrometers thick and cannot be mechanically separated, it must still be declared as an independent homogeneous material rather than averaged into the substrate. Concentration limits are calculated based on the mass of the homogeneous material; averaging systematically underestimates risk.
2. Limits and Exemptions: Translate Regulatory Text into Fillable Fields
Common restricted-substance requirements must be converted into individual data fields rather than broad claims. RoHS generally assesses lead, mercury, hexavalent chromium, polybrominated biphenyls, polybrominated diphenyl ethers, and cadmium against homogeneous-material mass-fraction limits of 0.1% and 0.01%; phthalates have separate thresholds in specific plasticized materials. Under REACH, an SVHC concentration above 0.1% in an article triggers communication or notification obligations, and because the Candidate List is updated approximately every six months, declarations must be tied to the list version date. Engineering teams should establish a restricted-substance master-data table containing at least: substance name, CAS number, regulatory source, applicable material category, concentration limit, exemption clause number and validity period, test-method standard (such as relevant IEC 62321 series methods for disassembly and determination in electrical and electronic products), and assessment unit (homogeneous material or complete article). Three common error areas require special attention: first, exemptions, such as lead in certain alloys or high-temperature solder, for which the clause number, scope, and expiry review must be recorded rather than simply stating compliance; second, process-introduced substances, since printing itself may not introduce cadmium, while post-processing plating solutions, passivation solutions, cleaning agents, release agents, adhesives, and inks may do so; and third, supplier changes, as a change of lot or production line for the same grade requires new declarations and does not permit reuse of an attachment from a year earlier.
3. Evidence Chain: SDSs, Supplier Declarations, and Test Reports Each Serve a Different Role
The three document types are not interchangeable. An SDS explains hazards and protective measures, while its composition section often provides ranges or omits information as trade secrets, making it insufficient for concentration-based compliance assessment. A supplier full material declaration or compliance declaration provides composition information and commitments to limits, but depends on the supplier's sampling and integrity. A third-party test report provides specific methods and measured values, but only covers the sampling locations of the submitted specimen. A verifiable approach is to establish a four-tier evidence chain: Tier 1, material identity (purchase orders, grades, lot numbers, CoAs, incoming-inspection records, and document hashes); Tier 2, composition declarations (full material declarations or IEC 63000-style material declarations containing CAS numbers, concentration ranges, SVHC version, exemption references, signatory, and date); Tier 3, process-introduction assessment (listing all post-processing auxiliary materials and consumables, identifying whether each may introduce restricted substances, whether residue risks exist, and documenting cleaning and curing validation); and Tier 4, verification and release (XRF screening for rapid assessment of elemental substances, and ICP-OES/MS or GC-MS for quantitative determination of phthalates and brominated flame retardants; reports must state sampling locations, disassembly methods, detection limits, measurement uncertainty, and decision rules). When results are close to a limit, apply conservative decisions using the uncertainty band under ILAC-G8 / ISO 14253-1; do not ignore U and directly declare compliance.
4. Integrate Substance Compliance into the 3D Printing Delivery Process
Compliance documentation should not be assembled only before shipment; it must be embedded at lifecycle milestones. During quotation and order review, first confirm the sales region, customer-industry regulations—electrical and electronic equipment, medical devices, automotive, toys, and food-contact applications each differ—and the required declaration types, then write restricted-substance requirements as assessable clauses in the technical agreement. During design, record material and surface-treatment codes in the BOM and model handover package to prevent a later coating change from leaving declarations unupdated. During purchasing and incoming inspection, collect declarations by lot and establish validity periods and change triggers. The maximum powder reuse count should also be recorded, because oxygen content and contamination history of recycled powder affect material identity. During production, link the auxiliary-material list, cleaning parameters, witness coupons, and work orders; any substitute auxiliary material must be processed through a change order. At release, the quality gate checks declaration versions, the list of homogeneous materials covered by test reports, whether exemptions remain valid, and whether packaging materials have been declared separately; if any item is missing, release is placed on hold. The final delivery package includes a homogeneous-material mapping table, restricted-substance declaration of conformity, SVHC communication letter where triggered, test-report index, exemption list, and version-controlled records. All documents must be recorded in accordance with ALCOA+ principles and retained beyond the contractually specified traceability period.
5. Quantitative Dashboard and a First-Pass Checklist
Six metrics are recommended for managing this chain: homogeneous-material list coverage (declared rows ÷ required rows; target 100%), declaration validity rate (unexpired and version-matched proportion ≥98%), process auxiliary-material assessment coverage (target 100%), consistency rate between test reports and limit determinations, timeliness of declaration updates following change triggers (target ≤3 working days), and first-pass customer acceptance rate for compliance documentation (target ≥95%). The 10-minute pre-release checklist is: first, verify the sales region and regulatory version; second, confirm that the BOM has been broken down into homogeneous materials without vague “other” entries; third, verify traceability of the grade, lot number, and declaration number for every material row; fourth, confirm all post-processing auxiliary materials have been assessed; fifth, verify the SVHC list version date and exemption validity; sixth, check test sampling locations and disassembly methods; seventh, confirm uncertainty has been considered for values near limits; eighth, verify packaging and marking materials have been declared separately; ninth, confirm change orders have been synchronized with declarations; and tenth, verify signatures, dates, and document hashes are complete. If any item is negative, a declaration of conformity must not be issued.
Conclusion: From “Forwarding Certificates” to a Verifiable Substance Ledger
The challenge of product chemical-substance compliance is not memorizing a few limits. It is breaking down a printed finished part by homogeneous material, translating regulatory provisions into data fields, assigning proper roles to SDSs, supplier declarations, and test reports, and ensuring that every material or process change triggers a declaration update. For platforms such as lantu3D that connect design, manufacturing, post-processing, and delivery, this approach extends “environmental protection” beyond workshop emissions and carbon narratives to the traceability of substances in the physical part received by the customer. Its direct value lies in reducing export rejections and repeated customer requests for supplementary documentation. Its indirect value is allowing compliance constraints to shape material selection, post-processing routes, and packaging solutions at the quotation stage, rather than discovering a missing link in the evidence chain just before shipment.
Submit a model, drawing, image or written notes. Engineers will review material, process, finishing and delivery based on actual use.