
Introduction: Why a Single Supplier Change Notice Can Invalidate an Entire Batch of Parts
Materials and outsourced-process supply chains in 3D printing are highly coupled. Changes in particle-size distribution, oxygen content, and recycled-powder blending ratio for the same grade of metal powder; melting point and flowability for the same grade of PA12 powder; or even the process provenance of the same model of protective lens, cleaning agent, or heat-treatment furnace can create drift when a supplier quietly changes production location, equipment, formulation, or discontinues a product. For platforms such as lantu3D, which manage the full lifecycle from drawings and design through physical delivery, the issue is not whether a notice was received, but whether that notice can be translated into a determinable, segregable, and traceable engineering event. If a supplier product change notification (PCN) remains only in a purchasing email while the shop floor continues to run machines using the old process card and inspection lots are still formed under the old parameter revision, customers may receive parts with discontinuities in mechanical performance, dimensional stability, or compliance declarations despite identical appearance.
1. Define the Subject First: A PCN Is Neither an Internal ECN nor a Customer Change Order
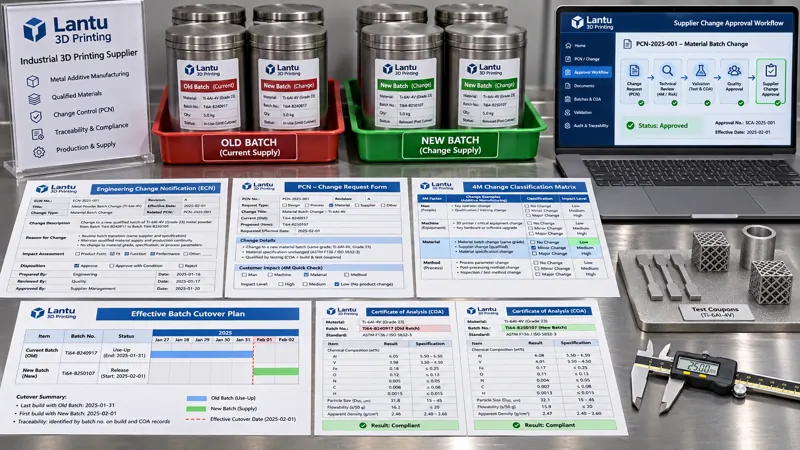
A PCN concerns a change initiated by an external supplier, received and dispositioned by the organization. An internal engineering change notice (ECN) generally answers: “After a customer or internal drawing revision, how should models, work in process, inventory, tooling, and quotations be transitioned?” A customer requirement change answers: “How should acceptance specifications be revised?” Supplier qualification and sourcing decisions answer: “Which supplier should be selected and under what purchasing terms?” A PCN answers: “What is an already approved supplier changing from the old state to the new state, from which effective lot onward, does the organization accept it, is change validation required, and must the customer be notified?” A usable PCN record should at minimum be linked to the supplier code, material number, material revision, change category, before-and-after descriptions, reason, supplier internal change number, proposed effective lot or date, sample and COA/COC numbers, last-purchase deadline for old material, contact person, and issuance timestamp. A “change notification” without an effective-lot field cannot define boundaries for inventory and work in process, and should be treated as information rather than a controlled engineering document.
2. Classify Changes by 4M1E Instead of Requalifying Everything or Releasing Everything
It is recommended to break changes into five categories using 4M1E: material changes (powder origin, atomization process, particle-size range, recycled-powder ratio, resin formulation, filament lot rules); machine and tooling changes (supplier production equipment, sieving equipment, heat-treatment furnaces, mold cavity numbers); method changes (standards or parameter ranges for cleaning, passivation, packaging, and test methods); personnel and site changes (relocation of critical processes, secondary subcontracting of outsourced processes, manufacturing-address changes); and environmental/compliance changes (REACH/SVHC declarations, RoHS exemptions, hazardous-waste disposal provider changes). For each category, first determine whether it affects frozen CTQs and process windows, then assign an A/B/C disposition level. Level A may affect safety, fatigue, or regulated attributes in implant and aerospace applications; new lots are suspended from production by default and may be released only after sample testing, witness coupons, full CTQ inspection, and any required written customer approval. Level B affects process stability but does not alter acceptance criteria; it requires comparative validation across at least three independent builds and tightened inspection of the first lot. Level C covers documentation-only or packaging-label changes and requires only a document consistency review and first-lot labeling verification. The classification decision must be entered in the PCN ledger and linked to the material master-data revision.
3. Change Validation: Use Reviewable Data to Demonstrate “Old/New Equivalence” or the Need for a Revision Change
For metal powders, compare at least D10/D50/D90, Hall flow rate, apparent/tap density, oxygen and nitrogen increases, and the proportion of satellite and hollow particles. Print standard test coupons using the same parameter package, then evaluate density, tensile properties, and critical dimensions. For polymers such as PA12, compare melting/crystallization windows, viscosity or melt flow, moisture content, and standard specimen strength. Validation cannot consist solely of confirming that supplier COA values fall within specification limits; results must be reproduced on the organization’s equipment, with its parameter package and post-processing chain. Retained samples from the old lot should be used as controls: three specimens in the old state and three in the new state, with critical characteristics evaluated using the same gauges, sampling orientations, and inspection-lot rules. A Level B change may be deemed equivalent only if mean drift between three consecutive independent builds is less than one-third of the historical standard deviation and no result falls within 10% of a CTQ tolerance limit. If differences are significant, this is not merely a “notice acknowledged” situation; it triggers an internal ECN. Update the process card, parameter-package revision, inspection-lot rules, quotation and cost-review sheet, and referenced technical-agreement documents, and specify the build number from which the new parameters take effect.
4. Lot Transition and Inventory: Express “Starting with Which Bag” Through Four Status Colors
The area most likely to lose control in a PCN is where old material, new material, work in process, and delivered parts remain under the same lot designation. In WMS/MES, establish four status categories for each affected material: old lot released, old lot frozen pending use, new lot pending validation, and new lot released. Inventory should be counted bag by bag according to container seal number and lot number, recording gross weight, tare weight, net weight, storage location, inspection-report number, and PCN number. Work-in-process builds should be traceable using “machine start timestamp + old-lot identifier + equipment number + parameter-package hash.” Parts from a build spanning a transition point must not be combined into one inspection lot; they should be split into old-material and new-material sub-lots, each with separate witness coupons retained. Whether old lots may be consumed depends jointly on the classification decision, customer contract terms, and remaining quantity. Level A changes normally do not permit continued use of old lots without authorization; Level C changes may be consumed on a first-in, first-out basis, but shipping documentation must identify the effective lot. Delivered lots are not automatically recalled because of a PCN, but it must be possible to trace from a part serial number, within 30 minutes, to the supplier PCN number, old-lot COA, inspection-lot number, and report revision for customer audits or dispute retesting.
5. Customer and Contract Boundaries: When Written Approval Is Mandatory
Whether customers must be notified does not depend on the perceived magnitude of a change, but on whether it affects “frozen items” in the technical agreement. If the agreement specifies material grade plus supplier plus country of origin, powder-lot locking, a maximum recycled-powder blend ratio, a designated heat-treatment furnace, or a designated test method, any change to these fields requires written customer approval. If the agreement specifies only performance requirements and acceptance criteria, and A/B/C validation demonstrates that both old and new states meet those criteria, the matter may be closed internally with batch records retained as evidence, provided shipping documentation remains traceable. Purchasing terms should predefine PCN lead time—typically 30–90 days, and no less than 120 days for discontinuation/EOL—along with the final purchase window, obligations to provide samples and COAs, a default prohibition on secondary subcontracting, a prohibition on unilateral implementation of changes to critical characteristics, and responsibility boundaries for retesting, rework, or delivery losses caused by failure to notify. This turns “the supplier changed the lot without telling us” from a dispute into an enforceable contractual condition.
6. Implementation Checklist and Common Failure Modes
Minimum ledger fields: PCN number, supplier code, material number, change category, 4M1E cause, A/B/C level, effective lot/date, validation report number, internal ECN number, inventory disposition order number, customer approval number, obsolete-document record, first-lot tightened-inspection result, and closure date. Five control gates: D1 purchasing receipt and numbering; D2 joint engineering/quality classification; D3 validation and material-master-data revision freeze; D4 segregation of inventory, work in process, and inspection lots; D5 review 30 days after first-lot release. Five common failures are: filing a PCN as a quotation email without entering it into controlled documentation; validating only the supplier COA rather than the internal process chain; recording the effective lot as “starting next month,” resulting in mixed material in the same build; releasing material as an “equivalent grade” when the customer technical agreement freezes supplier origin; and allowing an old parameter package to remain callable from the machine after PCN closure. Randomly select one or two closed PCNs every week for traceability drills, requiring traceability from any finished part to the PCN number, old/new COAs, validation report, and approval record within 30 minutes. The target first-pass success rate should be no lower than 95%.
Conclusion
The engineering value of a supplier product change notification lies not in having “received” it, but in converting an external change into a controlled object: with a unique identifier, 4M1E attribution, A/B/C classification, equivalence validation, an effective lot and four-color inventory status, defined customer-approval boundaries, and a traceable evidence chain. In this way, lantu3D can keep materials, processes, inspection, delivery, and commercial terms on a single lifecycle chain, ensuring that external supplier changes do not compromise consistency from design through physical delivery.
Submit a model, drawing, image or written notes. Engineers will review material, process, finishing and delivery based on actual use.