
Introduction: The System Documents Exist, but Which Clause Is Being Met?
Standardization efforts at many 3D printing companies remain at the level of simply “having documents”: quality manuals, procedure documents, and work instructions are complete, and system certificates are displayed on the wall. However, during a customer audit or third-party certification audit, auditors ask: “Which standard number and clause are you working to? What is the acceptance basis? Where are the supporting records retained?” If the only answer is “this is how we have always done it,” the system has deteriorated from an executable system into one intended merely for display. lantu3D has repeatedly encountered this gap while participating in aerospace, medical, and automotive component projects: process capability may be adequate, but unclear clause mapping, non-quantifiable criteria, and incomplete evidence chains lead to repeated first article qualification efforts and nonconformities raised during external audits. Moving standards from the “document level” to the “clause level” is the dividing line at which a standardization system begins to exert real control.
I. First Distinguish Standard Types and Their Hierarchy of Authority
The most common error in standardization work is treating all “standards” as equivalent documents. In fact, their authority and purpose differ substantially. National standards (GB) and industry standards establish general requirements and test methods and serve as entry thresholds. Association standards are generally closer to specific processes, are updated more rapidly, and provide more detailed technical indicators. Enterprise standards are the highest-authority internal documents and can incorporate customer-specific requirements. Reference relationships must be clear: the technical indicators in enterprise standards must not be lower than those of higher-level standards, and the document cover must identify the list of referenced documents and their edition years. At a minimum, an executable standards register should include the standard number, title, edition year, issuing organization, applicable scope clauses, applicable in-house processes, replacement relationships, and withdrawal date. Missing edition years are among the most common deficiencies: when a standard is revised but old acceptance criteria continue to be used, test results may be legally invalid.
II. Break Standards Down into Clauses and Map Them to Internal Control Points
Copying the full text of a standard into a work instruction is meaningless. The correct approach is to break the standard down into four levels: clause, requirement, control point, and record. Taking laser powder bed fusion (LPBF) as an example, a standard clause concerning “raw material acceptance” can be divided into four control points: re-verification of powder chemical composition, particle-size distribution testing, apparent density and flowability measurement, and batch retention samples. Each control point must specify the test frequency (every batch/every five batches), sampling method, acceptance criteria (for example, oxygen content ≤0.13%, with the specific value determined by alloy grade and standard edition), record form number, and retention period. Only after this level of work is completed does the standard truly reach the workstation. In practice, one primary process standard can be broken down into 30 to 60 auditable control points, approximately one-third of which require quantitative criteria, while the remainder are conformity-verification items.
III. Criteria Must Be Measurable: Avoid Terms Such as “Appropriate” and “When Necessary”
Conformity criteria are where audits most easily lose points. Wording such as “the surface shall be clean” or “cleaning shall be performed when necessary” cannot be objectively determined or traced. These statements should be replaced with measurable and reproducible requirements: no more than three residual powder particles larger than 50 μm in a 100× field of view; residual powder mass in internal channels not exceeding 0.5% of the total part mass; drying conditions after cleaning of 60°C for 60 minutes, with moisture content after removal from the oven not exceeding 0.05%. Criteria should also specify the measurement method and instrument resolution requirements. Using calipers with 0.02 mm resolution to assess a 0.01 mm tolerance zone renders the data itself invalid. Measurement system analysis (MSA) and gauge R&R are therefore not optional; they are prerequisites for valid acceptance criteria.
IV. Document Control: Revisions, Controlled Copies, and Obsolescence
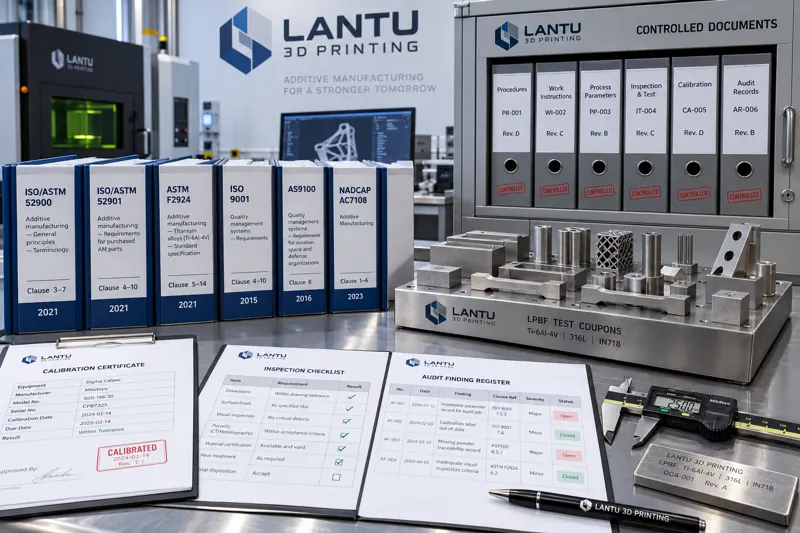
Controlled documents are the physical vehicle for clause-level implementation. Document control must address four issues. First, revision uniqueness: two revisions of a work instruction with the same document number must not be present on the shop floor, and obsolete revisions must be withdrawn or marked “obsolete copy retained.” Second, changes must be traceable: every revision must retain its reason for change, scope of impact, and effective date. Third, external documents must be identified: customer drawings, supplier material certificates, and referenced standards are all external documents and must be included in the register and periodically checked for updates. Fourth, records and documents must be managed separately: records are evidence of what was done and must not be combined with documents that specify how work is to be performed. Enterprise standardization system documents are typically divided into four levels: manuals, procedure documents, work documents, and record forms. The lower the level, the more specific and role-oriented it becomes.
V. Audit Checklists and Closed-Loop Evidence
Internal audits should not be exercises in finding typographical errors. They should verify whether clauses are implemented, criteria are met, and evidence is traceable. An audit checklist for an LPBF workshop can be organized by clause number. Each column should include the clause number, audit question, sampling method (such as sampling three records from the most recent three months), acceptance criterion, evidence type, and finding description. Nonconformities should be managed by severity. Minor nonconformities require correction and root-cause analysis, while major nonconformities involving batch risk require traceability actions and customer notification. The criterion for closure is not that “the corrective action report has been completed,” but that “the same type of issue does not recur in sampling during the next audit cycle.” Linking corrective-action effectiveness to the sampling performed in the next internal audit is a key mechanism for preventing corrective actions from becoming a paper exercise.
VI. Integration of Industry-Specific Standards
General quality management systems address whether a system exists; industry-specific standards address whether it is sufficiently specialized. Aerospace focuses on special-process validation, first article inspection, and nondestructive testing personnel qualifications. Medical applications focus on biocompatibility, traceability, and sterilization validation. Automotive applications focus on process audits and production part approval procedures. These requirements often appear as customer-specific requirements and take priority over general clauses. The standards register must therefore include a dedicated field for customer-specific requirements and clearly define their relationship to enterprise standards and the rules for resolving conflicts: the stricter requirement prevails and must be confirmed in writing in the technical agreement, avoiding post-delivery disputes caused by inconsistent acceptance criteria.
Conclusion
The maturity of a standardization system is not determined by the number of documents, but by whether it can answer three questions: which standard number and clause apply, what measurable criteria are used, and in which form are the records retained? Only by breaking standards down into clauses, mapping clauses to control points, writing control points as quantitative criteria, and embedding those criteria into controlled documents and audit checklists can standardization become a productivity tool rather than a display item. For 3D printing businesses centered on delivery from digital blueprint to physical part, the more robust this foundation is, the more controllable first-pass first article approval, external-audit nonconformities, and cross-project reuse efficiency will become.
Submit a model, drawing, image or written notes. Engineers will review material, process, finishing and delivery based on actual use.