
Introduction: Why This Issue Is Becoming Critical
Satisfaction comes from predictable delivery: How 3D printing customer service systems can shift from reactive to proactive is, at its core, about building the capability to move 3D printing from being able to make it to being stable, explainable, and deliverable. As customers shift from appearance prototypes to functional parts, small batches, and rapid spare parts, relying solely on experience-based quoting and ad hoc machine tuning is no longer enough to meet lead-time, quality, and cost requirements. lantu3D Printing is positioned as a lifecycle management and implementation platform from blueprint and design to physical delivery, so every step needs to be managed in a structured way.
1. Customer experience comes from stable expectations
Industry customers fear one thing most: lack of transparency. They do not know whether the model can be printed, when it will be scheduled, why the price increased, or how exceptions will be handled. The service team should clearly explain milestone status, risk causes, and alternative solutions. In real projects, engineers cannot look at a single indicator alone; instead, they must place the part's use case, load direction, assembly relationship, surface requirements, temperature resistance, and budget on the same decision table. For example, precision appearance parts usually prioritize SLA or high-precision resin, wear-resistant structural parts may choose SLS nylon, and parts with high load-bearing and temperature-resistance requirements need evaluation of SLM aluminum alloys, titanium alloys, or stainless steel.
Key parameters must be recorded in a verifiable way: common layer thickness ranges are 0.05-0.2mm, functional part wall thickness is generally not recommended to be below 1.2-2.0mm, and process compensation should be reserved for hole diameters, threads, and snap-fit locations. Only by feeding these constraints back to the design side in advance can manufacturing avoid repeated rework later.
2. From problem analysis to engineering decisions
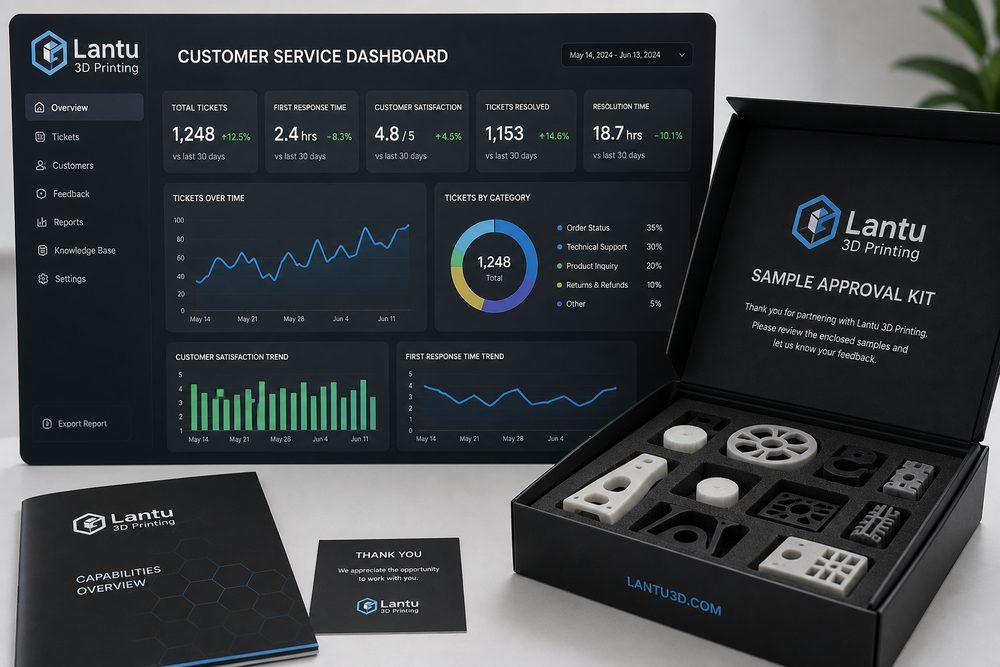
Improve satisfaction through standard scripts, progress notifications, sample confirmation forms, and a post-sales issue database. Common failures do not necessarily come from the equipment itself, but from misalignment among requirements input, model design, material selection, print orientation, post-processing, and inspection standards. For example, if a customer asks for high strength, a good surface finish, low price, and delivery tomorrow, then without prioritizing these requirements, rework is likely to occur late in production.
At the project launch stage, it is recommended to complete three types of judgments: first, whether the part is an appearance sample, an assembly sample, or a functional part; second, whether the key indicators are dimensions, strength, appearance, temperature resistance, or lead time; third, who bears the cost of failure and whether first-piece confirmation is required. The earlier these judgments are completed, the easier it is for the project to move forward as planned.
3. Practical implementation methods
In implementation, a combination of a standard parameter library, a project review form, and anomaly postmortems can be used. The standard parameter library records recommended settings for different materials, machines, and layer thicknesses; the project review form is used to confirm model integrity, minimum wall thickness, support risks, post-processing methods, and inspection criteria; anomaly postmortems turn issues such as warping, delamination, porosity, dimensional deviation, and surface defects into rules that can be avoided next time.
For small-batch orders, first-piece or sample validation should be performed before batch scheduling begins. Critical dimensions can be checked with calipers, a coordinate measuring machine, or scan comparison; appearance parts should clearly define sanding, painting, coloring, or polishing standards; and assembly parts should complete actual fit testing before delivery. This not only reduces customer risk, but also reduces internal rework.
4. Management metrics and continuous optimization
What companies should focus on is not the peak speed of a single machine, but the overall efficiency from order intake to delivery. It is recommended to continuously track quotation response time, first-pass review rate, first-article pass rate, material loss rate, equipment utilization rate, rework rate, on-time delivery rate, and customer repeat purchase rate. Each metric corresponds to an optimizable link.
When data accumulates to a certain scale, the platform can further support automated quoting, intelligent scheduling, risk alerts, and knowledge base recommendations. lantu3D Printing should condense these experiences into reusable processes so that customers get not just a part, but a more certain manufacturing path.
Conclusion
Competition in the 3D printing industry is shifting from equipment quantity to engineering capability, process capability, and delivery capability. Whether it is materials, processes, applications, equipment, service, quality, cost, customer experience, digitalization, or supply chain, the truly valuable approach is to identify, quantify, and manage uncertainty in advance. For industry practitioners, establishing standards, accumulating data, and continuously reviewing and improving are the core path to turning 3D printing into stable productivity.
Submit a model, drawing, image or written notes. Engineers will review material, process, finishing and delivery based on actual use.