
Introduction: Shipping Damage Is Not the End of Logistics, but a Test of Evidentiary Capability
A metal additively manufactured part that has passed full-dimensional CMM inspection arrives at the customer site, where unboxing reveals flange-face dents, deformed threaded holes, and damaged packaging inserts. A dispute immediately arises: Did the defects exist before shipment, or were they caused by impact during transit? Was the packaging design inadequate, or was the carrier responsible for rough handling? If a complete chain of evidence cannot be established at the unboxing site, liability is often left unresolved for weeks amid conflicting claims from both parties, ultimately ending in concessions that result in both financial loss and damaged trust. For high-value, low-volume, highly customized 3D-printed parts, the core of shipping-damage handling is not post-incident negotiation skill, but whether reproducible unboxing inspection procedures, preservable evidence-collection requirements, and determinable liability boundaries have been established in advance. In its lifecycle delivery management, lantu3D moves shipping-damage control forward into shipping documentation and unboxing procedures so that every exception can be supported by evidence.
I. Define Liability Boundaries First: How to Identify Four Types of Shipping Damage
The first step in handling shipping damage is not taking photographs, but determining which category the damage belongs to. In practice, it can be divided into four types. The first is manufacturing-residual damage, characterized by marks related to processing operations, such as support-removal remnants, machining tool marks, or discontinuous polishing patterns. The boundaries of such damage often correspond to the process path. The second is inadequate-packaging damage, concentrated at edges, bosses, and slender features where the part contacts the inner packaging. When multiple parts in the same batch show damage at the same locations, it indicates that the cushioning design did not protect critical vulnerable surfaces. The third is transport-impact damage, which is randomly distributed and accompanied by carton deformation, activated impact indicators, or loosened stretch wrap, with the damage direction consistent with the direction of impact or dropping. The fourth is environmental-corrosion damage, manifested as rusting, oxidation discoloration, or condensation inside the package, with timing corresponding to temperature and humidity logger data.
The key to distinguishing these four categories is to map damage characteristics to a timeline. Damage occurring before the delivery stage may have traces that are covered or contaminated by subsequent operations, whereas damage occurring during transportation must coincide in time with impact records and carton condition. From an engineering perspective, it is recommended to retain a condition baseline before shipment: clearly document every critical surface with images and record its identification number. This provides a reference frame for subsequent comparison. Without a baseline, any post-incident determination is merely speculation.
II. Standard Unboxing Inspection Procedures: Make Evidence Collection a Process Rather Than an Improvised Response
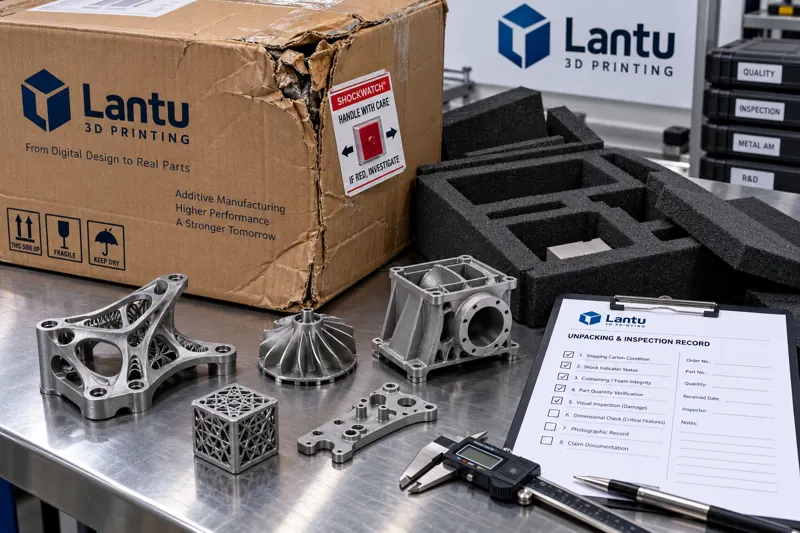
The most common loss of control during unboxing occurs when personnel rush to remove the part after discovering damage, thereby disturbing the original condition of the scene. The standard procedure should be formalized into six steps. First, before opening the package, take photographs of all six sides of the outer carton, including shipping marks, seal condition, impact and tilt indicators, stretch-wrap condition, and strapping condition. Second, record the unboxing time, location, persons present, and outer-carton weight. Third, remove cushioning materials layer by layer in sequence, photographing each layer and preserving the original positional relationship of the inserts. Fourth, after removing the part, first photograph its overall condition against the original packaging background, then take close-up images of damaged areas with a scale. Fifth, conduct an initial dimensional verification of the damaged area to determine whether assembly function is affected. Sixth, complete an unboxing inspection record and obtain signatures from both parties.
The value of this procedure is that it transforms evidence collection from an individual habit into an organizational capability. For printed parts with high unit value, it is advisable to require continuous video recording for every unboxing, starting from the first cut into the packaging and without editing. Video provides a better reconstruction of layer-by-layer relationships than photographs and can also address concerns about staged evidence. In addition, the outer carton should not be discarded or moved to another area before evidence collection is complete, because the carton itself is one of the most important evidence carriers.
III. The Composition of an Evidence Chain: Ensure Every Claim Has Supporting Documentation
A claim supported by sufficient evidence generally requires a closed loop of five categories of documentation. The first is delivery-condition evidence, including pre-shipment inspection reports, images of critical surfaces, identification numbers, and batch records, used to demonstrate compliant condition at shipment. The second is packaging-compliance evidence, including packaging design descriptions, cushioning material specifications, drop or vibration validation records, and carton-sealing operation photographs, used to demonstrate that the packaging design was reasonable. The third is in-transit condition evidence, including impact indicators, tilt indicators, temperature and humidity logger data, and carrier handover and receipt records, used to reconstruct the transportation process. The fourth is damage-fact evidence, including unboxing video, outer-carton photographs, damage close-ups, and dimensional verification records. The fifth is value evidence, including contract price, invoices, and cost estimates for rework or remanufacture.
These five categories connect sequentially over time, and the absence of any one creates a break in the evidence chain. The most common gap is in the second category: packaging designs have never been validated, making it impossible to prove packaging compliance once damage occurs. The next most common gap is in the third category: no indicators or data loggers were installed, making it impossible to attribute damage to transportation. Therefore, building evidentiary capability must begin before shipment, rather than after unboxing.
IV. Liability Determination Criteria and Allocation of the Burden of Proof
Liability should be determined based on criteria rather than positions. Practical criteria include the relationship between damage locations and cushioning structures, consistency between the direction of damage and the activation direction of indicator labels, whether the damage distribution across parts from the same batch follows the same pattern, whether damage fractures show fresh oxidation or contamination, and whether in-transit logger curves show abnormal peaks. If indicator labels have not been activated but random dents are found on the parts, the cause is more likely insufficient internal restraint or a pre-shipment condition issue. If indicators are activated and the outer carton is deformed, carrier responsibility is more clearly established. If data loggers show prolonged high humidity and the damage manifests as corrosion, responsibility for environmental control becomes prominent.
For burden-of-proof allocation, it is advisable to specify in contracts and delivery documents that the consignee is responsible for following standardized unboxing procedures; the shipper is responsible for proving pre-shipment condition and packaging compliance; and the carrier is responsible for maintaining in-transit condition records. Prior agreement is better than subsequent argument. For cases where the cause cannot be determined, clear handling thresholds should be established. For example, losses below an agreed amount may be handled through expedited replacement, while losses above that threshold trigger a joint investigation, preventing minor disputes from consuming labor resources far exceeding the value of the goods.
V. Time Limits, Loss Calculation, and Closed-Loop Improvement
The success of a claim often depends on timing. Transportation contracts typically impose strict deadlines for notifying parties of cargo damage, sometimes calculated as only a few days after receipt, with late notification deemed a waiver of the claim. Therefore, any anomaly identified during unboxing must be reported internally on the same day, and written notice must be issued to the carrier and insurer within the agreed time limit, together with preliminary images. The time at which written notice is sent must also be documented.
Loss calculations should distinguish between direct and indirect losses. Direct losses include remanufacturing costs, materials and machine time, rework operations, reshipment, and packaging costs. Indirect losses include schedule delays and production-line waiting costs; these are generally recoverable only when separately stipulated in the contract. The calculation should include a detailed cost breakdown rather than a lump-sum quotation.
More importantly, the process requires closed-loop improvement. Every shipping-damage incident should be incorporated as an input for revising the packaging solution: which vulnerable feature was not protected, which cushioning clearance was insufficient, and which box design failed during actual use. Only by converting individual cases into design rules can similar issues be prevented from recurring. It is recommended that the quality system maintain a dedicated shipping-damage register, categorize and analyze incidents by damage type, and incorporate high-frequency issues into packaging design standards and shipping work instructions.
Conclusion
The engineering-based handling of shipping damage is fundamentally about converting post-incident disputes into pre-agreed requirements and evidence preservation during execution. Classifying damage types, standardizing unboxing procedures, building five categories of evidence chains, clarifying determination criteria and burdens of proof, controlling time limits, and feeding findings back into improvement form a complete closed loop. For the highly customized, high-value, low-volume delivery model typical of 3D printing, the benefits of establishing this closed loop far exceed those of any individual claim: it makes delivery reliability demonstrable and keeps customer relationships stable even when exceptions arise.
Invia un modello, un disegno, un'immagine o note scritte. Gli ingegneri valuteranno materiale, processo, finitura e consegna in base all'uso effettivo.