
Introduction: From a single print to a deliverable engineering loop
Customer service and satisfaction in 3D printing is not about one machine or one material. It is about the full chain of design, process, manufacturing, inspection, and delivery. For industry teams, the challenge is usually not whether a part can be formed, but whether it can be delivered with stable cost, traceable quality, and a repeatable workflow. lantu3D Printing emphasizes lifecycle management from design to physical part: when a model or drawing arrives, materials, structure, batch size, post-processing, inspection, and lead time are evaluated together so decisions are not based only on a single-part quote or past one-off print experience.
To improve customer service and satisfaction, companies need to turn experience into executable standards. For example, confirm wall thickness, hole diameters, assembly clearances, support areas, and critical dimensions during review; record layer thickness, power, scan speed, powder refresh rate, or nozzle temperature during production; and use dimensional reports, appearance criteria, and review notes at delivery to guide the next project. This kind of system turns 3D printing from fast prototyping into manageable on-demand manufacturing.
1. The core issue: satisfaction comes from expectation management, process transparency, and fast response, not just from delivering the final part
The essence of satisfaction is to expose and quantify uncertainty early. Many projects focus on material price and machine hours at quotation time, while overlooking hidden costs such as design changes, support removal, heat treatment, sanding and blasting, threaded inserts, dimensional remeasurement, and packaging or shipping. For metal SLM parts, common control items include 20–60 μm layer thickness, oxygen monitoring, baseplate preheating, scan strategy, and stress-relief heat treatment. For SLS nylon parts, powder refresh rate, bed temperature, cooling curve, and post-dyeing process directly affect warpage, toughness, and color consistency. For FDM fixtures and jigs, nozzle diameter, infill ratio, wall line count, and build orientation determine strength anisotropy.
From a management perspective, the goal is not the extreme of one parameter, but a practical parameter window. Engineering prototypes may accept a shorter cycle and less finishing, while assembly verification parts must include hole location, snap-fit features, and clearance in inspection items. Display parts, by contrast, must prioritize surface texture, paint adhesion, and color consistency. Defining purpose, risk, and acceptance criteria at project kickoff reduces rework and helps customers understand price differences more clearly.
2. Engineering decisions: how materials, processes, and post-processing work together
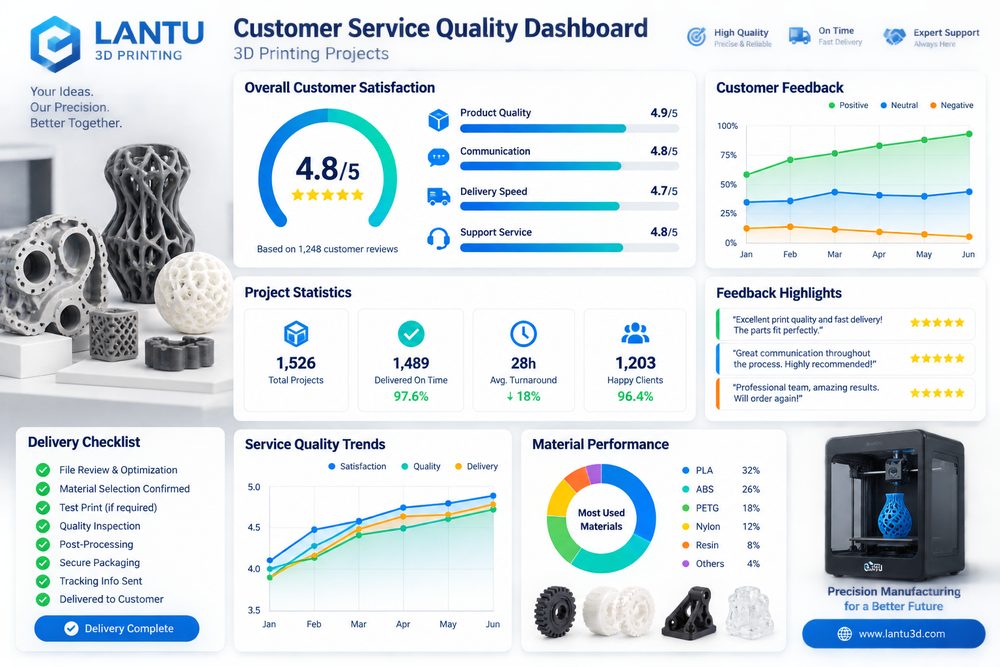
Material selection should follow the application scenario, not just the material name. Measurable metrics include first response time, quote accuracy, on-time delivery rate, rework rate, complaint closure time, and repeat order cycle. When a part needs impact resistance and light weight, PA12, PA11, or glass-fiber-reinforced nylon usually come first. When a high-fidelity surface or transparency is required, SLA or DLP resins are more suitable. When high-temperature strength, fatigue performance, or complex internal channels are needed, aluminum, titanium, or stainless-steel metal printing provides real engineering value. Each option implies downstream processing: nylon parts may need blasting, dyeing, and impregnation; resin parts require secondary curing, sanding, and coating; metal parts may need support removal, heat treatment, machining, and nondestructive testing.
In project reviews, lantu3D Printing usually discusses DFAM design, process route, and inspection method in the same table. For example, a thin-walled shell may be printable from a forming standpoint, but if it must later be painted and withstand screw torque during assembly, local ribs, fillets, and space for threaded inserts should be added. If a metal flow channel part traps residual powder, the design stage must add powder-removal holes, inspection holes, or a different build angle. The earlier the engineering decision is made, the lower the later cost.
3. Implementation path: use data to deliver stable results
One R&D customer revised its structure several times within three months. The platform kept every model version, quote, and test result, so by the fourth round it could reuse historical parameters directly and cut communication time by more than half. The shared lesson is simple: validate parameters with a small batch first, then scale up to stable production; confirm critical dimensions and functional surfaces before optimizing appearance; define test samples and sampling ratios before discussing lead time. For R&D samples under 10 pieces, critical dimensions can be fully inspected one by one. For small-batch orders of 50 to 200 pieces, a first-article check, in-process sampling, final-piece verification, and exception isolation mechanism are needed. This keeps the flexibility of 3D printing while giving customers quality certainty close to traditional manufacturing.
Digital records are equally important. Every batch should retain model version, quote version, material lot, machine ID, process parameters, post-processing method, and inspection results. When a customer adds an order or changes the design later, the platform can quickly determine which parameters should be inherited and which risks must be reassessed. For collaborative supply-chain projects, CNC finishing, surface treatment, assembly, and packaging can also be placed in a single order view to reduce information loss across vendors.
4. Implementation checklist: turn experience into repeatable standards
The customer service checklist should cover requirement confirmation, risk notes, stage notifications, delivery instructions, after-sales entry points, issue closure, and review suggestions. Companies should embed the checklist into quotation and production workflows: first, confirm use case, load, temperature, appearance grade, and assembly relationships; second, check minimum wall thickness, hole size, overhang angle, powder-removal channels, and support accessibility; third, select material and process and specify the key parameter window; fourth, define post-processing, inspection, packaging, and delivery methods; fifth, record customer feedback and review conclusions after delivery. The checklist does not need to be complex, but it must be executed on every project.
For service providers, standardization does not mean less flexibility. On the contrary, only by standardizing routine risks can the team focus on truly complex engineering problems. For buyers, a transparent workflow helps determine whether the quote is reasonable, the lead time is credible, and quality responsibility is clear. Competition in 3D printing is shifting from “can it be printed” to “can it be delivered stably, optimized continuously, and supported for the long term.”
Conclusion: increase the business value of 3D printing through a lifecycle view
The key takeaway from improving customer service and satisfaction in 3D printing is that real value appears only when 3D printing is managed as part of a complete manufacturing chain. Materials, processes, equipment, quality, cost, and service are not isolated modules; they influence one another as a system. By managing the full lifecycle from design to physical delivery, lantu3D Printing connects early review, process execution, post-processing inspection, and customer feedback to help companies achieve more controlled results in prototype validation, small-batch production, and complex part delivery.
Submit a model, drawing, image or written notes. Engineers will review material, process, finishing and delivery based on actual use.