
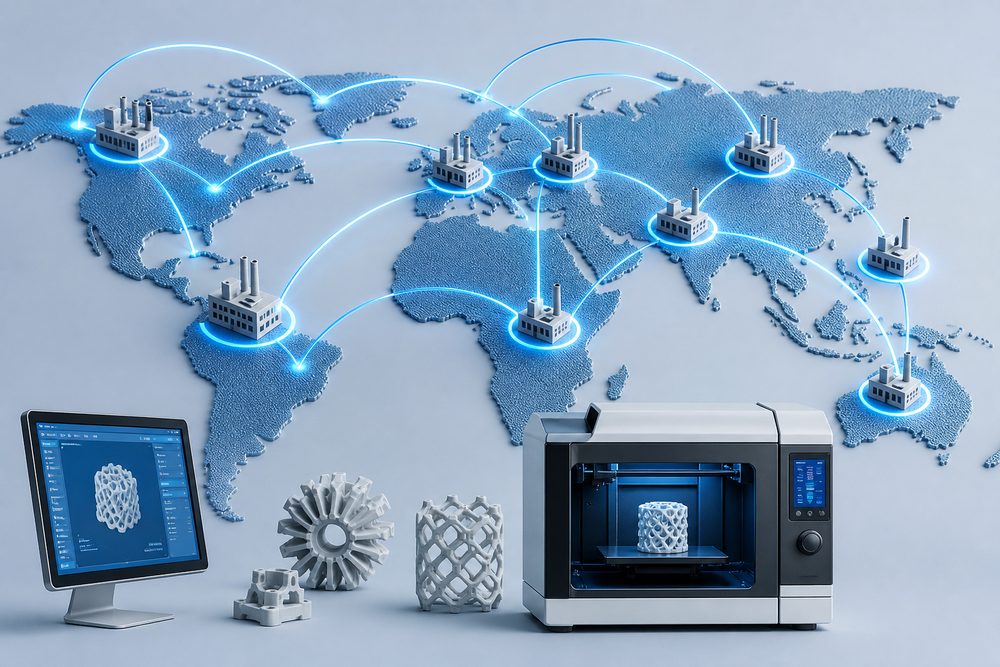
Introduction: The Dilemmas and Challenges of the Traditional Single-Point Production Model
In the field of industrial-grade 3D printing services, the traditional single-site production model is facing unprecedented challenges. According to 2025 data from the China Additive Manufacturing Industry Alliance, more than 78% of 3D printing service enterprises still adopt a centralized production architecture, resulting in an average delivery cycle of 5-7 days and a capacity utilization rate of only 52%-65%. When customer demand crosses regional boundaries, logistics costs account for as much as 18%-25% of total costs, severely constraining the improvement of service competitiveness.
Specifically, the single-site production model has three core pain points:
- Delivery timeliness bottleneck: After a customer in the Yangtze River Delta places an order, goods must be shipped from the Pearl River Delta production base, with an average logistics time of 2-3 days and emergency order response capability of less than 30%
- Capacity imbalance: In one region, equipment utilization exceeds 90%, while in another region idle capacity is as high as 40%, with a lack of flexibility in resource allocation
- Poor quality consistency: Cross-factory collaboration lacks unified standards; for the same SLM process part, the dimensional tolerance variation across different production bases reaches ±0.15mm, exceeding customer acceptance criteria
These issues have given rise to an urgent need for cross-regional collaborative manufacturing. By building a distributed production network, establishing a unified delivery system, and implementing networked operations, 3D printing service enterprises can shorten the delivery cycle to 24-72 hours, increase capacity utilization to over 85%, and reduce logistics costs by 35%-50%. This article will systematically explain the technical path and implementation key points for achieving this goal.
1. Core Architecture and Technical Foundation of Cross-Regional Collaborative Manufacturing
Cross-regional collaborative manufacturing is not simply a matter of setting up multiple sites; it is a systematic project built on three technical pillars: a digital collaboration platform, a standardized process system, and an intelligent scheduling system. Its core architecture is divided into four layers:
1. Device Access Layer
Each production base's 3D printing equipment must have IoT connectivity, enabling real-time data upload through the OPC UA or MQTT protocol. Taking SLA photopolymerization equipment as an example, the key parameters that need to be collected include:
- Laser power stability: fluctuation controlled within ±2% (standard value: 250-300mW)
- Scanning speed consistency: deviation ≤5% (recommended range: 8000-12000mm/s)
- Bath temperature control: 25±0.5°C (key to stable resin viscosity)
- Build platform levelness: flatness error ≤0.02mm per 100mm²
2. Data Transmission and Synchronization Layer
Cross-regional data synchronization must meet dual requirements of real-time performance and security. Recommended architectural solution:
- File transfer: STL/3MF model files use a resumable transfer mechanism, with a compression ratio of ≥60% and transfer time of ≤3 minutes for a single file (<500MB)
- Process parameter synchronization: Standardized process packages are distributed through a central database, including 12 core parameters such as layer thickness, infill density, and support structures, with synchronization latency ≤500ms
- Network bandwidth requirements: The uplink bandwidth of each production base must be ≥100Mbps to ensure the stability of simultaneous monitoring data uploads from 10 devices
- Data encryption: AES-256 encrypted transmission is adopted, in compliance with ISO 27001 information security standards
3. Intelligent Scheduling and Optimization Layer
The central scheduling algorithm is based on a multi-objective optimization model, taking into account four dimensions: delivery timeliness, equipment load, material inventory, and logistics costs. A typical optimization case:
| Scheduling Strategy | Average Delivery Time | Equipment Utilization | Logistics Cost Share | Overall Satisfaction |
|---|---|---|---|---|
| Proximity principle | 2.1 days | 68% | 12% | 72 points |
| Load balancing |
Next Step
Is this close to what you need?
Submit a model, drawing, image or written notes. Engineers will review material, process, finishing and delivery based on actual use. |