
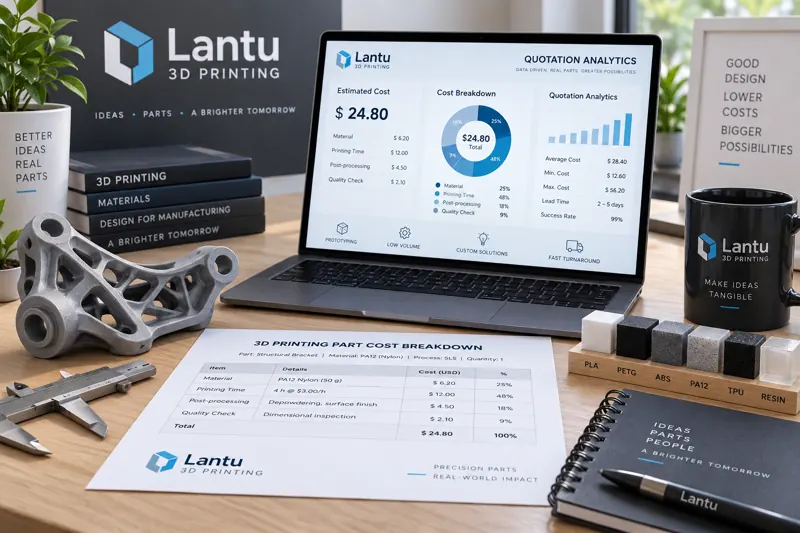
Introduction: Why Parts of the Same Size Can Have Widely Different Quotations
In inquiries from enterprise customers, a common question is: why can two 3D printed parts with similar external volume receive quotations that differ by several times? The reason is not arbitrary supplier pricing, but the fact that the cost drivers of 3D printing are completely different from traditional machining. It does not charge mainly for “batch size,” but for “complexity” and “materials.” Understanding the cost structure of a quotation helps procurement teams judge whether the unit price is reasonable, while enabling designers to reduce costs proactively at the modeling stage. This article breaks down what makes up a 3D printing quotation from four dimensions: geometry, materials, equipment, and post-processing.
1. First Principles of Cost: Charging by “Grams” and “Hours”
Unlike injection molding or stamping, which rely on mold cost amortization, additive manufacturing has no tooling fee. Its main cost drivers are material consumption and machine occupation time. SLM metal printing is often quoted using a dual-factor model of “built weight + build time”: powder is priced according to the actual melted amount, including necessary supports, while machine costs cover laser operating time, depreciation, inert gas, and energy consumption. Therefore, the heavier the part, the more overhangs it has, and the thinner the layer height, the higher the price and the longer the lead time. Understanding this underlying logic is essential for correctly interpreting every subsequent additional cost.
2. Geometric Features: The Invisible Hand Behind Cost
Geometric features are the most easily underestimated pricing variable. Solid volume directly determines metal powder consumption, while density differences among titanium alloys, aluminum alloys, and stainless steel lead to significant material cost differences for parts of the same volume. Wall thickness affects the number of powder layers and the length of laser scanning paths; thin-walled parts often require slower scanning speeds to ensure density. Overhangs and deep cavities require support structures, and the generation, printing, and subsequent removal of supports are all counted as labor time. By optimizing build orientation and adding self-supporting transitions, support volume can often be reduced by more than 30%. Internal channels and micro-holes create additional post-processing challenges such as powder residue removal and inaccessible supports, which raises the unit price. In simple terms, designing parts to be “lighter, require fewer supports, and be easier to depowder” is the first lever for cost reduction.
3. Material Factors: Grades, Forms, and Recycling Rates
Material cost is jointly determined by grade and form. Among engineering plastics, ABS, PA, and TPU are relatively affordable, while high-temperature specialty plastics such as PEEK and PEI can cost more than ten times as much as standard materials. For metal powders, 316L stainless steel and aluminum alloys are relatively mature and cost-effective, while titanium alloys, nickel-based superalloys, and cobalt-chromium alloys are significantly more expensive due to complex raw materials and powder production processes. In addition, powder recycling rate also affects quotations. The mixing ratio of virgin powder and recycled powder, as well as batch consistency control, is reflected in the cost per gram. Material selection should balance “meeting performance requirements” with “controllable cost,” avoiding unnecessary upgrades to higher grades for redundant specifications.
4. Equipment and Post-Processing: Hidden Costs You Cannot See
Equipment-side costs include machine depreciation, maintenance of laser optical systems, inert gas protection, and process tuning. First-article process validation and parameter calibration for complex parts may also result in one-time engineering fees. Post-processing is often a major component of the quotation: support removal, sandblasting, and polishing are basic processes; if stress-relief heat treatment, CNC finishing, anodizing, or coating is required, additional equipment and labor costs will be added. High-requirement parts that need CMM inspection, industrial CT scanning, or non-destructive testing will also incur testing and certification fees. Communicating these hidden steps in advance helps avoid mismatched expectations where an order starts with a low price but ends with high final costs.
5. From Understanding Quotations to Reducing Costs: Practical Advice for Engineering and Procurement
There are five actionable principles for turning cost logic into practice. First, simplify geometry and reduce supports by replacing overhanging thin walls with fillets and self-supporting angles. Second, consolidate parts by combining multiple assembled components into one print, reducing fasteners and assembly labor. Third, select materials early, prioritizing mature grades while meeting operating conditions. Fourth, plan post-processing in advance by reserving depowdering holes and clamping datums during modeling to reduce finishing difficulty. Fifth, batch parts reasonably by grouping small parts with the same material and process to spread setup and gas costs across one build. Understanding quotation structure is, in essence, negotiating price through design language.
Conclusion
A 3D printing quotation is an itemized account of “complexity and materials”: geometric features determine material consumption and labor time, material grades and recycling rates determine cost per gram, and equipment plus post-processing add hidden expenses. For procurement teams, it provides a basis for price comparison and negotiation; for designers, it serves as a roadmap for cost reduction. lantu3D Printing recommends that companies submit application scenarios and performance requirements at the inquiry stage, allowing the engineering team to provide a more cost-effective manufacturable solution in reverse, shifting quotations from price bargaining to value co-creation.
Submit a model, drawing, image or written notes. Engineers will review material, process, finishing and delivery based on actual use.