
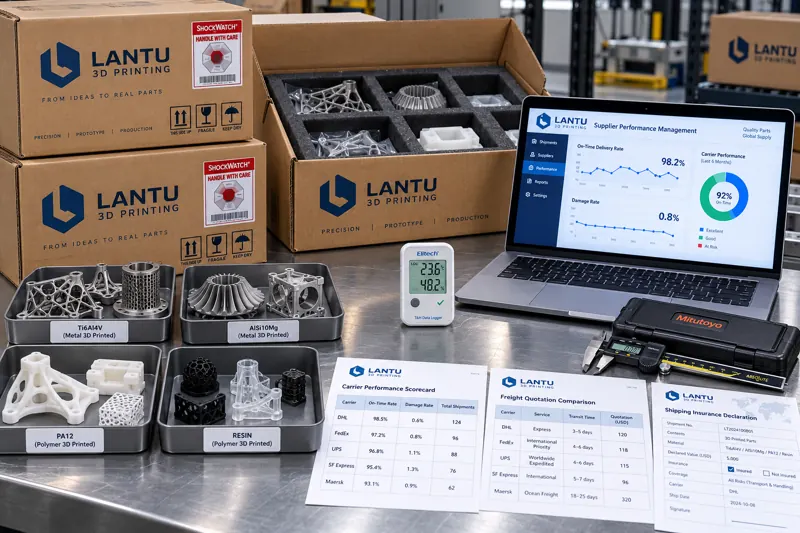
Introduction: Even the Best Packaging Cannot Eliminate Variables in Carrier Handling
Many 3D printing service teams invest heavily in packaging: selecting cushioning inserts based on fragility values, using barrier bags with desiccants, and heat-treating and stamping wooden crates in accordance with ISPM 15. Yet damage still occurs. Post-incident reviews often show that the root cause is not the packaging itself, but the carrier process—excessive loads during sorting and transfer, drops from loading ramps, unrecorded temperature and humidity fluctuations in transit, or a lack of verifiable handover evidence upon delivery. Packaging determines whether a part can withstand an impact; the carrier determines whether it encounters one. When delivery volumes grow from individual prototypes to dozens of shipments per month, simply choosing a familiar logistics provider is no longer sufficient. Carriers must be managed as suppliers subject to qualification, measurement, scoring, and tiered control.
1. Define “Transport Nonconformity” First, or Performance Cannot Be Scored
The first step in carrier management is not selecting a logistics provider, but defining what constitutes a failure. Many disputes arise because the two parties interpret “cargo damage” differently: Does a dented outer carton count? Does a scratch on a part surface count? Does a two-day delay count? Transport outcomes should be divided into four measurable event categories:
1. Functional damage—Part fracture, deformation, or damage to mating surfaces that prevents direct installation or use. This is a zero-tolerance category and carries the highest weighting.
2. Cosmetic damage—Damage to the outer carton, shifted internal cushioning that has not damaged the part, or repairable scratches on the part. These incidents are scored but do not constitute an overall delivery failure.
3. Delivery-time deviation—The difference between the actual proof-of-delivery time and the committed transit time. Record the deviation in hours for each shipment rather than making a simple binary on-time/late assessment, because the distribution of deviations reflects stability better than an on-time rate alone.
4. Missing records—A temperature/humidity data logger was not activated, a shock indicator label was not applied, or the delivery receipt lacks the recipient's signature or timestamp. Although seemingly minor, these are among the most common reasons claims fail and must be tracked separately.
Include these four categories in an appendix to the technical agreement or transportation service terms, and require carriers to acknowledge them before submitting quotations. Only then will subsequent performance scoring have a common basis.
2. Carrier Qualification: Tier by Part Risk Rather Than Using a Single Tender
A practical reality of 3D printing deliveries is the significant variation from part to part: a resin display model and a titanium alloy bracket have entirely different transportation requirements. Assigning all shipments to one carrier either results in overpayment or insufficient protection. A workable approach is to classify deliverables into three risk tiers:
Tier A (high value/high fragility)—Functional metal parts, thin-wall parts prone to deformation, prototypes already validated in installed applications, and orders whose individual part value exceeds an agreed threshold. Requirements: dedicated vehicle or direct route, no sorting or transfer hubs, full transit temperature and humidity logging, mandatory shock and tilt indicator labels, and declared-value insurance covering the full declared value.
Tier B (medium risk)—Nylon parts, standard resin parts, and small multi-part batches. One transfer is permitted, provided cushioning packaging meets requirements and outer-carton stacking limits are clearly defined.
Tier C (low risk)—Documents, sample coupons, and non-functional validation parts. Standard express delivery may be used, with no mandatory monitoring devices.
During qualification review, carriers must demonstrate their capability at the applicable tier, rather than merely claiming to have a nationwide network. The review checklist should include cargo-damage data for comparable goods over the previous 12 months, operating procedures for sorting hubs, availability of shipment-status query interfaces, and actual cycle times for declared-value insurance and claims closure. Carriers unable to provide historical data should initially be trialed with small Tier C shipments and upgraded only after sufficient sample data have been accumulated.
3. Performance Scoring: Base Scores on Records, Not Impressions
Carrier evaluation can easily deteriorate into “this provider seems acceptable.” To avoid this, every input to the scoring model must come from traceable records rather than subjective assessments. A practical quarterly scorecard can be structured as follows:
Damage rate (40% weighting) = Number of functionally damaged parts / Number of parts shipped. Recommended thresholds are ≤0.5% for Tier A orders and ≤2% for Tier B. Exceeding a threshold should trigger corrective action rather than immediate disqualification.
On-time performance rate (25% weighting) = Number of orders with deviations within the allowed window / Total number of orders. Windows should be defined by route, for example, ±12 hours for in-province shipments and ±24 hours for interprovincial shipments. Also record the standard deviation of delivery-time deviations. A high standard deviation indicates unstable transit performance and should flag risk even if the on-time rate is not low.
Record completeness rate (20% weighting) = Number of shipments with complete records / Total number of shipments. A complete record requires a delivery receipt with signature and timestamp, exportable monitoring-device data, and in-transit notifications for abnormal events.
Exception response and claims cooperation (15% weighting)—Measured by the number of working days from raising an exception to receiving the carrier's written response, as well as the claims closure cycle time.
The weighted score across these four categories becomes the quarterly performance result. Scores should not be used only for rewards and penalties; they should also drive tiered allocation adjustments: carriers meeting Tier A requirements for two consecutive quarters should receive a larger share of Tier A shipments, while those remaining below threshold for two consecutive quarters should have their allocation reduced or be downgraded. Only when scores affect business allocation do carriers have a real incentive to improve.
4. Freight and Terms: Include Hidden Costs in the Unit Price
A procurement approach that considers only the quoted price per kilogram will almost inevitably create problems in 3D printing deliveries. Actual transport costs include at least five elements: base freight, fuel and remote-area surcharges, declared-value insurance premiums, amortization of packaging fixtures and monitoring devices, and the cost of reproduction and claims administration after cargo damage occurs. The last category is most often overlooked. The direct loss from damage to a Tier A part may only be material and machine time, but the consequential losses can include customer production downtime, capacity consumed by rescheduling, and delayed project milestones.
When comparing quotations, normalize all carrier prices into a per-part landed cost: allocate the actual quarterly cost of the five items above across the number of parts shipped, then compare the result with quoted prices. In practice, the carrier with the lowest quoted rate often has the highest landed cost after its damage rate and lengthy claims cycle are factored in.
Three items must be explicitly fixed in contractual terms: declared-value insurance and claims limits (the compensation percentage of declared value and deductibles), the starting point for the claim period (preferably the proof-of-delivery timestamp rather than the invoice date), and allocation of the burden of proof (who provides unboxing photos, who provides in-transit monitoring data, and the consequences of failing to raise an objection within the agreed period). If these points are vague, a damage event will lead only to dispute.
5. Integration with Packaging Design: It Is Management Only When the Loop Is Closed
Carrier management is not an isolated function. When cargo-damage rates rise on a particular route, the first response should not simply be to replace the carrier. Review whether the packaging design matches actual route conditions: Does an increase in transfers mean stacking layers were underestimated? Does a longer transit time mean the desiccant quantity is insufficient? Do seasonal temperature and humidity changes exceed the design limits of the barrier bag? Conversely, the effectiveness of packaging improvements also requires carrier records for validation—only in-transit shock, temperature, and humidity data can determine whether changes to cushioning inserts actually work.
Therefore, establish a simple closed loop: each quarter, classify cargo-damage incidents by the three dimensions of “route + part risk tier + packaging design,” identify high-frequency combinations, make targeted adjustments to packaging specifications or carrier allocation for the route, and review the results in the following quarter. After two or three cycles, cargo-damage rates will typically show a clear structural decline.
Conclusion
The core of carrier management is to transform transportation from an activity that is simply outsourced into an engineered process with qualification standards, a scoring model, contractual controls, and closed-loop reviews. Four practical starting points are: clearly define the four categories of transport nonconformities and establish carrier requirements by tier; develop quarterly scores from traceable records rather than subjective impressions; convert all costs into per-part landed cost before comparing quotations; and include declared-value insurance, claim deadlines, and burden of proof in contractual terms. For 3D printing businesses characterized by high-value, low-volume deliveries and demanding schedules, the benefit of this approach is not merely saving a few percentage points in freight negotiations. It is converting uncontrollable in-transit variables into measurable, improvable, and accountable certainty.
Invia un modello, un disegno, un'immagine o note scritte. Gli ingegneri valuteranno materiale, processo, finitura e consegna in base all'uso effettivo.