
Introduction: Completing Training Does Not Equal Competency
Many 3D printing companies stop their workforce training process at “the courses have been delivered, attendance sheets have been collected, and exams have been passed.” Yet when production lines still frequently experience issues such as failing to verify powder-bed consistency after replacing a recoater blade, replacing protective lenses beyond their service interval, or loading unregistered powder batches into machines, what is truly missing is often not training hours but a quantitative assessment of training effectiveness. Training is an investment and must have measurable output criteria; otherwise, budget approval can only rely on experience and negotiation.
1. Separate the Evaluation Levels: An Engineering Adaptation of Kirkpatrick’s Four Levels
Kirkpatrick’s four-level model—reaction, learning, behavior, and results—often becomes a formality in workshops because every level is reduced to subjective scoring. An engineering-oriented approach assigns an objective data anchor to each level: at the reaction level, do not rely solely on satisfaction surveys, but count valid questions and case-discussion contributions after training; at the learning level, do not merely record whether trainees passed, but track first-pass rates in practical assessments and the number of omitted critical steps; at the behavior level, use on-site observation checklists to sample compliance with standard actions such as powder changes, powder cleaning, and first-article verification; at the results level, directly link training to quality and cost metrics, including rework batches caused by operational errors, unplanned downtime, and scrap cost.
2. First Define the Metric That Needs to Be Reduced
Without a baseline, there can be no evaluation. Before training begins, define two or three attributable metrics, such as reducing changeover time from 45 minutes to 30 minutes, lowering unplanned equipment downtime from 9 hours to 5 hours per month, or increasing first-article approval on the first attempt from 72% to 90%. These metrics must have a clear causal relationship with the training content: powder-spreading process training should correspond to powder-bed defect rates, while equipment inspection training should correspond to unplanned downtime. If the wrong metrics are selected, all subsequent evaluation data will be distorted.
3. Assess Actions, Not Memory
Written tests can only verify knowledge retention; they cannot validate operational consistency. Practical assessments should use scorecards designed for each workstation. For example, a powder-change procedure for LPBF equipment should include five to seven critical actions, such as used-powder sieve mesh size, documentation of reclaimed-powder blend ratios, oxygen-level verification, visual inspection of the recoater blade edge, and confirmation of the first powder-spread layer. Each action should be scored across three levels: “completed independently,” “completed after prompting,” and “unable to complete.” The consolidated result provides a job-skill attainment score, which is more predictive of on-site performance than an exam score.
4. Use Sampled Observation for the Behavior Level, Not Self-Discipline
The two to six weeks after training is the critical window for behavioral reinforcement. Schedule at least two on-site observations per month, with each session covering three to five operating cycles and being conducted by a team leader or process engineer using a standardized observation checklist. Observation results should be fed back into each employee’s skills matrix, creating a “training-observation-retraining” closed loop. Data show that teams receiving training without behavioral observation typically see standard-action compliance fall back to around 60% of pre-training levels after three months.
5. Convert Training Investment into Comparable Costs
Training costs consist of four components: instructor hours, trainee time away from production, equipment and material usage, and assessment and documentation. For a two-day equipment-operation training session for eight employees, assuming a fully loaded daily cost of RMB 400 per person and equipment opportunity cost of RMB 180 per hour, the direct investment is approximately RMB 12,000 to RMB 16,000. On the output side, calculate attributable reductions in rework costs, downtime losses, and scrap costs during the three months after training. When the output-to-input ratio consistently exceeds 2, the course is worth retaining and standardizing; when it falls below 1.2, its content should be redesigned or converted to on-the-job coaching.
6. Certification Authorization and Refresher Cycles
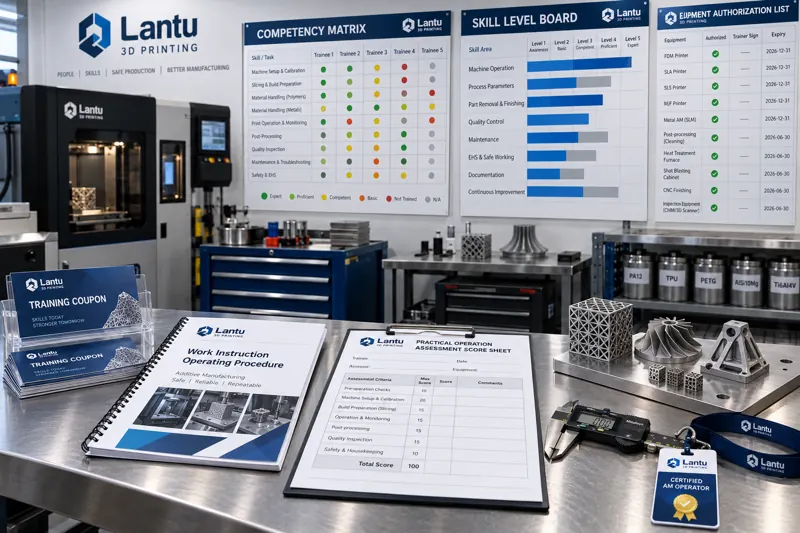
Evaluation conclusions must be translated into authorization decisions. Personnel who meet both theoretical and practical requirements should receive authorization for specific workstations, with an expiration period—typically 6 to 12 months—recorded in the skills matrix. Authorization may be extended only after refresher training or a behavioral-observation review is completed before expiration. Authorization should be automatically suspended following a quality incident, an equipment-operation violation, or three consecutive months without working at that station. The authorization list should be linked to the production scheduling system so that only personnel with valid authorization can be assigned to relevant tasks. This step truly embeds training outcomes into the production process.
7. Common Biases and Corrections
Three biases occur most frequently. First, satisfaction is used as a substitute for effectiveness: trainees provide high ratings while on-site metrics remain unchanged. Second, company-wide training is treated as a universal solution, overlooking the possibility that the problem may lie in tooling or work instructions. Third, evaluation is conducted only once, without trend comparisons. The corresponding corrections are to keep satisfaction weighting below 20%, determine root causes before deciding on the training format, and issue evaluation reports using consistent criteria every quarter to establish a time series.
Conclusion
The core of engineering-based training effectiveness evaluation is converting “attended a course” into “can work independently, performs consistently, and delivers measurable cost savings.” Use Kirkpatrick’s four levels to establish the framework, baseline metrics to anchor direction, practical scorecards and behavioral observations to validate performance, and ROI to determine whether courses should be retained. Finally, use certification authorization to embed results in each role. lantu3D emphasizes full life-cycle management from drawing to physical delivery; workforce capability requires the same closed loop: it must be definable, measurable, authorizable, and traceable.
Submit a model, drawing, image or written notes. Engineers will review material, process, finishing and delivery based on actual use.